Precision Fabrication & Engineering Products
Explore our high-frequency, prototype, and high-density interconnect (HDI) rigid and flex manufacturing capabilities verified across global aerospace, telecom, and industrial accounts.



The Global Shift to 3D Interconnect: Rigid-Flex Circuit Architectures
How Tier-1 aerospace, medical robotics, and automotive OEMs eliminate wire harnesses, reduce volumetric packaging by 60%, and eradicate intermittent dynamic failures.
Structural Harmonization
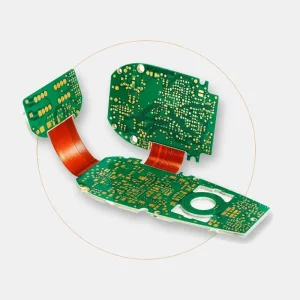
Rigid-flex printed circuit boards integrate alternating zones of flexible polyimide (PI) dielectric films and rigid FR-4 or high-Tg hydrocarbon laminates. By consolidating multiple rigid PCBs and flex cabling into an uninterrupted monolithic substrate, engineers eliminate failure-prone crimped pins, board-to-board connectors, and manual assembly hand soldering, providing superior resistance to shock, acceleration, and thermal cycling.
High-Frequency Signal Integrity
Traditional wire jumpers introduce unpredictable parasitic capacitance and inductive spikes that degrade high-frequency transmission. Our controlled-dielectric adhesiveless copper clad laminates (FCCL) maintain consistent characteristic impedance (50Ω single-ended, 90Ω/100Ω differential) across transitions, supporting multi-gigabit data protocols like PCIe Gen 4/5, USB4, and MIPI CSI-2 without phase reflection.
Harsh Environment Endurance
Certified under IPC-6013 Class 3, our rigid-flex circuits undergo automated thermal stress tests, surviving 288°C solder float conditions for over 10 seconds without delamination or barrel cracking. With operating temperature envelopes from -55°C to +150°C, these assemblies endure demanding automotive under-the-hood, defense guidance, and deep-well exploration environments.
Engineering Strategic Takeaway for Hardware Directors
While the initial unpopulated bare-board unit price of a rigid-flex PCB is higher than an equivalent pair of standard FR-4 boards with ribbon cables, the Total Cost of Ownership (TCO) is 18% to 32% lower when factoring in harness tooling, assembly labor, inspection steps, enclosure volume miniaturization, and warranty failure rates.
Rigid-Flex Design Rules, Stack-Up Geometries & Materials
In-depth technical baseline specifications for hardware development engineers targeting reliable static bending and dynamic flex endurance.
Substrate & Dielectric Selection
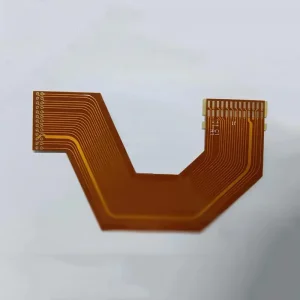
We strictly deploy premium grade adhesiveless flexible copper clad laminates (FCCL) using DuPont Kapton® or Kaneka polyimide films (12.5μm, 25μm, 50μm). Adhesiveless materials eliminate the z-axis expansion mismatch typical of acrylic and epoxy bonding agents, preventing micro-via shearing during thermal cycling and lead-free reflow.
Neutral Axis & Bending Dynamics
To avoid trace cracking in dynamic installations, copper conductors must reside strictly along the mechanical neutral axis. For dynamic flex sections, we mandate Rolled Annealed (RA) copper over standard Electro-Deposited (ED) foil, maintaining a minimum bend radius of $R \ge 10 \times T$ for single-layer dynamic lines and $R \ge 20 \times T$ for multi-layer flex zones.
Transition Zone & Strain Relief
The rigid-to-flex boundary represents a localized stress riser. Our DFM protocol introduces a minimum 0.5mm stagger between rigid prepreg cutouts and flex coverlay edges, complemented by bead-dispensed structural epoxy strain-relief fillets (flexible potting) to absorb shear forces generated during assembly folding.
| Manufacturing Parameter | Standard Commercial Capability | Advanced / Aerospace Capability | Verification / Standard |
|---|---|---|---|
| Layer Count Range | 2 to 12 Layers (Rigid + Flex Combined) | Up to 22 Layers (HDI Rigid-Flex 3+N+3) | IPC-6013 Type 4 |
| Flex Core Material | Polyimide (PI) Adhesiveless 0.5mil / 1mil / 2mil | Modified PI (MPI) / Liquid Crystal Polymer (LCP) | IPC-4204A |
| Copper Foil Types | Electro-Deposited (ED) 0.5oz / 1oz / 2oz | High-Ductility Rolled Annealed (RA) 1/3oz to 2oz | IPC-4562 |
| Min. Trace Width / Space (Inner Flex) | 3.0 mil / 3.0 mil (75μm / 75μm) | 1.8 mil / 1.8 mil (45μm / 45μm mSAP) | Optical Laser Direct Imaging (LDI) |
| Laser Micro-Via Diameter | 4.0 mil (0.10 mm) | 2.5 mil (0.065 mm) Picosecond UV | Micro-section & 3D X-Ray |
| Controlled Impedance Tolerance | ±10% Nominal | ±5% High-Precision Dynamic Stacks | Polar CITS8800 TDR Testing |
| Surface Finishing Systems | ENIG (Electroless Nickel Immersion Gold) | ENEPIG, Hard Gold Finger, Immersion Silver | IPC-4552 / IPC-4556 |
China Rigid Flex Circuit Pricelist & Cost Estimation Framework
Transparent benchmark engineering costs and batch volume scaling pricing. Direct factory quotes eliminate Western distributor markups while preserving full traceability.
| Stack-Up Configuration | Key Substrate Composition | Prototype Lot (5-10 Pcs) | Medium Volume (100-500 Pcs) | Production Volume (>1,000 Pcs) | Standard Lead Time |
|---|---|---|---|---|---|
| 2-Layer Pure Flex (FPC) | 1 mil Adhesiveless PI + 0.5oz RA Cu + Coverlay | $140 - $220 total | $1.80 - $3.50 / pc | $0.75 - $1.60 / pc | 3 - 5 Working Days |
| 4-Layer Rigid-Flex (1R + 2F + 1R) | FR-4 Outer + 2L Polyimide Core + No-Flow PP | $380 - $550 total | $6.80 - $12.50 / pc | $3.20 - $6.50 / pc | 6 - 8 Working Days |
| 6-Layer Rigid-Flex (2R + 2F + 2R) | High-Tg FR4 + Central 2L Dynamic RA PI Core | $560 - $780 total | $11.50 - $19.00 / pc | $5.80 - $10.20 / pc | 8 - 10 Working Days |
| 8-Layer Multi-Flex (2R + 4F + 2R) | Dual Flex Arms + Symmetrical Balanced FR4 | $850 - $1,250 total | $22.00 - $38.00 / pc | $12.50 - $21.00 / pc | 10 - 14 Working Days |
| 10-14 Layer HDI Rigid-Flex | Stacked Micro-Vias + Laser Blind/Buried Stacks | $1,400 - $2,100 total | $45.00 - $75.00 / pc | $26.00 - $42.00 / pc | 14 - 18 Working Days |
Tooling & Laser NRE
Tooling fees cover high-precision steel die-punching fixtures, flying probe / bed-of-nails E-test frames, and UV laser ablation profiles for pocket opening. Prototype NRE ranges from $180 to $450 depending on layer complexity.
Panel Utilization Rates
Because flex extensions can produce awkward board outlines, irregular geometries cause low panel nesting efficiency. Our engineers perform panelization interlocking during DFM to boost material yield above 82%, cutting unit costs.
No-Flow Prepreg Bonding
Rigid-flex pressing mandates specialized low-flow or no-flow prepregs (e.g., Ventec or Shengyi) to stop resin squeeze onto the flexible dynamic arms. Controlled rheology materials represent a modest cost premium that guarantees zero flex boundary blistering.
Turnkey SMT & Carrier Tooling
Flexible boards flex under SMT placement and reflow heat. We manufacture custom high-precision synthetic stone or magnetic assembly pallets to keep planar flatness within 0.05mm, ensuring 01005 passives and 0.35mm pitch BGAs mount with 99.8% yield.
Macro-Industrial Solutions & Strategic Deployments
Field-proven electronic architectures engineered to operate reliably under extreme mechanical shock, high thermal gradients, and severe spatial constraints.
Anti-Drone & Defense Jamming
Multi-spectral radar and anti-UAV systems demand high-power RF transmission and compact structural integration. We manufacture hybrid stackups combining Rogers 4350B hydrocarbon ceramics with multi-layer polyimide flex arms. These boards handle pulsed high RF wattage while folding neatly inside conformal drone-hunting antennas without connector insertion losses.
Class III Medical Robotics & Imaging
Endoscopic cameras, surgical robots, and ultra-miniaturized implantable diagnostic monitors depend on biocompatible flex substrates. With 25μm micro-trace geometries, adhesiveless polyimides, and ENEPIG gold wire-bondable surfaces, our assemblies withstand dozens of autoclave sterilization cycles without layer separation.
EV Powertrain & Battery Management
Next-generation Electric Vehicle Battery Management Systems (BMS) are replacing heavy copper wire harnesses with integrated rigid-flex sensing lines. Our multi-cell sensor boards span lengths up to 1,200mm, integrating NTC thermistors, voltage taps, and nickel-tab ultrasonic welding zones directly onto the battery module housing.
Aerospace & Satellite Avionic Avionics
Satellite payloads and flight control systems operate under severe payload weight penalties and cosmic radiation. By utilizing copper-invar-copper (CIC) thermal planes with polyimide rigid-flex links, we achieve balanced coefficient of thermal expansion (CTE) matching ceramic FPGA packages while cutting payload launch weight by kilograms.
Optoelectronic & Foldable Consumer Tech
From high-refresh-rate AR/VR headsets to foldable mobile displays, hinge-spanning interconnects endure tight dynamic flexing. Our high-ductility rolled-annealed foils and dual-sided symmetric coverlays survive over 200,000 bending cycles across a 1.5mm dynamic bend radius without impedance drift.
Industrial Automation & CNC Robotics
Articulated robotic arm joints subjected to continuous torsion and multi-axis flexing rely on custom helical rigid-flex cables. With silver-paste EMI shield printing and carbon cross-hatch ground planes, these assemblies block electrical motor drive noise from corrupting delicate sensor feedback lines.
Rigid-Flex Technology Roadmap (2026–2030)
Continuous process scaling to address fine-pitch sub-30μm lithography, embedded passive integration, and ultra-high-speed optoelectronic flex interconnects.
mSAP Fine-Pitch Generation
- Semi-Additive Process (mSAP) on flex cores down to 25μm line / 25μm space.
- Embedded laser-drilled copper micro-vias with 50μm landing pads.
- Low-loss Modified PI (MPI) laminates handling sub-6GHz and Wi-Fi 7 telemetry.
Liquid Crystal Polymer (LCP) Scale
- Full volume scale of multi-layer pure LCP circuits for mmWave 77GHz radar.
- Moisture absorption lowered to <0.04% for precision space applications.
- Direct die-attach wire bonding onto flexible core inner layers.
Embedded Active Silicon
- Bare silicon dies and passive components fully embedded inside the flex cavity.
- Zero-profile Z-axis interconnections cutting package thickness under 0.35mm.
- Graphene and carbon nanotube conductive films for million-cycle dynamic folding.
Electro-Optical Flexible Substrates
- Polymer optical waveguides integrated directly alongside flex copper traces.
- Terabit-per-second board-to-board optical links with zero EMI vulnerability.
- Bio-compatible dissolvable substrates for transient medical monitoring implants.
Metrology, Quality Assurance & Global Supply Chain Resilience
Stringent factory acceptance criteria backed by digital MES traceability, ensuring every panel delivered to North America, Europe, and Asia-Pacific operates fault-free.
IPC-6013 Class 3 Micro-Sectioning
Every production panel features dedicated inspection test coupons along the perimeter. We conduct cross-sectional metallurgical micro-etching to verify through-hole copper plating thickness (minimum 25μm in-hole wall), barrel-to-flex foil wrap integrity, and zero dielectric separation after 3-cycle thermal shock stress tests.
Automated Optical (AOI) & Flying Probe
Both inner flex layers and finished composite boards pass through 100% automated optical inspection (AOI) to intercept pinholes, nicks, and etching shorts. High-speed dual-sided flying probe electrical test frames verify 100% netlist continuity and isolation resistance up to 500VDC.
Localized Logistics & DDP Delivery
Headquartered in Bao'an District, Shenzhen — minutes from Hong Kong International Airport logistics gateways — we provide complete Delivered Duty Paid (DDP) shipping via DHL, FedEx, and air freight forwarders. Our engineering and sales team provides 24/7 technical support in fluent English with 2-hour DFM quote turnaround.
Frequently Asked Questions on Rigid-Flex Circuit Design & Sourcing
Definitive engineering and commercial answers to help procurement managers and PCB layout engineers validate design specifications before committing to tooling.
What is the minimum bend radius formula for multi-layer rigid-flex boards?
For static installations (bend-to-fit once during assembly), the safe design rule is a minimum bend radius $R \ge 10 \times T$, where $T$ is the total thickness of the flexible section. For dynamic applications (continuous flexing like hinges or robotic heads), the bend radius must satisfy $R \ge 20 \times T$ with single-layer or balanced dual-layer RA copper cores positioned strictly on the neutral axis.
Why should adhesiveless copper clad laminates (FCCL) be specified instead of adhesive-based?
Adhesiveless FCCL directly casts or bonds polyimide directly onto copper foil without an acrylic or epoxy bonding film. Acrylic adhesives have high z-axis thermal expansion coefficients ($>200\text{ ppm/°C}$), which can cause plated through-hole (PTH) barrel fracture during lead-free soldering. Adhesiveless laminates deliver better thermal stability, thinner profiles, and superior micro-via reliability.
How do you mitigate adhesive squeeze-out during the rigid-flex lamination cycle?
We deploy specialized no-flow or low-flow prepregs (such as Shengyi or Ventec) combined with CNC-cut release films and conformal rubber cushions. Standard prepreg flows excessively under vacuum pressure, oozing out over the flexible arm and compromising bendability. No-flow prepreg has a tight viscosity window that locks the boundary line within ±0.2mm.
What files are strictly required to quote and fabricate a custom rigid-flex PCB?
Please supply: 1. Gerber RS-274X or ODB++ dataset; 2. An unambiguous stack-up diagram defining which layers are rigid FR-4 and which layers extend into the flex zone; 3. A mechanical drawing indicating rigid-to-flex transition borders, coverlay openings, and stiffener materials; 4. An IPC-356 netlist for automated bare-board electrical testing.
Can you assemble surface mount components (SMT) directly onto the flexible region?
Yes. When components must sit on flexible arms, we apply rigid backing stiffeners (FR-4, polyimide, stainless steel, or aluminum) laminated directly beneath the component footprint with thermosetting adhesive. Stiffeners prevent the circuit from bending under the solder joints, protecting SMT ceramic capacitors and IC packages from micro-fracturing.
What is the standard production turnaround time for prototypes vs. volume orders?
Standard quick-turn prototype rigid-flex boards (4 to 6 layers) are built and tested in 6 to 9 working days. Expedited 72-hour fast-turn options are available upon DFM confirmation. Production volumes (500 to 10,000+ pieces) require 2 to 3 weeks, including laser routing, flying probe/fixture testing, and vacuum desiccant packaging.
High-Reliability Rigid, Flex & Multilayer Catalog
Explore our broader factory portfolio including high-power heavy copper boards, metal core thermal substrates, and high-frequency materials manufactured under ISO 9001 and UL protocols.