
High-Reliability Rigid-Flex & Advanced PCB Assemblies
Engineered for mission-critical signal integrity, dynamic flexing endurance, and high thermal dissipation in compact enclosures.
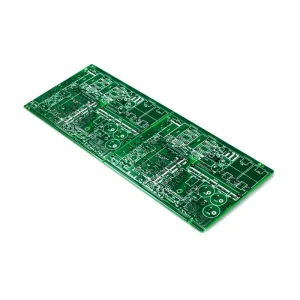
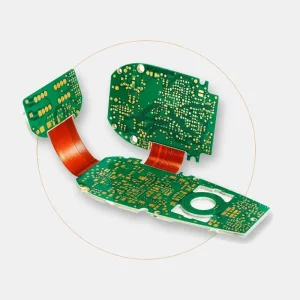


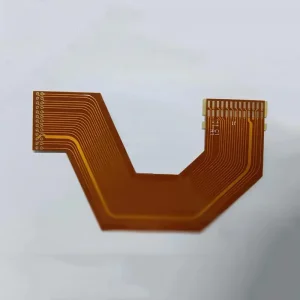
Altium Designer Rigid-Flex Stack-Up Architecture & 3D ECAD-MCAD Co-Design
Eliminating spatial interference, trace fracturing, and impedance mismatches at the schematic and layout phases through automated physical validation.
Native Layer Stack Manager (LSM)
Altium Designer’s advanced Layer Stack Manager enables dynamic multi-stack configuration within a singular PCB database. Our engineering direct-intake pipeline translates your Altium stack-up files directly into laser-drilling and pre-preg press recipes.
- Precise sub-stack definitions for rigid zones (FR-4 / High-Tg) and flexible regions (adhesiveless polyimide).
- Configurable dielectric constant (Dk) and loss tangent (Df) parameters for impedance modeling up to 28 Gbps.
- Embedded coverlay, adhesiveless FCCL, and localized stiffener definition (FR-4, Stainless Steel, Aluminum).
3D Clearance & Dynamic Folding Simulation
Avoid expensive re-spins caused by enclosure collisions. Using Altium's realistic 3D folding engine and bend-line definition tools, our engineers verify mechanical enclosures against copper trace stress points before panel fabrication.
- Dynamic bend radius (R) validation adhering strictly to IPC-2223 guidelines ($R \ge 10\times$ thickness for dynamic flex).
- Collision detection with adjacent SMT components, connector latches, and mechanical housing chassis.
- STEP model exchange between Altium, SolidWorks, Autodesk Fusion, and Siemens NX for seamless tolerance fit.
Automated DFM DRC Constraints
We supply native Altium Design Rule Check (`.rul`) files customized for complex rigid-flex builds. Load our rules directly into Altium to instantly trap manufacturing violations before tape-out.
- Automated detection of conductor routing perpendicular to bend axes to mitigate grain-direction fracture.
- Enforced clearance margins from rigid-to-flex transition interfaces (minimum 1.25mm keep-out zone).
- Staggered microvia rules and hatched ground polygon configurations for sustained flexible shield integrity.
Comprehensive Engineering Capabilities & Design Rules
Adhering to IPC-6013 Type 4 rigid-flex requirements for high-vibration, mission-critical, and extended thermal cycling environments.
| Process Parameter | Standard Capability | Advanced / ODM Tolerance | Design Consideration (Altium Setup) |
|---|---|---|---|
| Layer Count (Rigid + Flex) | 2 to 16 Layers | Up to 24 Layers (HDI Rigid-Flex) | Configured in LSM with multi-stack region mapping |
| Base Flex Substrate | Polyimide (PI) 12.5µm / 25µm | Adhesiveless FCCL (DuPont Pyralux AP/LF) | Essential for dynamic high-frequency flexing |
| Rigid Core Laminate | FR-4 (Tg 150°C to 180°C) | Rogers 4350B, Megtron 6, Shengyi S1000-2M | Hybrid dielectric pairing for low-loss RF transitions |
| Min. Line Width / Spacing (Outer) | 3.0 mil / 3.0 mil (75µm / 75µm) | 2.0 mil / 2.0 mil (50µm / 50µm) | Compensated during CAM etching photolithography |
| Min. Laser Microvia Aspect Ratio | 0.8:1 | 1:1 (Stacked / Staggered via-in-pad) | Enables ultra-dense 0.35mm pitch BGA breakout |
| Rigid-to-Flex Transition Overlap | 1.0 mm (0.040 in) | 0.5 mm (Controlled bead profile) | Requires structural strain-relief acrylic epoxy fillet |
| Dynamic Flex Bend Ratio | $10\times$ total flex thickness | $6\times$ (Static single-installation fold) | Neutral bend axis copper layer positioning |
| Surface Finishing | Electroless Nickel Immersion Gold (ENIG) | ENEPIG, Immersion Silver, Hard Gold | Protects against micro-crack formation during bending |
Controlled Impedance Co-Simulation
Impedance discontinuities in rigid-flex occur predominantly at the boundary interface where the dielectric medium shifts from FR-4 to polyimide. Our CAM engineering team applies automated field-solver simulations to balance line widths at the necking region, guaranteeing 90Ω differential and 50Ω single-ended tolerances within ±5%.
Cross-Hatched Flex Ground Planes
Solid copper planes compromise the mechanical ductility of the flexible arm and create mechanical memory that promotes delamination. We automatically optimize Altium solid polygon planes into 45-degree cross-hatched geometries, preserving maximum electromagnetic shielding while delivering superior flexibility and thermal relief.
Air-Gap Multi-Layer Flex Technology
When rigid-flex designs exceed three flexible layers, cumulative material stiffness can severely hinder tight chassis installation. We employ selective air-gap manufacturing where flex arms are physically unbonded in dynamic sections, dramatically lowering bend resistance and extending cyclic flex life beyond 1,000,000 continuous bend cycles.
High-Yield Turnkey Fabrication in China's Electronics Capital
Combining vertically integrated component procurement, high-speed SMT lines, and automated IPC testing under one roof in Bao'an, Shenzhen.
Tier-1 BOM Component Sourcing
Positioned at the epicenter of Shenzhen's semiconductor trading network, we maintain strategic partnerships with direct franchised distributors for Texas Instruments, Analog Devices, STMicroelectronics, Microchip, Murata, and TE Connectivity. We mitigate lead-time crunches by recommending pin-compatible drop-in alternatives accompanied by full lifecycle reports.
Laser Microvia Drilling & Plasma Cleaning
Rigid-flex multi-layer stacks require clean transitions through differential substrates. We utilize Mitsubishi UV/CO2 laser drilling systems paired with industrial vacuum plasma desmear stations to eliminate resin-smear in flexible via barrels, ensuring zero barrel separation or micro-crack development during high-temperature reflow cycles.
Specialized Rigid-Flex Assembly Pallets
Standard SMT surface mount machines encounter feed errors when placing components on unsupported flexible regions. Our tooling department designs custom high-precision magnetic SMT fixture pallets and vacuum carriers for every rigid-flex design, ensuring flat board presentation through solder paste printing, high-speed chip shooting, and multi-zone convection reflow.
Global Enterprise Procurement, Local Support & Regulatory Compliance
Addressing Western OEM procurement criteria: tariff optimization, stringent quality certifications, and direct engineering accountability.
International Compliance
Our manufacturing facilities operate in strict compliance with ISO 9001:2015, ISO 13485 (Medical Devices), and IATF 16949 (Automotive). All delivered bare boards and assembled PCBA units meet RoHS 3, REACH, and UL 94V-0 flammability ratings.
ITAR & IP Protection
We enforce strict intellectual property isolation protocols. Sensitive Altium design files, schematic libraries, and firmware binaries are stored in isolated encrypted on-premises vaults with role-based engineering clearance and strict non-disclosure compliance.
End-to-End MES Traceability
Every rigid-flex panel is laser-marked with a unique DataMatrix 2D barcode. Our Manufacturing Execution System tracks raw material batch numbers, lamination press temperatures, solder paste lot numbers, reflow profiles, and automated optical inspection logs down to individual serial numbers.
Bilingual DFM Support
Overseas clients collaborate directly with dedicated English-fluent CAM engineering managers. Within 12 hours of Altium file receipt, we return comprehensive DFM/DFA engineering queries (EQ) covering stack-up adjustments, drill tolerances, and component pad geometries.
Emerging Technologies Shaping Modern Rigid-Flex Architecture
Addressing the demands of micro-miniaturization, 5G/6G RF frequencies, and extreme power densities in mission-critical electronics.
Any-Layer HDI Rigid-Flex (ELIC)
As wearables and medical endoscopic devices shrink, traditional through-hole vias give way to Every Layer Interconnect (ELIC). Our plant delivers multiple laser-drilled microvia cycles stacked through both rigid and flexible sections, permitting complex BGA escapes under 0.3mm ball pitch with zero stub-induced signal reflection.
Embedded Passives & Thin Stiffeners
To reclaim board real estate in dense packaging, we embed discrete thin-film resistors and planar decoupling capacitors directly inside inner flex layers. Coupled with CNC-machined stainless steel stiffeners featuring thermally conductive pressure-sensitive adhesives (PSA), heat is efficiently drawn away from localized hot spots.
Low-Loss High-Speed SerDes Channels
Next-gen edge computing, LiDAR scanners, and camera vision links require PCIe Gen 5 and USB4 speeds through flexible umbilical interconnects. We laminate modified polyimide (MPI) and liquid crystal polymer (LCP) cores directly with low-loss high-Tg rigid cores to maintain clean eye diagrams past 32 Gbps.
Mission-Critical Applications Powered by Our Rigid-Flex Technology
Proven across extreme aerospace environments, high-precision biomedical devices, and harsh industrial power applications.
Aerospace & Defense Jamming
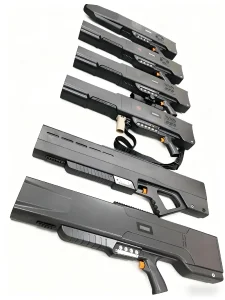
Used extensively in counter-UAS directional jamming arrays and airborne radar units. Rigid sections support high-wattage GaN RF power amplifiers while the integrated flex sections bend around circular chassis hulls, eliminating heavy wire harnesses and coaxial RF connectors.
Biocompatible Medical Devices
From swallowable pill-cams to multichannel continuous glucose monitoring (CGM) sensors. Fabricated with pure polyimide substrates, ENIG/ENEPIG biocompatible finishes, and micro-pitch SMT placement down to 01005 passives for wearable, flexible patient comfort.
Automotive EV & ADAS Radars
Installed inside 77 GHz radar transceivers, battery management systems (BMS), and electric steering actuators. Engineered to withstand continuous thermal shocks from -40°C to +150°C and severe harmonic vibration profiles without wire-bond fatigue.
Robotics & Dynamic Articulation
Serving high-speed optical inspection pick-and-place heads and multi-axis collaborative robotic arms. Designed for millions of dynamic flexural cycles using rolled-annealed (RA) copper foil to prevent crystallization and trace rupture during continuous motion.
Rigid-Flex PCB & Altium Design: Frequently Asked Questions
In-depth engineering answers to common challenges faced during schematic capture, stack-up planning, and overseas production handover.
How do I properly export Altium Designer files for rigid-flex manufacturing?
When preparing rigid-flex projects in Altium Designer, the preferred export formats are ODB++ or IPC-2581. These modern formats preserve complex layer-stack assignments, rigid-to-flex boundary definitions, bend lines, and stiffener geometries within a single consolidated database. If exporting traditional Gerber RS-274X, you must provide separate Gerber layers for coverlays, stiffener profiles, flex cutouts, and bonding adhesive windows, accompanied by an explicit Stack-Up Table drawing and DFM notes document.
What is the difference between ED and RA copper in rigid-flex fabrication?
Electro-Deposited (ED) copper is formed via chemical electroplating and possesses a vertical columnar grain structure. While rigid boards use ED copper, it is prone to cracking when subjected to dynamic folding. Rolled-Annealed (RA) copper undergoes intense mechanical rolling that creates elongated, horizontal crystalline grain structures. RA copper is mandatory for any flexible PCB section subject to repetitive flexing, offering orders-of-magnitude greater cyclic fatigue endurance over ED copper.
Why should I avoid placing plated through-holes (vias) near the transition line?
The interface between the rigid laminate (FR-4) and the flexible arm (polyimide) represents an abrupt mechanical stress gradient. Under IPC-2223 rules, plated through-holes or laser microvias placed within 1.25mm (50 mils) of this transition boundary experience concentrated mechanical shear stresses during panel handling, reflow expansion, or bending. This shear leads to copper barrel rupture or inner-layer foil cracking. Always respect our design keep-out rule of at least 1.25mm from the rigid interface.
Can you assemble SMT components directly onto the flexible region?
Yes. Components can be placed on flexible regions provided appropriate structural support is implemented. For passive components (0402, 0603) or small ICs, we laminate localized FR-4, polyimide, or stainless-steel stiffeners on the reverse side of the board directly beneath the component footprint. This creates a rigid platform that prevents solder joint micro-cracking caused by board flexing while allowing the surrounding arm to bend freely.
How does your Shenzhen factory test unpopulated rigid-flex circuit boards?
100% of bare rigid-flex boards undergo non-destructive electrical verification. We employ high-precision flying probe testing alongside dedicated four-wire Kelvin resistance measurement setups to identify microscopic hairline opens, microvia delaminations, or leakage down to 0.05Ω. For high-volume production orders, custom bed-of-nails test fixtures with contour-milled nest supports ensure high-speed continuity validation without marring flexible polyimide coverlays.
What are the minimum prototype lead times and volume ramp capabilities?
Standard rigid-flex prototypes (4 to 8 layers) can be completed in 5 to 7 working days, with an expedited 48-hour turn available for critical engineering verification. Following First Article Inspection (FAI) and functional testing sign-off, our 6 automated SMT lines and high-capacity lamination presses can seamlessly ramp to batches of 50,000+ units per month with consistent Cpk yield indices.
High-Layer Count, Specialized Substrates & RF Circuit Solutions
Explore our extended line of multi-layer, thermal-core, and high-frequency printed circuit boards manufactured in Shenzhen, China.



