
Precision Prototype Solutions: Active Production Series (Part I)
Engineered for mission-critical NPI iterations, low-loss high-speed communications, and stringent thermal dissipation thresholds.

ODM High-Density Interconnect HDI PCB from Trusted China Suppliers
Explore Product
China High-Quality 1-60 Layers Multilayer PCB from China Suppliers
Explore Product
ODM High-Frequency RF & Microwave PCBs Low Loss Signal Control
Explore Product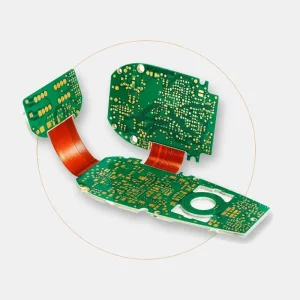
ODM China Rigid Flex PCB Single & Double-Sided Multilayer Factory
Explore Product
ODM High Frequency PCB Solutions: Minimize Signal Loss & Crosstalk
Explore Product
Buy High Thermal Conductivity Aluminum PCB Superior Performance
Explore Product
ODM PCB Prototype Manufacturer, Fast Engineering Verification
Explore Product
OEM High TG PCBs for Automotive, Aerospace, and Defense Applications
Explore ProductCommercial Status of Prototype PCB Manufacturing: The Speed-to-Market Imperative
In high-velocity electronic hardware engineering, the prototype printed circuit board stage is no longer a secondary fabrication step—it is the strategic linchpin determining enterprise valuation and market survival.
Compression of the NPI Horizon
Global hardware development cycles have contracted from an historical average of 18 months down to sub-90-day execution sprints. Tier-1 engineering firms require high-mix low-volume (HMLV) fabrication partners capable of delivering verified, multi-layer functional prototypes within 48 to 72 hours, bypassing long tooling queues while maintaining zero defect rates under IPC Class 2 and Class 3 specifications.
- 48-Hour expedited lamination for up to 32 layers
- Immediate engineering CAM DFM review
The Shenzhen Supply-Chain Concentrator
The industrial concentration across Shenzhen's Bao'an and Fuhai industrial clusters represents an unmatched engineering node. Integrating raw copper clad laminate (CCL) synthesis, high-precision laser direct imaging (LDI), dedicated chemical plating lines, and same-day component warehousing eliminates the geographic and logistical friction common to Western and regional assembly houses.
- Immediate access to local franchise component hubs
- Sub-15-minute raw material freight routing
De-Risking Capital Allocation
Deploying production-grade tooling on unverified schematics causes catastrophic capital burn. Modern prototype printed circuit board factories act as critical operational filters: running rigorous Design for Manufacturing (DFM) and Design for Assembly (DFA) analytics that preemptively resolve annular ring breakouts, solder bridging, and thermal traps prior to high-volume commitments.
- Sub-0.35mm pitch BGA breakout validation
- First Article Inspection (FAI) reports with cross-sectioning
SPI, AOI, & 3D AXI automated inline verification
Expedited turnaround for high-layer count prototypes
High-precision placement for extreme miniaturization
Rigid, rigid-flex, and hybrid RF material pressing
Industry Development Trends: The Next Architecture of Circuit Fabrication
As microelectronics shift toward edge artificial intelligence, silicon carbide (SiC) switching, and sub-terahertz radio frequencies, prototype circuit board suppliers must adapt their physical processes.
Any-Layer HDI & Sub-50µm Geometry
Traditional mechanical drilling hits physical limits at 0.15mm hole diameters. Next-generation prototype factories deploy UV and CO2 laser drilling to produce 50-75µm microvias in staggered, stacked, and via-in-pad copper-filled (VIPPO) structures. This enables dense routing around high-pin-count BGA chips (≤0.35mm pitch) typical of advanced AI processors and edge compute units.
Low-Dk / Low-Df Hybrid RF Architectures
High-frequency communications (5G mmWave, 77GHz automotive radar, satellite payloads) require dielectric constant (Dk) tolerances tighter than ±0.05 and dissipation factors (Df) down to 0.0019. Modern suppliers utilize composite multi-stack press cycles—bonding low-loss Rogers or Taconic PTFE laminates directly to standard FR-4 cores to optimize RF integrity while managing bill-of-materials costs.
Thermal Dissipation & Heavy Copper
Wide-bandgap power semiconductors (GaN/SiC) in EV inverters and high-density power converters operate at unprecedented current densities. Prototype manufacturing incorporates 3oz to 10oz heavy copper layers combined with aluminum or copper-substrate metal cores, thermal via arrays, and ceramic-filled prepregs to manage thermal dissipation exceeding 3.0 W/m·K.
AI-Powered Closed-Loop CAM & MES
Manual engineering data preparation is a bottleneck in quick-turn prototyping. Modern factories leverage automated CAM software that algorithmically extracts IPC netlists, adjusts copper etch compensation based on historical chemistries, and outputs direct digital imaging (LDI) code. This eliminates operator error and synchronizes the physical build with cloud-based Manufacturing Execution Systems (MES).
Mission-Critical Application Scenarios: Tuned Engineering Profiles
Prototyping demands sector-specific calibration across dielectric behavior, vibration survivability, thermal endurance, and surface passivation.
Aerospace & Avionics
Class 3/A high-reliability multilayer rigid and rigid-flex builds with TG180-TG260 polyimide substrates, compliant with IPC-6012DS standards to resist outgassing and vibration-induced micro-cracking.
Automotive & EV BMS
Heavy copper circuitry engineered for battery management systems (BMS) and motor inverters, qualified through thermal cycling (-40°C to +150°C) and comparative tracking index (CTI ≥ 600V) compliance.
Medical Diagnostics
Ultra-dense flex and rigid-flex configurations utilizing biocompatible ENIG/ENEPIG plating, optimized for portable ultrasound scanners, telemetry devices, and surgical robotic feedback systems.
Telecom & Radar
Phase-matched microstrip and coplanar waveguide architectures fabricated on ceramic-filled hydrocarbons, guaranteeing controlled impedance (±5%) for 5G/6G active antenna arrays and drone jammers.
Technical Roadmap & Future Outlook: 2026 to 2032
The boundary between integrated circuit packaging (OSAT) and bare PCB fabrication is dissolving. Prototyping suppliers are evolving to support advanced heterogenous integration schemes.
Substrate-Like PCB (SLP) & mSAP
Adoption of modified semi-additive processes (mSAP) enables copper line width and spacing down to 25/25µm on standard FR-4-compatible carriers. This bridges traditional PCB routing with semiconductor substrate densities, permitting direct micro-bump packaging without specialized interposers.
Embedded Passives & Active Dies
Embedding bare silicon dies, planar inductors, and thin-film capacitors directly inside inner prepreg layers. This eliminates surface parasitic inductance, shrinks board footprint by up to 40%, and mitigates thermal hotspot concentrations through direct planar heat sinks.
Optoelectronic & Circular Substrates
Integration of optical waveguides directly into the multilayer stack for terabit chip-to-chip interconnects, bypassing copper's high-frequency RC loss. Concurrently, recyclable vitrimer resins and bio-based epoxy systems will enable low-carbon closed-loop copper and fiber extraction.
| Process Parameter | Standard Prototype Class | Advanced HDI / High-Speed | Aerospace / Mission-Critical |
|---|---|---|---|
| Layer Count Range | 1 – 12 Layers | 14 – 40+ Layers (Any-Layer) | 4 – 60 Layers (Hybrid Pressed) |
| Min Trace / Space (L/S) | 3.5 / 3.5 mil (89 / 89 µm) | 1.8 / 1.8 mil (45 / 45 µm) | 2.5 / 2.5 mil (63 / 63 µm) |
| Min Laser Hole Size | 0.20 mm (Mechanical) | 0.075 mm (UV/CO2 Laser) | 0.10 mm (Laser VIPPO) |
| Controlled Impedance | ±10% Standard | ±5% High-Precision | ±5% Verified via TDR coupon |
| Surface Finishes | HASL, Lead-Free HASL, ENIG | ENEPIG, Immersion Silver, OSP | Hard Gold (30-50µ"), ENEPIG |
| Testing Protocols | Flying Probe (100% Netlist) | 4-Wire Kelvin, 3D AOI | Thermal Shock, X-Ray, Cross-Section |
Macro Industry Solutions: Unifying Fabrication, Sourcing, & SMT Assembly
Procuring bare boards from one shop, components from disparate distributors, and assembly from a third contract manufacturer introduces compounding risks. Turnkey prototype manufacturing provides a single accountable pipeline.
Authorized Component Procurement
Overcoming supply chain instability requires direct partnerships with tier-1 semiconductor manufacturers (TI, ADI, STMicroelectronics, Microchip, Murata). An in-house incoming quality control (IQC) protocol checks every component lot through microscope inspection, acetone decapsulation verification, and pin-to-ground resistance measurements to eliminate counterfeit parts.
Agile SMT Placement Lines
Featuring Yamaha and Panasonic high-speed pick-and-place lines, prototype setups transition seamlessly from ultra-dense 01005 chips to 0.3mm pitch micro-BGAs and irregular edge connectors. Dedicated 10-zone nitrogen reflow ovens permit per-assembly thermal profile configuration, matching specific solder paste formulations without thermal degradation of adjacent sensitive silicon.
Comprehensive Inline Quality Assurance
High reliability demands automated inspection at every fabrication stage: 3D Solder Paste Inspection (SPI) to detect volume deviations before placement, pre- and post-reflow Automated Optical Inspection (AOI) to flag component shifts, and 3D Automated X-ray Inspection (AXI) to verify voiding levels under BGA solder balls remain well below 15% thresholds.
Frequently Asked Questions: Prototype PCB Engineering & Sourcing
Authoritative technical answers to common questions asked by hardware engineers, procurement specialists, and product managers.
To execute a full turnkey build with zero CAM delay, provide RS-274X Gerber or ODB++ files, NC drill files, an exact bill of materials (BOM) including manufacturer part numbers (MPN) and vendor designations, an XY pick-and-place centroid file, and mechanical assembly drawings detailing any special connector clearances or conformal coating keep-out zones.
Hybrid pressing pairs materials with differing coefficients of thermal expansion (CTE) and resin glass transitions (e.g., Rogers 4350B paired with Shengyi FR-4). Delamination is prevented by using specialized bonding prepregs (such as Rogers RO4450 series), adjusting the multi-stage press heating ramp rate, and standardizing plasma surface activation across inner PTFE layers before copper plating.
Engineering prototype runs have a true MOQ of 1 piece, scaling up to 500 units for pilot validation. Standard lead times for double-sided bare boards begin at 24 to 48 hours. Turnkey PCBA runs—inclusive of component procurement, stencil laser-cutting, SMT assembly, and functional testing—typically clear shipment within 3 to 9 working days, depending on parts availability.
IPC Class 2 covers commercial electronics where continuous performance is required, permitting minor visual variations and non-critical annular ring breakout. IPC Class 3 applies to mission-critical, aerospace, and medical equipment demanding uninterrupted uptime in harsh environments. Class 3 mandates zero annular ring breakout, thicker plated-through-hole (PTH) copper barrels (≥1 mil/25µm), tighter dielectric clearance, and formal microsection coupon reporting.
Automated DFM software parses CAD data before physical processing begins, identifying missing solder mask clearances, trace-to-copper clearances below etch limitations, thermal relief gaps, and acute copper acid traps. Resolving these issues algorithmically during CAM pre-flight prevents line stoppages and avoids scrapped builds.
Yes. Via-In-Pad Plated Over (VIPPO) is a core capability for fine-pitch BGAs. We mechanically drill or laser-ablate the microvia, electroplate the barrel wall, fill the hole completely with non-conductive epoxy resin, planarize the surface flat with chemical-mechanical polishing (CMP), and cap the top with an electroplated copper pad suitable for void-free SMT solder joints.
Precision Prototype Solutions: Active Production Series (Part II)
From single-board embedded computers to heavy copper industrial power circuits and aerospace-grade high-Tg laminates.
China High Density Interconnect (HDI) PCB Leading Factory Solutions
Explore Product
ODM High TG PCB Suppliers & Factory in China for Defense Industries
Explore Product
High-Quality China Raspberry Pi HAT: Affordable Mini SBC Modules
Explore Product
China PCB Prototype Suppliers Fast Manufacturing Solutions Leading Factory
Explore Product
ODM High-Quality RF & Microwave PCBs for Mobile Phones & Radar
Explore Product
Famous Heavy Copper PCB Durable Components for Power Converters
Explore Product
Famous High-Quality 1-60 Layers Multilayer PCB Fastest 48-Hour Turns
Explore Product