
Precision OEM Fabrication & Specialized Circuit Solutions
Engineered for high-frequency signal integrity, thermal dissipation, and sub-miniaturized embedded architectures.


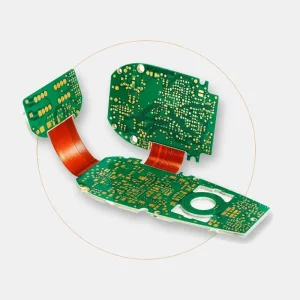

The Global OEM Circuit Board Ecosystem: Supply Resilience & Micro-Electronics Migration
Analyzing shifts in global electronics manufacturing services (EMS), component lead times, and why the Pearl River Delta remains the central engineering nexus for high-mix, fast-turn electronics.
The Modern Macro Paradigm: Beyond Traditional Brokerage to Single-Sourced Engineering Accountability
In contemporary high-reliability electronics procurement, the historical segregation between bare PCB fab houses, component brokers, and surface-mount technology (SMT) assemblers introduces compounding risks. Supply chain volatility, uncoordinated thermal profiles, and decentralized quality auditing frequently cause prolonged NPI cycles and catastrophic field failures.
As original equipment manufacturers (OEMs) develop miniaturized, ultra-dense architectures across IoT edge gateways, advanced driver-assistance systems (ADAS), and industrial avionics, PCB manufacturing requires immediate integration between board physics and robotic assembly tolerances. Operating an 8,000 m² advanced electronics assembly facility located within Shenzhen’s high-tech industrial cluster (Anda Electronic Industrial Zone, Fuhai Subdistrict, Bao'an District), Shenzhen ICSLOVE Technology Co., Ltd. (operating internationally as PCB ADEPT) solves this fragmentation by uniting raw laminate fabrication, global franchised component procurement, IPC Class 3 SMT mounting, and complete mechatronic box-build testing under a unified ISO 9001 quality framework.
Tier-1 Component Integrity
Uncompromising procurement channels strictly vetted for active ICs (TI, Analog Devices, STMicroelectronics, Microchip) and passive passives (Murata, TDK, Samsung, TE Connectivity). Every reel is tracked with lot date codes in our automated Manufacturing Execution System (MES) to prevent gray-market ingress.
Controlled Thermal & Signal Stackups
Substrates ranging from standard FR-4 (high TG170/TG180), polyimide flex, to high-frequency hydrocarbon ceramics (Rogers 4350B, 4003C, Taconic) ensuring tight dielectric constant (Dk) tolerances and low dissipation factors (Df) across multi-gigahertz operations.
Sub-Millimeter Inspection Matrix
Every board passes automated 3D Solder Paste Inspection (SPI), multi-angle Pre-Reflow AOI, Post-Reflow 3D Optical Inspection, First Article Inspection (FAI), and real-time Boundary Scan / In-Circuit Testing (ICT) to eliminate non-visible BGA solder bridge voids.
PCB Fabrication & Assembly Technical Specification Matrix
Verified manufacturing process parameters across HDI microvias, copper weight classifications, surface metallurgy, and robotic SMT lines.
| Manufacturing Parameter | Standard Commercial Capability | Advanced / High-Density Capability | Verification & Test Standard |
|---|---|---|---|
| Layer Count Range | 1 – 8 Layers (FR4, CEM-1, Aluminum) | 10 – 60 Layers (Multi-lamination HDI) | Cross-section microsectioning / AOI |
| Flex & Rigid-Flex Builds | 1 – 4 Flex Layers (PI Substrate) | Up to 22 Layers Rigid-Flex (4x HDI cycles) | IPC-6013 Class 3, Dynamic Bend Stress |
| Min. Line Width / Spacing | 3.0 mil / 3.0 mil (75 μm) | 1.8 mil / 1.8 mil (45 μm, mSAP process) | Optical Laser Micrometry & AOI |
| Minimum Microvia Diameter | 0.20 mm (0.008") Mechanical Drill | 0.075 mm (0.003") UV Laser Drilling | X-Ray Inspection & Barrel Copper Gauge |
| SMT Component Placement | 0402, 0603, 0805, QFP, SOP | 01005 passives, 0.3mm pitch BGA, PoP | YAMAHA Multi-Vision + 3D Post-AOI |
| Surface Finishes (Passivation) | HASL, Lead-free HASL, OSP | ENIG, ENEPIG, Hard Electrolytic Gold | XRF Plating Thickness Analyzer |
| Maximum Finished Copper | 1 oz – 3 oz Copper foil | 4 oz – 12 oz (Heavy Copper for Power) | Thermal Cycling & Resistance Metering |
| Controlled Impedance | ±10% Standard Tolerance | ±5% Tight RF / High-Speed Differential | Time-Domain Reflectometry (TDR) Testing |
Engineering Rule of Thumb for DFM Optimization
Thermal dissipation and aspect ratios govern PCB yield. For boards with BGA balls below 0.4mm pitch, our engineering team mandates via-in-pad plated over (VIPPO) structures with copper filling rather than standard resin-capped plugs. This eliminates outgassing during reflow, preserves coplanarity across complex thermal profiles, and secures 99.8% first-pass SMT assembly yields.
HDI Multi-Lamination & Any-Layer Interconnects
As smart sensors and compact computing engines concentrate processing silicon into 0.35mm pitch wafer-level packages, conventional mechanically drilled through-holes fail to satisfy routing density. We implement microvia laser drilling with staggered and stacked copper-filled architectures (1+N+1 to 4+N+4 structures), eliminating capacitive stubs and preventing high-speed signal reflections across 56Gbps+ SerDes communication backplanes.
Thermal Management: Insulated Metal & Heavy Copper
Power conversion systems, electric vehicle traction inverters, and high-lumen luminaires require rapid thermal conductive dissipation away from MOSFET junctions. Our facility manufactures insulated metal substrates (IMS) with aluminum and copper base plates achieving thermal conductivities up to 8.0 W/m·K. Heavy copper configurations up to 12 oz ensure current-carrying integrity without board delamination under severe in-rush loads.
Macro Industry Solutions & Sector-Specific Deployments
Deep-dive domain implementations across specialized fields demanding rigorous standards compliance and structural durability.
Anti-Drone & Microwave Countermeasures
Modern electronic warfare and counter-unmanned aerial systems (C-UAS) rely on multi-channel RF power amplifiers and high-rejection planar filters operating in S, C, and Ku bands. We manufacture hybrid stackups combining Rogers 4350B ceramic hydrocarbon cores with FR-4 sub-layers, minimizing insertion loss while reducing substrate costs. Gold wire bondable finishes (ENEPIG) ensure structural wire stability during high shock pulses.
Automotive Power & ADAS Sensor Platforms
Autonomous vehicle radar and battery management systems (BMS) operate under extreme vibration and thermal swings ranging from -40°C to +150°C. Fabricated strictly to high-Tg standardizations (TG170, TG180), our automotive assemblies utilize lead-free wave soldering, conformal coating against dendritic growth, and 100% automated optical inspection to uphold functional safety compliance.
Industrial Robotics, PLC & Edge Gateways
Factory automation infrastructure necessitates prolonged operating life cycles extending beyond 10–15 years. We build ruggedized single-board computers, Raspberry Pi industrial HAT expansions, and multi-channel isolated I/O modules protected against high electrical fast transients (EFT) and heavy industrial electromagnetic disturbances.
Precision Medical & Diagnostic Wearables
Ultra-miniature biometric trackers and clinical diagnostics mandate flexible and rigid-flex interconnects capable of million-cycle flexure without conductor fatigue. Utilizing adhesiveless copper-clad polyimide substrates, our cleanroom assembly lines support fine-pitch SMT placement (down to 01005 passives) under stringent static and particulate controls.
Green Energy Inverters & ESS Storage Units
Solar inverters, high-capacity bidirectional DC-DC converters, and grid storage control systems handle massive ampacity. We provide thick-copper busbar-embedded circuit boards and multi-layer aluminum configurations that isolate high galvanic voltages while rapidly dissipating Joule heat across heavy switching transients.
Satellite Ground Stations & Aerospace Radios
LEO constellation antennas and airborne transceivers operate within harsh radiation and altitude environments. Our fabrication process uses certified low-outgassing PTFE substrates, electrolytic hard gold plating on card edge connections, and vacuum baking protocols to prevent entrapped moisture volatilization during low-pressure operation.
End-to-End Advanced Production & Verification Workflow
From initial Gerber DFM clearance to robotic solder paste deposition, high-speed component mounting, and final functional verification.
Engineering DFM / DFA Audit
Every Gerber, ODB++, and BOM submission undergoes deep automated algorithmic clearance: identifying acid traps, copper slivers, insufficient solder dam margins, and package thermal mismatches prior to tooling release.
Precision Solder Paste & 3D SPI
Using laser-cut electro-polished nickel stencils, solder paste is applied via automated printers. 3D SPI instantly scans paste height, area, and volume to stop bridge or insufficient solder defects before components are placed.
Dual-Gantry High-Speed SMT
Six automated YAMAHA mounters place ultra-miniature 01005 passives alongside complex 1,500-pin BGAs with sub-25 μm positional repeatability. Pre-reflow optical checks eliminate component polarity misalignments.
Multi-Zone Reflow & 3D AOI
10-zone nitrogen-purged reflow ovens track custom thermal profiles per board thermal mass. Post-reflow 3D AOI and automated X-ray inspection (AXI) inspect hidden BGA solder balls for micro-voiding under IPC-A-610 Class 3.
Strategic Sourcing & Anti-Counterfeit Verification Infrastructure
Our dedicated procurement team brings over a decade of supply relationships with authorized global semiconductor distributors (Arrow, Digi-Key, Mouser, Avnet) and direct Asian franchised agents. Incoming components undergo microscopic die marking verification, pin oxidation analysis, and LCR parametric testing to defend your equipment against grey-market non-conformance.
Engineering Inquiries: Circuit Fabrication & Turnkey Assembly
Detailed technical responses addressing design specifications, quality assurance, procurement governance, and prototype transitions.
What specific Gerber and assembly files are required for an instant DFM and turnkey quote?
To produce an authoritative quote and complete comprehensive DFM review, provide:
- Gerber RS-274X or ODB++: Containing all copper layers, solder mask, silkscreen, drill files (Excellon format), and board mechanical outline.
- Bill of Materials (BOM): Formatted with explicit Manufacturer Part Numbers (MPN), approved alternate manufacturers, reference designators, package footprints, and description.
- Pick and Place / Centroid File: ASCII text specifying X-Y coordinates, board rotation angle (theta), and layer side (Top/Bottom).
- Assembly Fabrication Drawings: Denoting special instructions (e.g., conformal coating keep-out zones, press-fit connector tolerances, critical impedance nets).
How do you manage controlled impedance for high-speed differential pairs and RF microstrip lines?
We model line geometry using Polar Instruments Si9000 field solvers during the pre-engineering stage. Stackups are calibrated against measured prepreg dielectric constants (Dk) at operating frequencies. Finished boards integrate impedance test coupons on manufacturing break-away rails, which undergo 100% Time-Domain Reflectometry (TDR) measurement to confirm values within ±5% or ±10% tolerances with documented inspection reports.
What is your policy and screening methodology regarding electronic component obsolescence and long lead times?
During our initial BOM health check, our component engineers flag End-of-Life (EOL), Not Recommended for New Designs (NRND), and volatile lead-time devices. We propose drop-in pin-compatible replacements (e.g., recommending equivalent automotive-grade microcontrollers from STMicroelectronics, Microchip, or Texas Instruments) or pin-to-pin compatible active alternates that preserve software firmware functionality while mitigating supply disruptions.
What non-destructive test methods are deployed to verify solder integrity under BGAs and QFN thermal pads?
Every lot containing bottom-terminated components (BTC), Quad Flat No-leads (QFN), and Ball Grid Arrays (BGA) undergoes high-resolution transmission 3D Automated X-Ray Inspection (AXI). We mathematically measure solder voiding percentages (keeping voids strictly under 15–20% in compliance with IPC Class 3 standards) and inspect for bridging, micro-solder balls, or head-in-pillow defects that remain invisible to optical AOI.
Can you manufacture hybrid multilayer boards combining Rogers high-frequency substrates with standard FR-4?
Yes. We frequently fabricate hybrid PTFE/hydrocarbon and FR-4 multi-layer boards. This allows engineers to place high-frequency RF traces (such as 24GHz or 77GHz radar front-ends) on low-loss Rogers 4350B outer layers while routing digital controls, power management, and low-speed signals on cost-effective internal FR-4 layers. Thermal expansion matching (CTE) and prepreg rheology are calibrated to prevent inner-layer delamination during reflow.
What assembly capabilities do you provide for full electro-mechanical box-build production?
Beyond surface mount (SMT) and dual inline package (DIP) wave soldering, our Shenzhen production facility supports complete box-build integration: CNC aluminum milling, plastic injection molding, wire harness crimping, silicone potting, MCU firmware flashing via automated programmers, thermal aging burn-in cycles, and custom retail or industrial packaging with barcode traceability.
High Thermal, Heavy Copper & Specialized Flex Circuitry
Specialized laminate fabrications engineered for high currents, dynamic bend cycles, and harsh environments.



Initiate Your OEM Circuit Board Project Consultation
Transfer your Gerber archives, stackup specifications, and complete BOM requirements to our Shenzhen manufacturing center for a complete DFM report and production quote within 24 hours.