ODM China Suppliers for Rigid Flex PCB - Single, Double-Sided, 4-16 Layer & Complex Multi-Layer Factory Solutions Manufacturer, Pricelist
Product Description
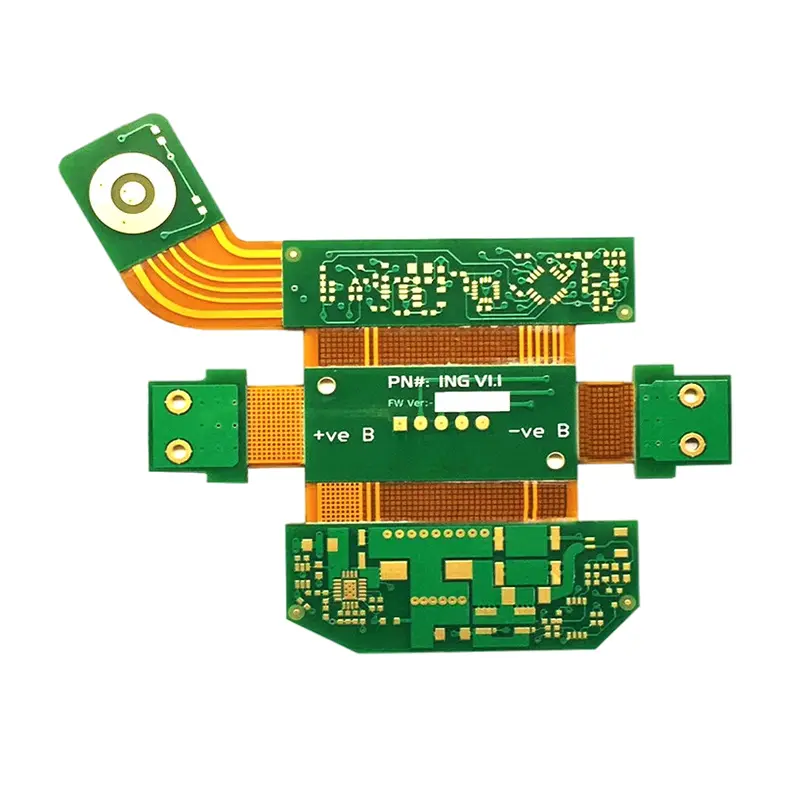
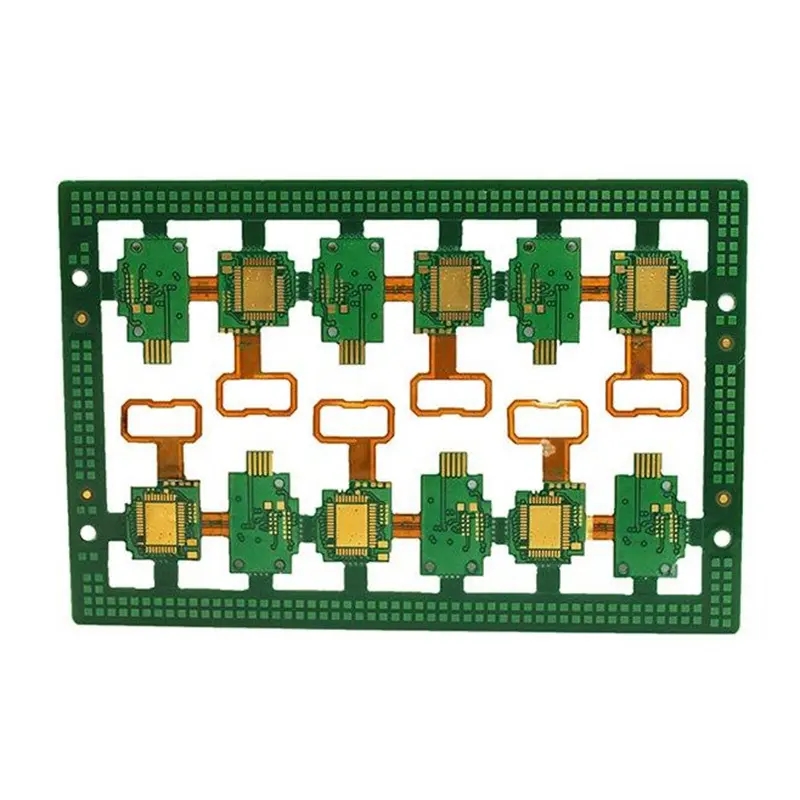
What is Rigid Flex PCB?
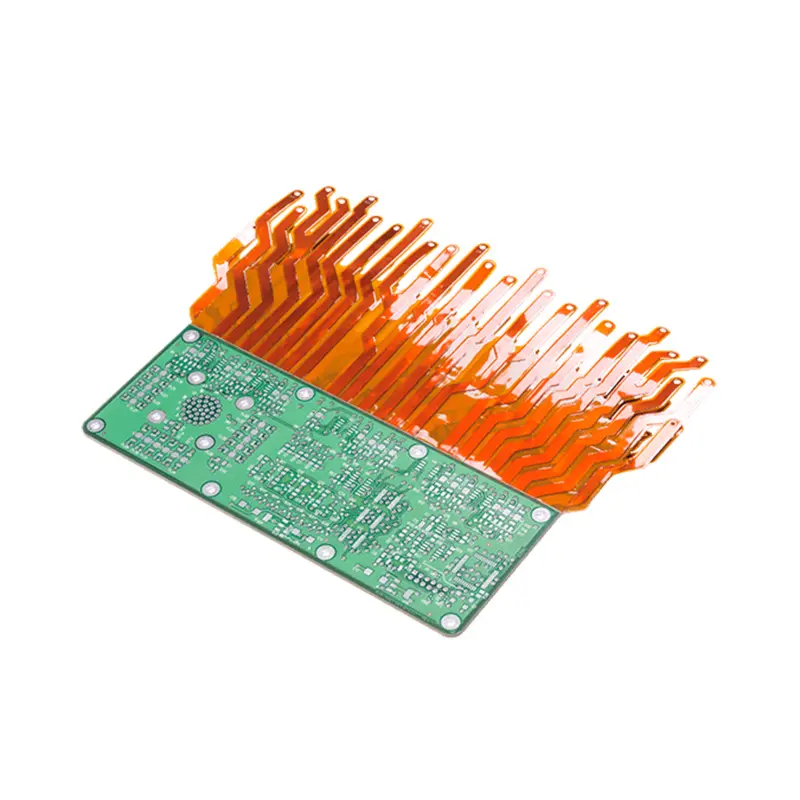
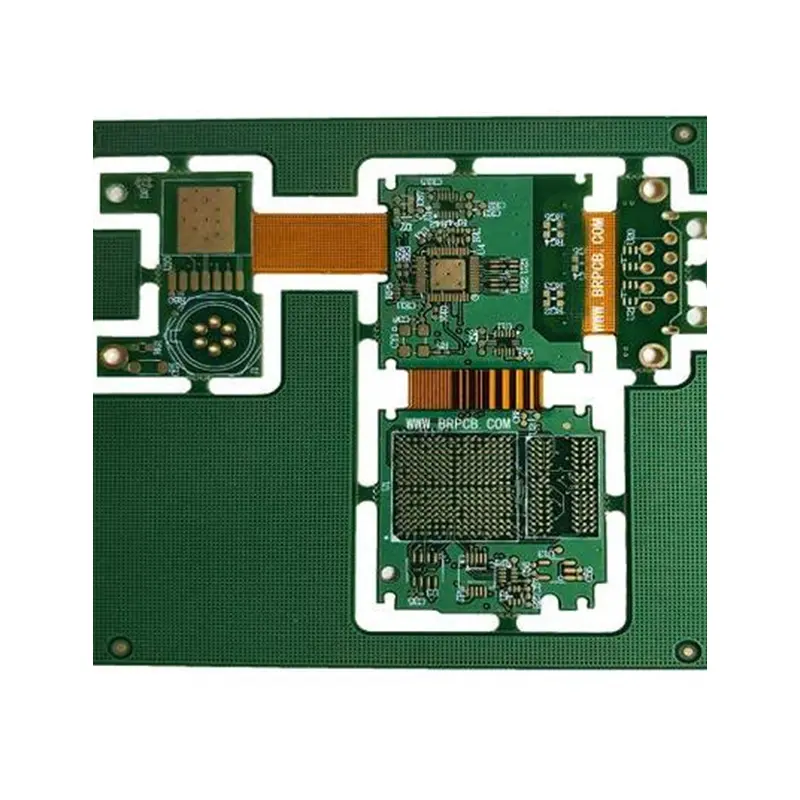
Core Components & Structure
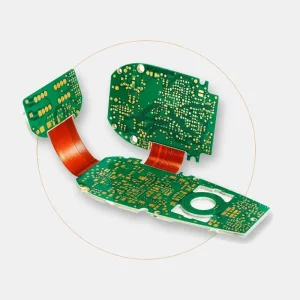
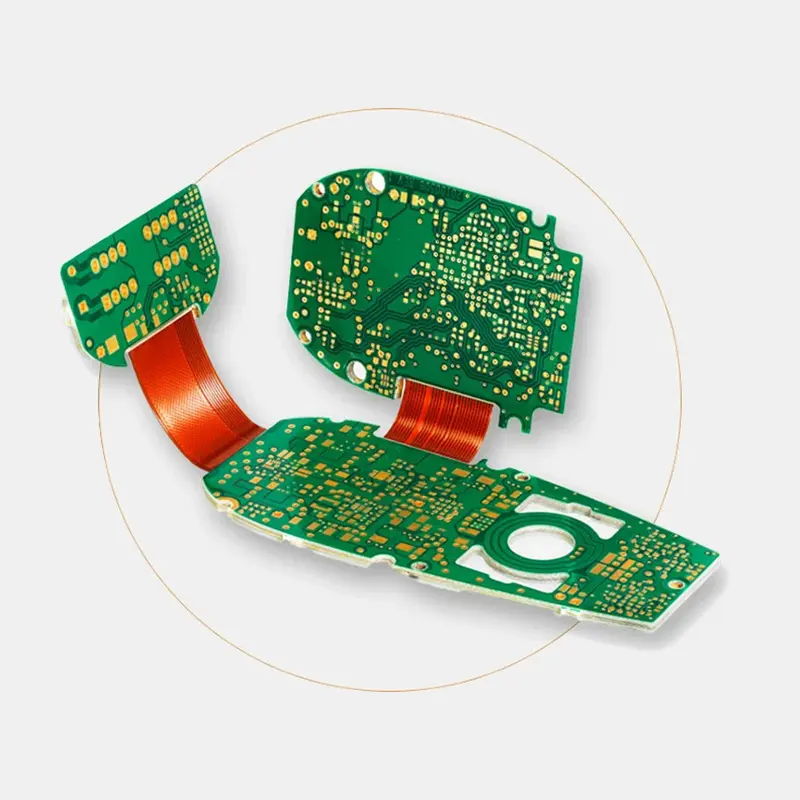
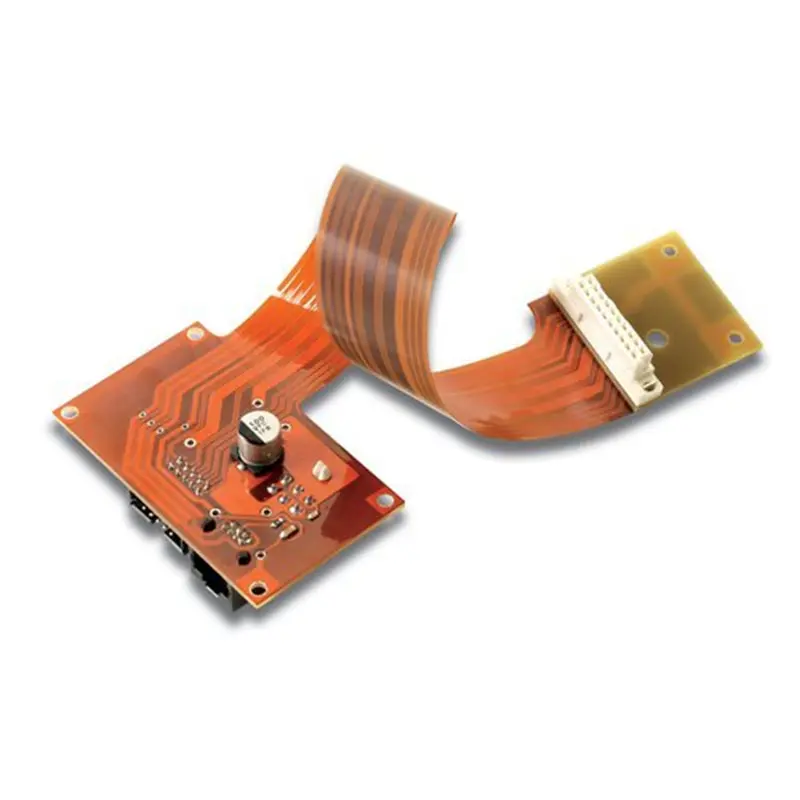
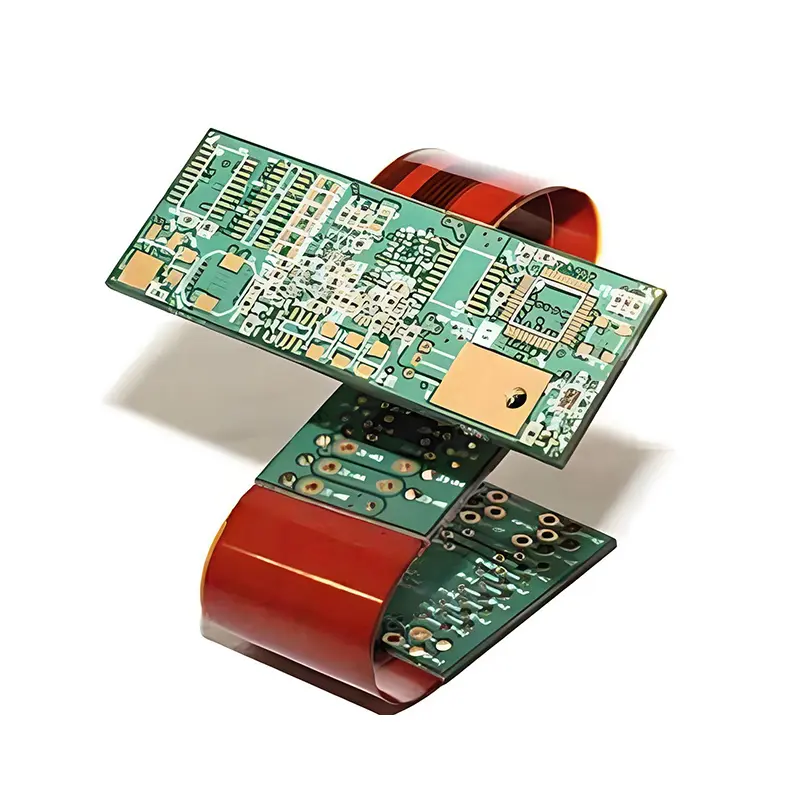
A typical rigid-flex PCB consists of three key parts, layered and bonded together through specialized processes:
-
Rigid sections: Made of traditional rigid substrate materials (e.g., FR-4, a glass-reinforced epoxy resin). These parts provide mechanical stability to support electronic components (such as chips, resistors, capacitors) and ensure structural integrity.
-
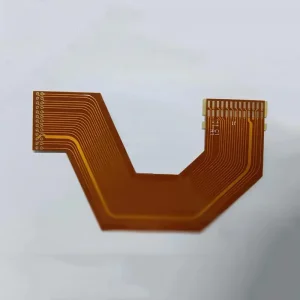
Flexible sections: Composed of flexible substrates (common materials include polyimide, PI, or polyester, PET). These parts are thin, lightweight, and can be repeatedly bent, folded, or twisted, allowing the board to adapt to irregular shapes or dynamic environments (e.g., parts that need to open/close or vibrate).
-
Interconnect layers: The rigid and flexible sections share internal conductive copper layers (signal traces, power lines, ground planes) that are seamlessly connected. This eliminates the need for wires, connectors, or solder joints between separate rigid and flex boards, reducing failure risks.
Key Advantages
-
Space & weight savings: They can be folded to fit into tight, complex enclosures (e.g., foldable phones, wearables), reducing the overall size and weight of electronic devices.
-
Enhanced reliability: Fewer connectors and solder joints mean fewer potential points of failure (e.g., loose connections from vibration or aging), which is critical for high-reliability applications like aerospace equipment.
-
Simplified assembly: Integrating multiple rigid and flex parts into one board streamlines the manufacturing process, reducing assembly time and human error.
-
Improved performance: Continuous copper traces minimize signal loss and electromagnetic interference (EMI), ensuring stable signal transmission—essential for high-frequency devices.
Common Applications
Rigid-flex PCBs are indispensable in industries where space, reliability, and flexibility are paramount:
-
Consumer electronics: Foldable smartphones, smartwatches, laptops, cameras, and earbuds (e.g., the hinge area of foldable phones uses flexible sections to connect rigid display and battery boards).
-
Aerospace & defense: Satellites, aircraft avionics, and military equipment (they withstand extreme temperatures, vibration, and space constraints).
-
Automotive: In-vehicle infotainment systems, sensor modules, and advanced driver-assistance systems (ADAS) (adapt to the curved or confined spaces of car interiors).
-
Medical devices: Portable monitors, implantable devices (e.g., pacemakers), and diagnostic equipment (offer biocompatibility, miniaturization, and durability).
Would you like me to elaborate on the manufacturing process of rigid-flex PCBs or the material selection criteria for different applications?
The type of rigid flex PCB?
The classification dimensions of Rigid-Flex PCB (Rigid-Flex PCB) are numerous. The core classification can be based on structural form, flexible area characteristics, number of layers, and adaptability to application scenarios, etc. Different categories correspond to different process difficulties and usage requirements. The following are the mainstream classification methods and detailed explanations in the industry.
This is the most commonly used classification method. The core basis is the connection mode and layout characteristics of the rigid and flexible areas, which directly determine the installation compatibility of the PCB.
Single flexible zone rigid-flexible combined PCB: The entire board has only one continuous flexible zone, with both ends or one end connected to the rigid board. The flexible zone is mainly used to achieve "folding" or "turning" functions, such as the flat cable connecting the laptop screen to the main unit and the circuit board of some headphones. It has a simple structure and low cost, and is the most common basic model in consumer electronics.
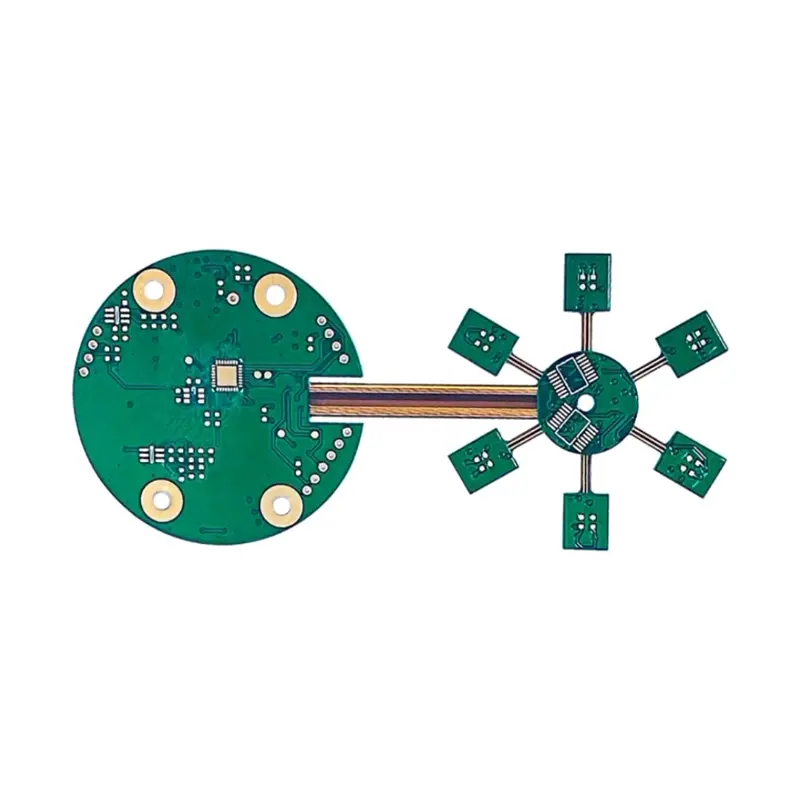
Multi-flexible zone rigid-flexible combined PCB: It contains two or more independent flexible zones and forms a complex structure through the series connection of multiple rigid boards. It is suitable for equipment that requires multi-directional bending and decentralized layout, such as industrial sensor modules (multiple detection units are connected to the main control rigid board through flexible areas) and lens module circuit boards for multi-camera mobile phones.
Three-dimensional rigid and flexible combined PCB: The flexible area can achieve bending and twisting in three-dimensional space, while the rigid area is distributed in different spatial planes and seamlessly connected through the flexible area. It is mostly used in equipment with extremely compact space and irregular shapes, such as the fuselage control board of unmanned aerial vehicles and the integrated circuit boards in car instrument panels, which can maximize the utilization of three-dimensional space.
The main distinction is whether the flexible part can be repeatedly bent to adapt to static installation or dynamic working scenarios.
Static rigid-flex combined PCB: The flexible area is only bent and shaped once during assembly, maintaining a fixed form during subsequent use and not subject to repeated deformation. For instance, the frame of a foldable phone is connected to the circuit board. After assembly, the flexible area remains in a fixed folded state for a long time. The core requirement is the structural stability after shaping.
Dynamic rigid-flex PCB: The flexible area needs to withstand long-term and repeated bending, twisting and other dynamic actions, which requires extremely high fatigue resistance and copper layer adhesion of the flexible substrate. Typical applications include the paper feed mechanism circuit board of printers and the opening and closing components of wearable devices (such as foldable watches), which need to meet the requirement of no failure after tens of thousands of bends.
Similar to ordinary PCBS, they are classified by the number of layers of conductive circuits. The more layers there are, the higher the integration degree and the more complex the process.
Single-layer rigid-flex PCB: It contains only one layer of conductive copper foil, and the flexible and rigid areas share this layer of circuit. It has the simplest structure and the lowest cost, but its function is single. It is only suitable for low-complexity circuits, such as the control boards of simple toys and the connection lines of small remote controls.
Double-layer rigid-flexible combined PCB: It consists of two layers of conductive copper foil, with interlayer conduction achieved through vias in the middle. The flexible area uses a flexible substrate, and the rigid area is equipped with a FR-4 core board. Taking into account both cost and practicality, it is widely used as a peripheral module for smart phones and tablet computers.
Multi-layer rigid-flex PCB: The number of layers is ≥4, usually composed of alternating superposition of "rigid layer - flexible layer - rigid layer", and it has a power layer, ground layer and signal layer inside. It has a high degree of integration and can achieve complex signal transmission and power management. It is suitable for high-end electronic devices, such as satellite circuit boards in aerospace and precision detection mainboards in medical equipment.
Specialized types designed for extreme environments or special needs, with additional customized requirements for materials and processes.
High-frequency rigid-flex combined PCB: It adopts flexible substrates with low dielectric constant and low loss (such as PTFE-modified polyimide), reducing attenuation and interference during signal transmission, and is suitable for high-frequency scenarios such as 5G equipment, radar systems, and satellite communication equipment.
High-temperature resistant rigid-flex combined PCB: The flexible substrate and adhesive are made of high-temperature resistant materials (such as special PI), which can operate stably within a temperature range of -55 ℃ to 200℃ or even wider. It is widely used in peripheral equipment of aero engines and industrial high-temperature sensors.
High-density interconnect (HDI) rigid and flexible combined PCB: By using micro-vias and fine line width and line spacing technologies, it enhances the line density and reduces the board size, making it suitable for miniaturized devices such as smartwatches and implantable medical devices (such as auxiliary circuit boards for pacemakers).
How to design rigid flex PCB?
The design and production of rigid-flex combined PCBS need to take into account both the structural stability of rigid PCBS and the bending adaptability of flexible PCBS. During the design stage, potential risks in subsequent production and use should be avoided. In the production stage, special process links need to be controlled to ensure the reliability and consistency of the product. The following are detailed design and production key points:
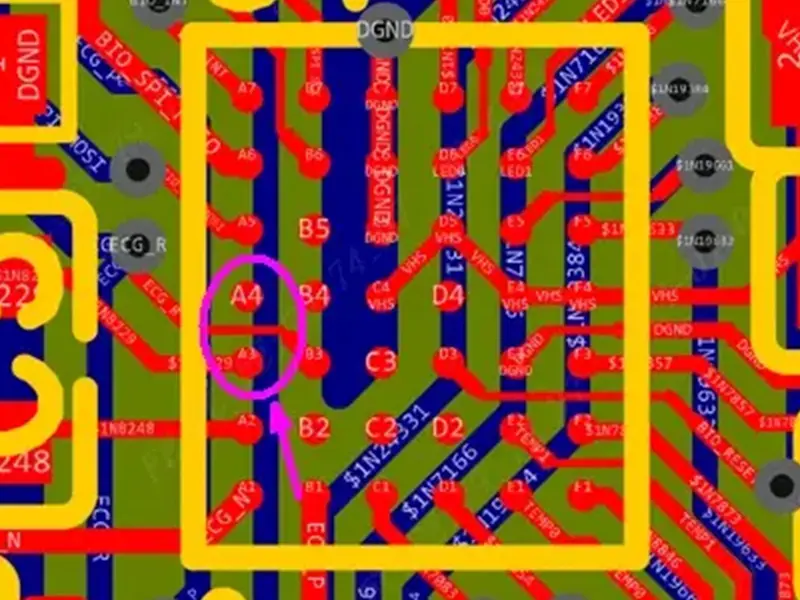
Design is the core of the quality of rigid-flex combined PCBS. It needs to take into account electrical performance, mechanical characteristics and production feasibility simultaneously, with a focus on the following aspects:
• Structural and layout design
The boundary between the rigid zone and the flexible zone is clear: A transition zone (usually 0.5-1mm) should be reserved at the boundary between the rigid zone and the flexible zone to prevent components, vias, and copper foils from crossing the boundary and to avoid cracking due to material differences during bending. The edges of the flexible zone need to be rounded (radius ≥1mm) to reduce stress concentration.
Flexible zone location and bending planning: The flexible zone should avoid high-stress areas. In dynamic bending scenarios, the bending radius should meet the requirement that "the minimum bending radius of the inner copper foil is ≥ 10 times the thickness of the flexible substrate, and that of the outer copper foil is ≥15 times". Static bending only requires one-time shaping, and the radius can be appropriately reduced. At the same time, avoid overlapping and bending in the flexible zone to prevent long-term compression from damaging the circuit.
The layout of components is reasonable: Heat-generating components (such as chips and resistors) should be concentrated in the rigid area and far away from the flexible area to avoid aging of the flexible substrate due to high temperature. Heavy-duty components (such as interfaces and sensors) need to be fixed in rigid areas, and reserved heat dissipation space and fixing holes should be provided.
• Line and layering design
The line direction is adapted to the bending direction: In the flexible zone, the line direction is preferred to be horizontal (parallel to the bending direction) to reduce the tensile/compressive damage to the copper foil during bending. Avoid setting dense thin lines and sharp-angled lines in the flexible area. The line width and spacing should be slightly larger than those in the rigid area (it is recommended that the minimum line width/spacing be ≥0.1mm).
Stacking structure optimization: For multi-layer rigid-flexible combined PCBS, the flexible layer should adopt a symmetrical structure (such as "rigid layer - flexible layer - flexible layer - rigid layer") to prevent the board from warping. Rigid core materials are prohibited in the flexible zone. The adhesive should be made of flexible materials (such as acrylic) to ensure bending performance.
Via and grounding design: Metallized vias are prohibited in the flexible zone. All vias must remain in the rigid zone and be at least 1mm away from the boundary of the flexible zone. Set up independent ground layers to reduce signal interference. In high-frequency scenarios, "microstrip line" or "ribbon line" structures can be adopted to optimize signal transmission.
• The material selection meets the requirements
Flexible substrate: For dynamic bending scenarios, choose polyimide (PI) with good fatigue resistance; for static scenarios, polyester (PET) with lower cost can be selected. High-frequency equipment should select PI substrates with low dielectric constants (such as PTFE-modified PI).
Copper foil and covering film: For flexible areas, rolled copper foil (with good ductility and bending resistance) is preferred, while for rigid areas, electrolytic copper foil can be used. The surface of the flexible zone should be covered with a flexible covering film (PI film), and the edge should extend 0.2-0.3mm beyond the copper foil to provide protection and insulation.
Key points of manufacturing
The production of rigid-flexible combined PCBS integrates the processes of rigid and flexible PCBS, and requires additional control over the connection links between rigidity and flexibility. The core points are as follows:
▶ Substrate pretreatment and lamination process
• Substrate cleaning: The surface of the flexible PI substrate is prone to adsorbing impurities. It is necessary to remove oil stains and oxide layers through plasma cleaning or chemical treatment to enhance the adhesion between the copper foil and the substrate. Rigid FR-4 substrates need to be dried and dehumidified to prevent air bubbles from forming during lamination.
• Precise lamination: During lamination, temperature, pressure and time need to be controlled. The bonding parameters of the flexible zone and the rigid zone should be set differently to prevent deformation of the flexible substrate or delamination of the rigid zone. The stepwise lamination method is adopted. First, the flexible layer is laminated, and then it is laminated with the rigid layer to ensure a tight interlayer bond.
▶ Circuit fabrication and etching control
• High-precision exposure: Flexible substrates are prone to stretching. Special fixtures should be used for fixation during exposure to prevent line deviation. The ultraviolet parallel light exposure machine is adopted to ensure the accuracy of the line pattern, especially to control the line width error in the flexible zone within ±0.02mm.
• Etching process optimization: Alkaline etching solution is used to treat the copper foil in the flexible zone. The etching speed is slightly lower than that in the rigid zone to prevent excessive etching from causing line breakage. After etching, it is necessary to clean it in time to avoid the residual liquid from corroding the substrate.
▶ Cutting and forming processes
• Flexible zone contour cutting: The flexible zone contour is processed by laser cutting (CO₂ laser or ultraviolet laser), with a smooth cut and no burrs, avoiding the tearing of the base material caused by mechanical cutting. When cutting, the laser power needs to be controlled to prevent damage to the internal circuits.
• Rigid zone forming: The rigid zone can be formed by CNC milling, and the edges need to be deburred and chamfered. The boundary between the rigid zone and the flexible zone needs to be ground a second time to ensure a smooth transition and reduce stress concentration during bending.
▶ Post-processing and quality inspection
• Surface treatment: Rigid areas can undergo surface treatments such as tin spraying, gold plating, and OSP to enhance soldering performance. The surface of the flexible zone is only protected by a covering film. High-temperature treatments such as tin spraying are prohibited to prevent deformation of the base material.
• Full-process inspection: During production, interlayer adhesion (through peel test) and line conductivity (flying probe test) need to be inspected. The finished products need to undergo bending tests (dynamic bending requires simulating tens of thousands of cycles) and high and low temperature environment tests to ensure stability and reliability in usage scenarios.
| RIGID FLEXIBLE PCB CAPABILITY | |||||
|---|---|---|---|---|---|
| RIGID FLEX PCB | Flex layers | Lamination structure≤4L;Book structure≤10L | Lamination structure≤4L;Book structure≤12L | ||
| Max. Panel Size(shipping) | 210MM*480MM | 460MM*480MM | |||
| FPC dielectric thickness | 2MIL、3MIL、4MIL | 1MIL | |||
| PTH rigid-flex transition area | ≤1.2MM | ≤1.0MM | |||
| Pattern spacing, rigid area to rigid-flex transition area | ≥1.2MM | ≥0.9MM | |||
| Rigid-Flex Structure | Typical structure、Flying tail structure、Multi-flex book structure、Two-flex lamination structure、Single-sided asymmetric structure,Asymmetric structure etc. | ||||