
Featured Turnkey PCB Hardware Systems
Explore our primary manufacturing lines optimized via advanced DFM engineering rules, strict thermal profiling, and IPC Class 2/3 certified fabrication controls.





The Strategic Mandate: Design for Manufacture (DFM) in Modern Electronics
Bridging the gap between conceptual Electronic Computer-Aided Design (ECAD) and physical assembly line physics to eliminate yield drop, thermal strain, and component obsolescence.
Fundamental Industry Reality: More than 82% of all premature board-level production halts and costly post-layout revisions are not caused by logical schematic flaws, but by unvetted physical manufacturability violations. When enterprise procurement teams look to buy PCB design for manufacture services, they are investing in the risk-reduction buffer that prevents costly line downtime, scrap cycles, and field-failure liabilities.
Proactive DFA & DFM Verification
Traditional electronic manufacturing treated layout and factory floor assembly as distinct silos. In contrast, modern Design for Assembly (DFA) integrates pick-and-place nozzle constraints, thermal relief pad symmetry, and component centroid clearances directly into the initial routing stage. This eliminates shadowing effects during infrared reflow and wave soldering.
Controlled Impedance & Signal Integrity
With high-frequency transceivers exceeding multi-gigabit throughputs, dielectric layer consistency and exact copper trace geometry dictate signal propagation integrity. DFM protocols evaluate copper etching undercut factors, differential pair coupling, and dielectric thickness tolerances (FR-4, Rogers, Megtron) to guarantee impedance within ±5% to ±7% margins.
Lifecycle & Sourcing Resilience
True DFM extends beyond bare-board etched copper to the bill of materials (BOM). Our Shenzhen sourcing engineering teams vet active parts against real-time global stock availability, lifecycle flags (NRND, EOL), and pin-to-pin footprint alternatives before mass tooling starts, preserving production continuity.
Global Commercial Landscape & Industrial Evolution
Navigating global supply chain realignments, the Shenzhen hardware acceleration ecosystem, and the technological parameters shaping modern electronics contract manufacturing.
The global printed circuit board and electronic manufacturing services (EMS) marketplace is undergoing a decisive architectural shift. Geopolitical factors, the rapid adoption of edge artificial intelligence, and the migration of automotive powertrains toward 800V high-voltage platforms have elevated DFM from a routine quality checklist to a competitive survival vector. Companies sourcing PCB fabrication and turnkey assembly can no longer afford the traditional "throw-it-over-the-wall" development cycle where layout designers produce Gerber files in isolation from the assembly floor.
Shenzhen, China, has firmly established itself as the global nexus for rapid prototype turnaround and complex multi-layer PCB production. With fully integrated component markets, localized copper laminate suppliers, specialized chemistry providers, and advanced SMT packaging hubs clustered within a 50-kilometer radius in districts like Bao'an, engineering modifications that previously required weeks in Western facilities are routinely validated, routed, and fabricated within 48 to 72 hours.
Engineering Matrix: Material Dynamics & DFM Constraints
Comparative analysis of substrate performance, thermal conductivity, layer stackups, and physical process tolerances across advanced PCB design categories.
| Substrate Classification | Material Core Specs | Key DFM Physical Bottlenecks | Thermal & Frequency Metrics | IPC Class / Qualification Standard |
|---|---|---|---|---|
| High-TG FR-4 Multilayer | TG150, TG170, TG180, TG260, Shengyi, ITEQ, Isola | Aspect ratio > 10:1 barrel cracking, z-axis expansion control, desmear adequacy | Tg: 170-180°C, Td: 345°C, CTE z-axis: <3.5% | IPC-6012 Class 2 / Class 3, UL94V-0 |
| RF & Microwave Laminate | Rogers RO4350B, RO4003C, Taconic, PTFE blends | Microstrip line undercut, passive intermodulation (PIM), surface roughness loss | Dk: 3.48 ±0.05, Df: 0.0037 @ 10GHz | IPC-6018 Class 3 (Aerospace/Military) |
| Heavy Copper Substrate | FR-4 core with 3oz, 4oz, up to 10oz finished copper | Etch factor limits, resin starvation between heavy copper traces, solder voiding | Current carrying: >50A, High thermal sinking | IPC-2152 Standard for Copper Sizing |
| Metal Core (MCPCB) | Aluminum base 5052/6061, Copper base, Dielectric ceramic | Creepage distances between copper foil and baseplate, v-cut edge burring | Thermal conductivity: 1.0 to 8.0 W/m·K | IPC-4101E / Automotive AEC-Q200 |
| Rigid-Flex Interconnect | Polyimide (PI), Adhesive/Adhesiveless, FR-4 stiffeners | Bending radius stress points, transition zone air gaps, coverlay registration | Dynamic bend cycles: >100k, operating -40°C to +125°C | IPC-6013 Class 3 Type 4 |
| Ultra-High Density (HDI) | Laser-drilled microvias (stacked/staggered), 1+N+1 to 4+N+4 | Microvia plating voids, fine line etching (<50μm), pad cratering during reflow | Pitch: down to 0.35mm BGA, Line/Space: 2/2 mil | IPC-2226 High Density Architecture |
As the market accelerates toward sub-micron chip packaging and complex system-in-package (SiP) architectures, DFM methodology is moving from post-layout rules validation toward algorithmic generative layout synthesis. Design rules must now account for electrochemical migration (ECM), conductive anodic filament (CAF) risk paths along glass fiber weave bundles, and intermetallic compound (IMC) embrittlement at the solder interface caused by repeated lead-free thermal excursion cycles.
Mission-Critical Industry Application Scenarios
How targeted DFM adjustments resolve localized engineering challenges across defense, industrial automation, medical robotics, and energy infrastructure.
Aerospace & Anti-Drone Systems
Electronic countermeasure (ECM) platforms require continuous RF transmission across multiple frequency bands without phase distortion. Here, DFM mandates Rogers PTFE hybrid lamination, edge-plating ground shields, and controlled copper foil tooth profiles to reduce skin-effect losses and eliminate inter-band crosstalk in compact handheld jammers.
Industrial Drive Controllers & Inverters
Factory automation PLCs and variable-frequency drives (VFDs) operate under severe motor EMF kickback, vibration, and thermal loading. Our heavy copper DFM rules enforce dual-sided solder mask clearance, creepage isolation barriers adhering to IEC 60664-1, and mechanical mounting keep-outs to prevent trace shear under vibration.
Implantable & Wearable Health Tech
Medical diagnostic instrumentation and telemetry patches require ultra-miniaturized form factors without compromising signal-to-noise ratios. By deploying staggered microvia HDI stackups with rigid-flex designs, rigid board mass is minimized while eliminating wire harness interconnection failures.
Automotive BMS & EV Power Trains
Operating inside high-voltage lithium battery packs demands zero delamination risk across wide thermal operating bands (-40°C to +150°C). High-Tg laminates paired with aluminum baseplates transfer high heat away from MOSFET switching arrays, preventing local thermal runaway and preserving solder joint structural integrity.
Full Lifecycle Enterprise Supply Chain Integration
How our consolidated Shenzhen manufacturing center mitigates margin risk, eliminates component counterfeit vectors, and guarantees batch traceability.
Contracting separate entities for bare-board fabrication, components procurement, stencil tooling, and surface-mount assembly creates systemic operational vulnerabilities. When assembly defects such as solder bridging, non-wetting, or thermal stress delamination occur, fragmented suppliers often deflect responsibility between PCB fabrication flaws, component oxidation, or reflow oven thermal profiling errors.
MES Digital Traceability
Every bare PCB panel, component reel barcode, and SMT line parameter is registered in our centralized Manufacturing Execution System (MES). From solder paste thickness verified by 3D Solder Paste Inspection (SPI) to pre-reflow and post-reflow Automated Optical Inspection (AOI), complete data logs allow every board to be traced back to its raw material lots.
Authentic Component Sourcing
Operating directly within the Shenzhen electronics hub, our dedicated procurement engineers work directly with original manufacturers and authorized franchised distributors (including Texas Instruments, Analog Devices, STMicroelectronics, NXP, Murata, and TE Connectivity). Incoming materials undergo rigorous Incoming Quality Control (IQC) inspection, including X-ray fluorescence (XRF) testing, decapsulation, and pin-structure verification.
Box Build & Mechanical Integration
Beyond board-level SMT and through-hole soldering (DIP), we provide complete electro-mechanical box build integration. Services include custom CNC precision housing machining, injection plastic molding, conformal coating (acrylic, polyurethane, or silicone), MCU firmware programming, burn-in aging chambers, and direct-to-consumer or B2B export packaging.
Expanded PCB & Module Solutions
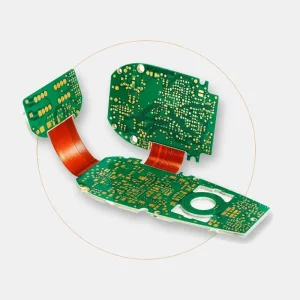
Explore additional specialized fabrication classes engineered for high-frequency signal processing, extreme-density interconnects, and flexible geometry requirements.


Frequently Asked Engineering & Procurement Questions
Essential technical insights covering DFM audit stages, stackup calculations, lead-free solder metallurgy, and prototype-to-volume transition parameters.
What specific technical checks are performed during a comprehensive DFM audit before production starts?
Our pre-production engineering DFM review evaluates more than 60 specific rules across fabrication and assembly domains. These include checking minimum trace widths and copper spacing against finished foil thickness weights; identifying potential acid traps caused by acute acute-angle trace geometry (<90°); calculating solder mask sliver retention thresholds to prevent solder bridge shorts; verifying via annular rings to eliminate teardrop breakouts; and comparing package land footprints to component body tolerances (IPC-7351B) to avoid component tombstoning during surface mount reflow.
Why is High-TG substrate material crucial for industrial, automotive, and defense PCB designs?
The Glass Transition Temperature (Tg) indicates the thermal boundary where the board's epoxy resin matrix transitions from a rigid, glass-like state to a flexible, rubbery structure. Standard FR-4 exhibits a Tg around 130°C to 140°C. In modern lead-free SAC305 wave and reflow soldering processes, peak oven temperatures reach 245°C to 260°C. High-TG materials (TG170, TG180, and higher) significantly curb Z-axis coefficient of thermal expansion (CTE), safeguarding through-hole plated vias against internal barrel fracture, corner cracking, and resin delamination under intense thermal cycling.
How does PCB ADEPT guarantee tight impedance control on high-frequency RF boards?
Precise impedance targeting (standard ±10%, precision tuned down to ±5%) begins with dielectric constant (Dk) stability. For high-speed applications exceeding 500MHz up to 77GHz millimeter-wave frequencies, we run pre-layout simulations in Polar SI9000 to determine precise line widths and ground reference planes. During wet-chemical etching, automated optical feedback adjusts conveyor travel speeds to compensate for copper etch factor undercuts. Every high-frequency production panel includes dedicated test coupons analyzed via Time-Domain Reflectometry (TDR) to certify exact performance before release.
What are the key manufacturing constraints when designing heavy copper printed circuit boards (≥3oz)?
Heavy copper circuit boards (ranging from 3oz up to 10oz) require specialized compensation factors. Because chemical spray etchants take longer to clear thick copper profiles, minimum spacing requirements increase proportionally to prevent lateral over-etching. Furthermore, during multilayer pressing, thicker copper configurations demand high-resin prepreg types (such as 1080 or 2116 with elevated resin content) to thoroughly encapsulate trace boundaries without generating micro-voids, resin starvation, or surface unevenness.
What engineering file formats are required to begin a turnkey PCB fabrication and assembly order?
To initiate our complete DFM and turnkey workflow, we require: (1) ODB++ data archives or Gerber RS-274X datasets complete with NC drill files; (2) A complete Bill of Materials (BOM) in Excel format denoting manufacturer part numbers (MPN), reference designators, package descriptions, and approved vendor list (AVL) alternates; (3) Pick-and-Place X-Y Centroid data files; and (4) Mechanical engineering drawings detailing cutouts, panel break-away tabs, V-score dimensions, and specialized testing/firmware flashing protocols.
What surface finish is best suited for fine-pitch BGA and surface mount packages?
While traditional HASL (Hot Air Solder Leveling) provides an economical finish, its surface profile is non-planar and inconsistent for fine-pitch BGAs (<0.5mm pitch) or 0201/01005 passives. Electroless Nickel Immersion Gold (ENIG) offers a flat surface, long shelf life, and excellent corrosion resistance. For mission-critical wire bonding or aerospace applications with high thermal demands, Electroless Nickel Electroless Palladium Immersion Gold (ENEPIG) eliminates "black pad" fracture vulnerabilities by introducing an intermediate palladium layer.
How do you identify and protect against counterfeit or refurbished electronic components?
Our IQC laboratory follows standard counterfeit-detection procedures. Incoming parts undergo microscopic visual inspection for signs of pin re-tinning, package sanding, or inconsistent laser markings. We also conduct solvent resistance testing to verify surface markings against chemical wipes, X-ray inspection to check internal lead frame alignment, and automated functional sample testing before components are kitted to the SMT placement floor.
What are the primary differences between IPC Class 2 and IPC Class 3 manufacturing standards?
IPC Class 2 governs standard commercial electronics, including consumer goods, appliances, and general computing hardware, where uninterrupted operational lifespan is preferred but not life-critical. IPC Class 3 specifies high-reliability electronics—such as aerospace navigation, automotive powertrain units, and implantable medical monitors—where downtime is impermissible. Class 3 dictates stricter requirements: zero allowable internal barrel plating voids in vias, higher minimum copper plating thickness (minimum 25μm inside hole walls), and tighter annular ring centering tolerances.