
Featured Small-Run PCB & Flex Solutions
Explore our high-performance board configurations engineered specifically for specialized prototypes, pilot batches, and mission-critical hardware iterations.

China Heavy Copper PCB Suppliers in China - High Current Capacity & Excellent Heat Dissipation from Reliable Factory Pricelist, Factory
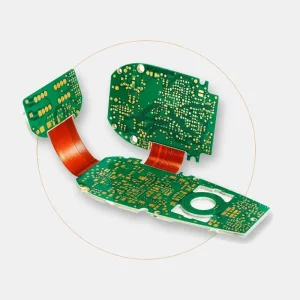
Buy China Rigid Flex PCB Suppliers - Single & Double-Sided, 4-16 Layer Multi-Layer Flex PCB Factory Supplier, Company
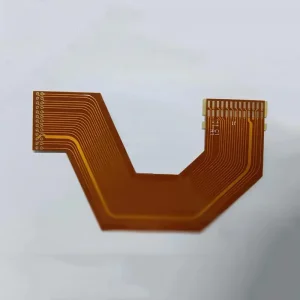
OEM High-Quality Flexible PCB from China Suppliers - Lightweight, Bendable and Foldable Solutions for Consumer Electronics Factory Quotes, Pricelist
OEM China Suppliers of Rigid Flex PCB, Double-Sided & Multi-Layer Flex Circuit Factory Company, Pricelist
OEM China Flexible PCB Suppliers - Bending, Folding, Lightweight Connections for Consumer Electronics Factory Manufacturers, Manufacturer
ODM China Suppliers Factory for Single and Double-Sided Rigid Flex PCBs, 4-16 Layer Complex Multi-Layer Solutions Pricelist, Factory
ODM China Rigid Flex PCB Suppliers - Single & Double-Sided, 4-16 Layer Complex Multi-Layer Factory Solutions Supplier, Company
High-Quality Flexible PCB Suppliers in China | Lightweight, Bendable, and Foldable Factory Solutions for Consumer Electronics Suppliers, Pricelist
The Paradigm Shift in Small-Run PCB Manufacturing
Why Low-Volume High-Mix (LVHM) fabrication has transformed from an experimental R&D afterthought into the critical competitive differentiator for global hardware development.
The Demise of "One-Size-Fits-All" Mass Tooling
Traditional PCB fabrication pipelines were architected for continuous mass-production runs exceeding hundreds of thousands of boards. In that legacy framework, high Non-Recurring Engineering (NRE) tooling charges, static panelization schemes, and prolonged photolithography setup cycles were amortized over massive volumes.
Today's electronics landscape, however, is governed by rapid agile sprints, iterative hardware development, accelerated product obsolescence, and hyper-targeted industrial deployments. When an engineering team requires between 5 and 500 pristine boards, committing to high setup investments with rigid Tier-1 mega-fabs introduces unacceptable fiscal drag and scheduling latency.
The Low-Volume High-Mix (LVHM) Imperative
Specialized sectors—ranging from aerospace guidance controllers and RF microwave communications to advanced medtech diagnostic sensors—do not operate on consumer-scale numbers. They operate on high complexity, varied stack-ups, tight trace impedances, and exotic substrates.
Modern high-quality small-run PCB manufacturing bridges this critical chasm. By implementing automated direct imaging (LDI), software-driven dynamic panel sharing, and quick-change surface-mount technology (SMT) feeders, high-tier facilities deliver production-grade IPC Class 3 reliability at prototype-level responsiveness.
De-risking the Commercialization Lifecycle
Procuring a low-volume run is fundamentally an insurance policy against systemic hardware failure. The cost of recalling or reworking 50,000 soldered boards due to uncontrolled thermal expansion or high-frequency dielectric loss can bankrupt a venture.
A rigorous small-run program allows cross-functional engineering teams to validate signal integrity, thermal dissipation vectors, solderability under active reflow profiles, and mechanical enclosures in authentic operational settings before allocating capital to full-scale rollouts.
Information Gain: Overcoming the "Prototype vs. Mass Production" Yield Gap
Many hardware developers discover that their functional prototype boards fail catastrophically once moved to high-volume assembly. This discrepancy is caused by low-end quick-turn prototype shops taking shortcuts: applying manual drill registration, non-controlled etch pools, and non-standard solder mask pigments that do not replicate commercial mass production tolerances. PCB ADEPT enforces uniform SMT reflow profiles, IPC-A-610 Class 3 optical inspections, and automated solder paste inspection (SPI) across every pilot run, ensuring zero variance when scaling.
Global Enterprise Sourcing & Quoting Dynamics
How international hardware buyers, engineering leads, and supply chain directors deconstruct PCB quotations, control hidden costs, and establish predictable delivery cadences.
Deconstructing the Small-Run PCB Cost Matrix
Procurement teams often face wide variances when evaluating small-run PCB quotations from international suppliers. Understanding the underlying pricing drivers allows engineering managers to optimize designs for cost efficiency without sacrificing signal integrity or thermal reliability:
- Substrate Selection & Dielectric Properties: Standard FR-4 (Tg 130–140°C) versus Mid/High-Tg laminates (Tg 170–180°C like Shengyi S1000-2M, Isola 370HR) or specialized PTFE/ceramic substrates (Rogers RO4350B, Taconic) represent significant cost differences.
- Layer Count & Lamination Cycles: Standard 2- to 8-layer rigid boards require a single press cycle. Rigid-flex or sequential build-up (HDI with 1+N+1 or 2+N+2 structures) require multi-step press lamination, increasing setup time.
- Copper Thickness & Etch Compensation: Standard 1oz copper runs smoothly through standard etching chambers. 3oz, 6oz, or 10oz heavy copper demands prolonged chemical milling and specialized resin filling.
- Surface Metallization Finishes: Lead-free HASL is cost-effective, whereas Electroless Nickel Immersion Gold (ENIG), ENEPIG, or Hard Electrolytic Gold (for edge connectors) require precious metals and tight chemical titration controls.
What Global Procurement Managers Require
Navigating cross-border manufacturing requires more than competitive board-level pricing. Tier-1 enterprise buyers prioritize comprehensive risk mitigation throughout the supplier evaluation lifecycle:
- Transparent NRE Disclosures: Clear itemization between photo-tooling, laser drill setup, electrical testing (flying probe vs. dedicated bed-of-nails fixture), and SMT laser-cut stencils.
- Complete Bill of Materials (BOM) Autonomy: Guaranteed direct sourcing from franchised distributors (Mouser, Digi-Key, Element14, Arrow) or verified original component manufacturers (TI, ADI, ST, Microchip, Murata).
- End-to-End MES Traceability: Complete lot tracking linking each physical board serial number to incoming copper laminate batches, solder paste inspection data, and reflow oven thermal records.
- Flexible Commercial Agility: Rapid credit options, non-disclosure agreements (NDAs) that preserve proprietary IP, and seamless handover to mass manufacturing.
Deep-Tier DFx: DFM, DFA, and DFT Engineering Execution
A rigorous Design for Excellence (DFx) review is the fundamental line of defense against costly functional respins, assembly bridges, and post-reflow signal degradation.
Design for Manufacturability (DFM)
DFM validates that board geometries can be reliably formed within physical chemical and mechanical tolerances:
- Aspect Ratio Verification: Mechanical hole aspect ratios are capped at 10:1 (or 0.8:1 for laser-ablated blind/buried micro-vias) to ensure copper plating within barrels.
- Annular Ring Integrity: Calculation of drill breakout risk under mechanical wander, guaranteeing an annular ring of ≥4.0 mil for Class 2, and ≥5.0 mil for Class 3.
- Copper Distribution Balancing: Thieving copper patterns in open signal spaces to prevent localized over-etching and board warpage.
- Solder Mask Dam Clearances: Maintaining minimum 3.0 to 4.0 mil mask webs between fine-pitch IC pins to eliminate solder bridges.
Design for Assembly (DFA)
DFA analyzes how components interact with pick-and-place nozzles, reflow profiles, and wave solder fountains:
- Component Shadowing Mitigation: Strategic placement of tall electrolytic capacitors away from small passive chips (0201/0402) to prevent uneven infrared/convection reflow.
- Thermal Relief Dynamics: Providing multi-spoke thermal isolation on ground plane pads so solder joints reach liquidus temperature without excessive heat sinking.
- Fiducial Placement: Inclusion of 1.0mm optical fiducial marks on panel corners and fine-pitch BGAs (<0.5mm pitch) for sub-micron vision alignment.
- Keep-Out Zone Adherence: Strict clearance enforcement between SMD pads and board v-score lines or rout paths to prevent ceramic capacitor cracking.
Design for Testability (DFT)
DFT incorporates test infrastructure into the layout to ensure electrical integrity without manual probing:
- Flying Probe Test Points: Locating dedicated circular test pads (≥28 mil diameter) on all critical power nets, reset lines, and clock paths.
- Boundary Scan (JTAG/SWD): Preserving clear, unhindered pin access for in-circuit micro-controller programming and scan testing.
- High-Voltage Isolation Routing: Ensuring creepage and clearance distances comply with IEC 61010-1 / UL 60950-1 for power converters.
- Automated Impedance Couplets: Incorporating test coupons on the panel border to verify single-ended (50Ω) and differential (90Ω, 100Ω) trace tolerances via TDR.
Small-Run Technical Capability Matrix
| Manufacturing Parameter | Standard Small-Run Capability | Advanced / Precision High-Density Capability |
|---|---|---|
| Layer Count Range | 1 – 16 Layers (Rigid FR-4) | Up to 60 Layers (Rigid), 1–6L (Flex), 4–22L (Rigid-Flex) |
| Minimum Trace Width / Space | 3.5 mil / 3.5 mil (0.089 mm) | 2.0 mil / 2.0 mil (0.050 mm) via Laser Direct Imaging |
| Minimum Mechanical Drill Size | 0.20 mm (8 mil) | 0.15 mm (6 mil) |
| Laser Micro-Via Drill Size | 0.10 mm (4 mil) | 0.075 mm (3 mil) via UV / CO2 Laser Drilling |
| Base Copper Cladding | 0.5 oz – 2.0 oz | 3.0 oz – 10.0 oz (Heavy Power Copper Systems) |
| Board Thickness Tolerance | ± 10% | ± 5% (Precision Pressing & Controlled Lamination) |
| Controlled Impedance Tolerance | ± 10% standard | ± 5% (Polar Instruments TDR Coupon Verified) |
| SMT Component Packaging | 0402, 0603, 0805, standard QFP/SOP | 01005 passives, 0.35mm pitch BGA, PoP, CSP, Micro-QFN |
| Automated Inspection Suite | 2D Optical Inspection, Flying Probe | 3D Solder Paste Inspection (SPI), 3D AOI, Offline X-Ray (AXI) |
Macro-Industry Application Blueprints
Engineered to satisfy demanding reliability constraints across specialized technology verticals.
Aerospace & Defense Systems
Flight management controllers, drone telemetry pods, and radar signal processors operating across extreme thermal cycling (-55°C to +125°C):
- High-Tg polyimide and hydrocarbon ceramic laminates.
- Immersion gold over nickel or ENEPIG metallization.
- IPC Class 3 manufacturing controls and X-ray analysis.
RF, Microwave & 5G Telecommunications
Phase-matched arrays, low-noise amplifiers, and millimeter-wave modules demanding low dielectric loss tangents (Df):
- Rogers 4000 series, Taconic, and PTFE/FR-4 hybrids.
- Smooth copper profiles for reduced skin-effect losses.
- Controlled dielectric spacing for matched lines.
Medical Diagnostics & Wearables
Portable patient telemetry, ultrasound transducers, and surgical devices requiring compact, flexible footprints:
- Ultra-thin polyimide rigid-flex constructions (1–6L flex).
- 01005 passives and high-density micro-BGA components.
- Biocompatible conformal coating and wash protocols.
Power Electronics & E-Mobility (xEV)
Traction inverters, battery management systems (BMS), and DC-DC converters carrying high sustained current:
- 3oz to 10oz heavy copper conductors for thermal loads.
- Aluminum and metal-core PCB (MCPCB) heat dissipation.
- High dielectric breakdown creepage isolation.
Shenzhen Manufacturing Hub & Global Compliance
Operating from Shenzhen's Bao'an electronics cluster, PCB ADEPT (Shenzhen ICSLOVE Technology Co., Ltd.) combines local supply chain agility with global quality governance.
8,000 m² Advanced Manufacturing Facility
Our Anda Electronic Industrial Zone plant integrates 6 high-speed YAMAHA SMT lines, 4 specialized through-hole DIP lines, nitrogen reflow ovens, and cleanroom environments. We maintain balanced capacity schedules, ensuring small-run prototype builds are never deprioritized behind high-volume mass production batches.
International Compliance Architecture
Manufacturing protocols are certified under ISO 9001:2015 quality management standards. Every bare PCB is fabricated to meet UL 94V-0 flammability ratings and complies with RoHS and REACH environmental directives. Assemblies are inspected and documented against IPC-A-600 (bare board) and IPC-A-610 Class 2 or Class 3 (assembly).
Supply Chain Cluster Proximity
Located in Shenzhen, our procurement personnel maintain direct, daily logistics with global component brand branches (Texas Instruments, Analog Devices, STMicroelectronics) and specialized material convertors. This eliminates multi-week shipping delays for obscure passives and exotic core laminates.
Step-by-Step Pilot Production Workflow
A systematic 4-phase manufacturing process engineered to deliver functional, tested PCB assemblies on schedule.
DFM Audit & Engineering Q&A
Within 24 hours of receiving your Gerber (RS-274X, ODB++), IPC-2581 files, and BOM, an assigned project engineer runs an automated 38-rule design rule check, identifying thermal traps, clearance hazards, or part obsolescence risks before tooling begins.
Tooling & Bare Board Fabrication
High-precision laser direct imaging (LDI), automated wet process chemical etching, CNC mechanical drilling, micro-via laser ablation, and vacuum press lamination are executed under continuous automated thickness and registration verification.
High-Speed SMT & DIP Assembly
Stencils with electro-polished apertures apply lead-free SAC305 paste, monitored via 3D SPI. High-speed YAMAHA placement systems position everything from 01005 passives to ultra-fine pitch BGAs prior to nitrogen reflow and wave soldering.
Testing, Box Build & Global Logistics
Boards undergo 100% automated optical inspection (AOI), first article inspection (FAI), flying probe testing, and custom functional testing (FCT). Assemblies are moisture-barrier vacuum-sealed and dispatched via express logistics (DHL/FedEx/UPS).
Technological Roadmap: 2026 to 2030
Anticipating the technological shifts reshaping low-volume electronics manufacturing over the next half-decade.
Sub-25μm Modified Semi-Additive Process (mSAP)
As next-generation System-in-Package (SiP) and edge-AI processor packages shrink ball pitches below 0.3mm, conventional subtractive chemical etching reaches its physical aspect ratio limits. PCB ADEPT is deploying mSAP copper build-up workflows in pilot production batches, allowing trace and space resolutions below 25μm with near-vertical sidewalls for higher signal routing density.
Deep Component Embedding in Thin Cores
Space-constrained medical implants and defense avionics increasingly require passive capacitors and thin-film resistors to be embedded directly within internal core laminates. This internal integration frees up surface area for active silicon, shortens parasitic loop inductances, and enhances EMI performance across multi-gigahertz operational bands.
Sustainable & Low-Carbon Eco-Laminates
Impending EU and North American ESG regulations mandate lower product carbon footprints. We are integrating PFAS-free copper clad laminates, bio-based resin systems, water-soluble flux chemistries, and low-temperature bismuth-tin (Bi-Sn) solder alloys that lower peak reflow temperatures from 245°C down to 170°C, reducing operational thermal stress on sensitive components.
Frequently Asked Questions
Comprehensive engineering and commercial answers to simplify your small-run PCB sourcing decisions.
What defines a "small-run" or low-volume PCB production order at PCB ADEPT?
What documentation and files are needed for an accurate small-run PCB and PCBA quote?
How does PCB ADEPT prevent counterfeit or substandard electronic components from entering the build?
Can you manufacture hybrid stack-up PCBs combining Rogers high-frequency material with standard FR-4?
What are the lead times for prototype turnarounds versus small batch turnkey assemblies?
Do you offer Box Build, custom enclosure integration, and firmware programming for pilot runs?
How do you handle Design for Manufacturability (DFM) discrepancies during engineering audits?
What surface finish is best suited for small-run PCBs featuring fine-pitch BGA or QFN packages?
High-Spec PCB Technologies for Rapid Production
Browse our advanced manufacturing solutions for high-frequency RF, high-current heavy copper, and complex multilayer prototypes.
Buy High Performance Heavy Copper PCBs from China Suppliers - Ideal for Power Converters & Vehicles with Superior Heat Dissipation Companies, Factories
ODM China Suppliers of High-Quality Rigid Flex PCB: Single, Double-Sided, and Multi-Layer Factory Solutions Manufacturer, Supplier

OEM High Frequency PCB Suppliers in China | Factory Solutions for Signal Loss, Crosstalk, and EMI Issues Suppliers, Factories
China Heavy Copper PCB for Power Converters - China Suppliers' Superior Factory Products for Enhanced Heat Dissipation and Current Capacity Supplier, Pricelist

Famous High TG PCB Suppliers in China - Durable Rogers PCBs for Automotive, Aerospace & Defense Industry Supplier, Factory
High-Quality China Rigid Flex PCB Suppliers | Single & Double-Sided, Multi-Layer Rigid Flex PCB Factory Manufacturers, Quotes
ODM Rapid PCB Prototyping and Validation by China Suppliers: Quality Factory Solutions for Modern Electronics Company, Quotes
