
Enterprise PCB Solutions: Engineering Validation to Production
Explore standard, heavy-copper, high-frequency, and HDI circuit boards manufactured to stringent IPC Class 2 and Class 3 specifications with instantaneous fabrication RFQ feedback.




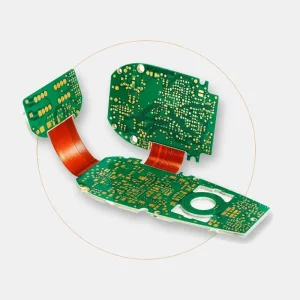

Deconstructing the PCB Fabrication Quote: Modern Determinants
In modern high-mix, low-to-mid volume manufacturing, quote calculation has transitioned from manual area-based formulas to cloud-driven DFM parsers that evaluate manufacturing risk, copper balance, and yield attrition.
Lamination & Dielectric Stack-up
Laminate choices heavily swing the quoting matrix. Beyond standard FR-4 (Tg 130-140°C), modern RF and automotive platforms mandate High-Tg (Tg > 170°C), halogen-free laminates, or specialized PTFE/ceramic substrates like Rogers 4350B and Taconic. The quotation reflects not just raw resin cost, but cycle press duration and specialized thermal curing profiles.
- Standard FR-4 vs. High-Tg vs. Polyimide flex cores
- Controlled prepreg dielectric thickness tolerances (±7-10%)
- Hybrid lamination combinations requiring dual-stage pressing
HDI Topography & Microvia Cycles
Quotes scale drastically when transitioning from standard mechanically drilled through-holes to High-Density Interconnect (HDI) structures. Laser Direct Imaging (LDI) and CO2 laser drilling for blind and buried microvias demand multiple press cycles (1+N+1, 2+N+2, Any-Layer HDI), with yield expectations mathematically factored into panel costs.
- Laser microvias down to 0.075mm (3 mil) diameter
- Copper via filling (VIPPO / IPC-4761 Type VII)
- Sequential electrochemical plating runs & planarization
Heavy Copper & Thermal Management
For industrial motor drives, EV powertrains, and solar converters, heavy copper fabrication (3oz to 10oz+) requires extended chemical etching baths and specialized solder mask deposition methods to prevent trace undercutting and void formation during wave or reflow soldering, directly influencing fabrication pricing.
- Etch-factor compensation for wide copper sidewalls
- Multi-pass differential solder mask printing
- Aluminum and copper-core metal-backed heat dissipation
Enterprise Sourcing Strategies: TCO vs. Sticker Price
Tier-1 automotive, telecommunications, and defense procurement executives no longer evaluate suppliers on bare board cost alone. The total cost of ownership (TCO) methodology integrates defect escapes, NPI iterations, and component obsolescence.
The Shift to Turnkey Procurement
Separating PCB fabrication from PCBA assembly introduces severe finger-pointing when component footprint solderability fails or warp-and-twist tolerances exceed SMT feeder parameters. Modern supply chain leaders aggregate bare-board fabrication, active BOM sourcing (Texas Instruments, STMicroelectronics, Analog Devices), and box-build assembly under a single accountable contract.
This integrated quoting protocol eliminates customs handover delays, eliminates airfreight legs between fab house and SMT line, and guarantees IPC-A-610 Class 3 assembly alignment from the very moment the bare panel is routed.
Supply Chain Resiliency & De-risking
Volatile geopolitical trade barriers and component end-of-life cycles mandate that famous PCB quotation suppliers offer robust BOM scrub capabilities. At Shenzhen ICSLOVE Technology (PCB ADEPT), every RFQ is run through parametric cross-referencing to flag at-risk ICs, extended lead times, or costly single-source components before fabrication begins.
Engineering teams receive drop-in pin-compatible alternatives that can cut bill-of-materials costs by 10% to 25% while shaving weeks off production milestones, turning the routine quotation phase into an active value-engineering consultation.
China Industry 4.0: Why Shenzhen Dominates Global PCB Supply
Located in the heart of the Guangdong-Hong Kong-Macao Greater Bay Area, the manufacturing hub of Shenzhen combines complete component supply proximity with cutting-edge smart automation.
MES-Driven Traceability
Every fabrication panel is barcoded at the inner-layer dry-film stage. As panels navigate chemical copper immersion, automated optical inspection (AOI), solder mask spray, and ENIG plating, lot parameters are tied to a central Manufacturing Execution System (MES), allowing full root-cause forensics down to individual circuit board coordinates.
Automated In-Line Inspection
High-speed YAMAHA SMT equipment operates in tandem with Solder Paste Inspection (SPI), pre-reflow automated optical inspection, and full 3D AOI post-reflow. Solder fillet heights, coplanarity, and void ratios under fine-pitch BGAs are quantified via inline X-ray systems (AXI), locking defects out of the final assembly stream.
Sub-Hour Proximity Ecosystem
Within a 30-kilometer radius in Bao'an and surrounding districts, raw copper-clad laminate suppliers (Shengyi, Kingboard), solder chemistry providers, stencil fabricators, and authorized component warehouses converge. This geographical hyper-density compresses production lead times from weeks down to 48 hours for rapid NPI verification.
Engineering Specifications & Fabrication Capability Windows
Comprehensive design-for-manufacturing (DFM) baseline specifications for engineering qualification.
| Parameter | Standard Capability | Advanced / High-Density Capability | Inspection & Verification Protocol |
|---|---|---|---|
| Layer Count Range | 1 – 16 Layers | Up to 60 Layers (Hybrid Stack-ups) | Microsection Analysis & Time Domain Reflectometry |
| Min. Line Width / Spacing | 3.5 mil / 3.5 mil (0.089mm) | 2.0 mil / 2.0 mil (0.050mm Any-Layer HDI) | Laser Direct Imaging (LDI) & Inline AOI |
| Min. Finished Hole Size | 0.20mm (Mechanically Drilled) | 0.075mm Laser Microvias (Blind / Buried) | Optical Hole Check & Cross-Section Void Exam |
| Finished Copper Thickness | 1oz – 3oz (35µm – 105µm) | Up to 10oz+ (Heavy Power Plane Routing) | XRF Copper Thickness Coating Gauge |
| Surface Finishes | HASL, Lead-free HASL, ENIG | ENEPIG, Immersion Silver/Tin, Hard Gold 50µ" | Solderability Testing & Gold Purity Titration |
| Quality & Cleanliness Standards | IPC-A-600 / IPC-A-610 Class 2 | IPC Class 3 / Aerospace / Automotive IATF | Ionic Contamination & High-Voltage Hi-Pot Test |
Localized Engineering Application Scenarios
Circuit boards manufactured by PCB ADEPT are engineered to withstand extreme thermal, electromagnetic, and vibrational duty cycles across critical vertical industries.
RF & Telecommunications
Millimeter-wave radar, satellite communication receivers, and 5G cellular infrastructure demand tightly controlled relative permittivity (Dk 2.2 to 3.5) and low dielectric loss tangent (Df < 0.002). Stack-ups integrate Rogers 4003C or PTFE hybrids with ENIG or ENEPIG finishes to mitigate skin effect losses at high gigahertz frequencies.
EV Power & Conversion
Onboard chargers (OBC), DC-DC power converters, and battery management systems (BMS) operate under massive current surges. Heavy-copper boards with up to 10oz inner and outer copper layers, backed by insulated metal substrates (IMS), ensure thermal dissipation without hot-spot delamination.
Industrial Edge AI & Robotics
Compact compute modules running multi-core SoCs, LPDDR5, and NVMe interfaces require micro-pitch BGA breakouts (<0.4mm ball pitch). By deploying 10-to-16 layer Any-Layer HDI with copper-filled vias, high trace density is achieved without signal degradation or crosstalk.
Aerospace & Defense
Unmanned aerial vehicles (UAVs), electronic warfare jamming systems, and tactical avionics require rigid-flex circuit architectures that absorb constant mechanical shock. Polyimide flex regions seamlessly transition into rigid multilayer sections, eliminating failure-prone wiring harnesses.
Frequently Asked Questions: PCB Fabrication Quotes
Comprehensive engineering clarifications addressing the key concerns raised by international hardware procurement leads, quality assurance directors, and NPI managers.
What primary documentation is required to generate an accurate turnkey PCB quotation?
An exact quotation requires Gerber RS-274X or ODB++ fabrication data, comprehensive layer stack-up drawings with defined core/prepreg thicknesses, a drill chart, and IPC netlist (.IPC-D-356). For turnkey assembly, please supply an engineering Bill of Materials (BOM) in Excel format with complete Manufacturer Part Numbers (MPN), reference designators, component descriptions, footprint packages, and an explicit approved manufacturer list (AML).
How does panelization and scrap factor affect the fabrication price per board?
Fabrication pricing directly depends on panel area utilization. Standard production panels are typically 18"x24" (457mm x 610mm) or 16"x21". Irregularly shaped, circular, or non-interlocking L-shaped designs that waste sheet area drive up square-inch costs. Working with our DFM team during the quoting phase allows you to optimize panel routing, scoring rails, and mouse-bite tabs to achieve >85% panel utilization, reducing overall unit prices.
When should an engineer specify ENEPIG over standard ENIG surface finish?
Standard ENIG (Electroless Nickel Immersion Gold) is excellent for flat surface SMT and fine-pitch components, but can experience "black pad" corrosion under improper chemistry control and is unsuitable for direct gold wire bonding. ENEPIG (Electroless Nickel Electroless Palladium Immersion Gold) incorporates an intermediate palladium barrier layer (0.05–0.15µm) that eliminates brittle nickel-tin intermetallic growth. Specify ENEPIG when wire bonding, ultra-fine BGA reliability, and harsh aerospace thermal cycling are required.
How are controlled impedance requirements verified and reported?
When controlled single-ended (e.g., 50Ω) or differential pair (e.g., 90Ω, 100Ω) lines are specified, test coupons are placed on production panel rails replicating the identical trace geometry and layer reference planes. Every production lot is verified via Time Domain Reflectometry (TDR) test instruments. Detailed impedance test reports, microsection photos, and dielectric layer measurements are included with the final outgoing Certificate of Conformance (CoC).
What is the typical lead time progression from quote acceptance to shipment?
For standard 2-to-8 layer quick-turn prototypes, bare board fabrication takes 24 to 72 hours. Advanced multilayer (10-24 layers), HDI, and rigid-flex prototypes typically require 5 to 9 business days. Turnkey PCBA lead times depend on active component procurement lead times, with standard kitted runs delivering in 3 to 9 days after incoming quality control (IQC) verification. Volume mass production generally operates on a 3-to-4 week release cycle.
How does PCB ADEPT guarantee against counterfeit electronic components?
All active and passive electronic components are sourced strictly through authorized direct distribution networks (such as Arrow, DigiKey, Mouser, Avnet) or original component manufacturers (OCM). Sourced components pass through rigorous incoming inspection, including microscopic package verification, pin oxidation analysis, laser marking verification, and random X-ray die inspection to prevent gray-market or counterfeit components from reaching the production floor.
Advanced Substrates, High-Tg & Industrial Volume Orders
Explore high-frequency, extreme temperature, and advanced thermal management boards ready for high-yield volume delivery.

