Buy Heavy Copper PCB Suppliers in China - High-Performance Factory for Power Converters & Efficient Heat Dissipation Company, Factories
Product Description
What is Heavy Copper PCB?
The core is used in high-current and high-power scenarios (such as power supplies, new energy, industrial control, etc.). The key points of its design, manufacturing and application are as follows:
Core Features and Application Scenarios
- Strong current-carrying capacity: The current-carrying capacity of 70μm copper foil (2 ounces) is approximately twice that of 35μm copper foil (1 ounce) (under the same line width).
- Good heat dissipation: The thick copper layer can quickly conduct heat, reducing the risk of overheating of the device.
- High mechanical strength: Thick copper enhances the PCB's resistance to bending and impact.
- Power converters (AC-DC/DC-DC), BMS for new energy vehicles, industrial frequency converters, control boards for welding machines, etc.
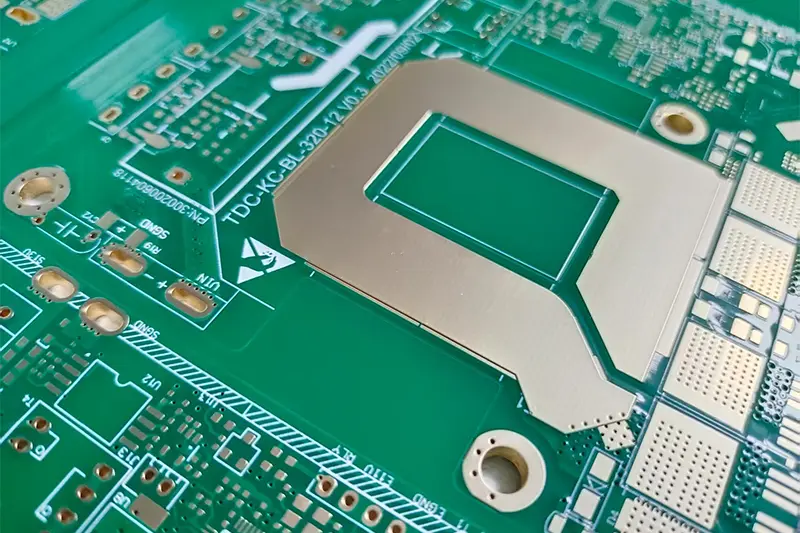
Key Design Points
Selection of Copper Foil Thickness
• Common specifications: 70μm (2 ounces), 105μm (3 ounces), 140μm (4 ounces), and up to 420μm (12 ounces) in extreme scenarios.
• Matching scenarios: For large current (≥5A) circuits, 2 to 4 ounces of copper should be preferred. For ultra-power scenarios (≥20A), 6 to 12 ounces of copper should be selected.
Trace & Current-Carrying Design
• Current-carrying capacity calculation based on copper thickness, line width, and temperature rise (usually designed based on a temperature rise of 10℃).
• Formula reference: I = K × W × T0.83 (I is the current, K is the coefficient, W is the line width, and T is the copper thickness). Example: 2 ounces of copper (70μm), wire width 5mm, current carrying capacity approximately 15A (temperature rise 10℃).
• Keep high-current traces as short and wide as possible to avoid narrow necks. Multi-layer boards can adopt parallel connection of multiple layers of copper foil.
Via and Pad Design
• Vias: For high-current vias, the hole diameter should be increased (≥0.5mm), the number of vias should be increased (estimated at 1A per hole), and the copper plating thickness on the hole wall should be ≥20μm.
• Pads: Thick copper pads need to be enlarged in size (0.2 to 0.5mm larger than ordinary pads) to prevent the copper layer from dissipating heat too quickly during welding, which may lead to false soldering.
Heat Dissipation & Insulation
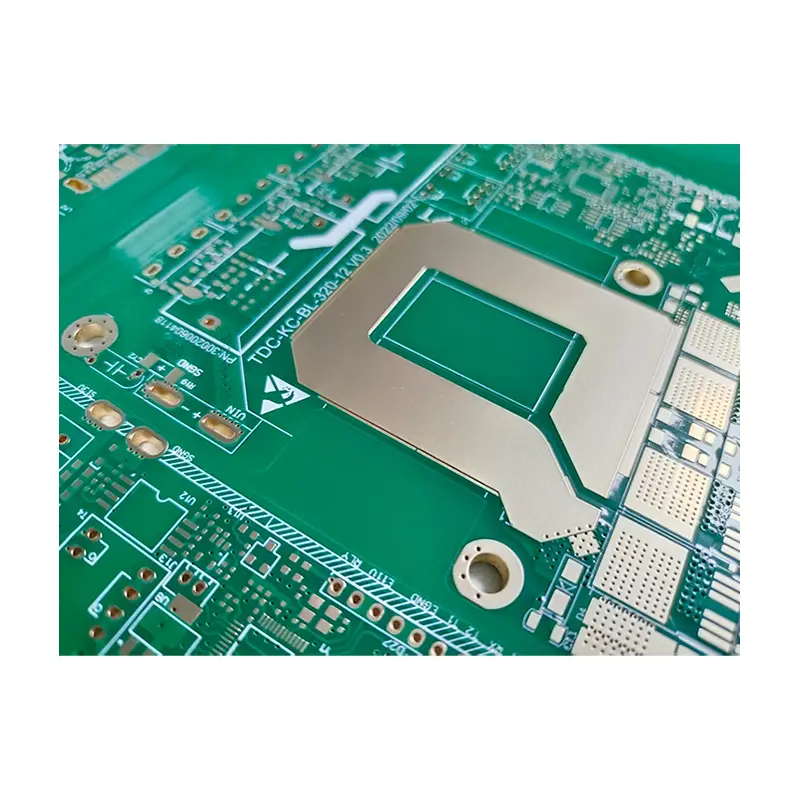
• Heat dissipation: The thick copper area can be designed as a "copper sheet heat sink", or a metallized via array (via spacing ≤1mm) can be added to connect to the heat dissipation layer.
• Insulation: The wire spacing for thick copper layers should be widened (for 70μm copper, the corresponding wire spacing should be ≥0.2mm) to prevent creepage breakdown under high voltage.
Manufacturing Process Difficulties and Control
Copper Foil Lamination and Etching
Thick copper lamination: High-temperature and high-pressure lamination (180℃/4MPa) is required to ensure the peel strength between the copper foil and the substrate (≥1.2N/mm).
Thick copper etching: The etching rate is slow (about 1μm/min), and the etching time needs to be controlled to avoid side etching (side etching amount ≤0.05mm). A stepwise etching process should be adopted to reduce line width deviation.
Lamination and Warpage Control
The coefficient of thermal expansion (CTE) of thick copper layers differs significantly from that of the substrate. When laminating, a "symmetrical structure" (with consistent copper thickness between the upper and lower layers) should be adopted, and a rigid support layer should be added to prevent PCB warping (warping degree ≤0.5%).
Surface Treatment
The surface of thick copper is prone to oxidation. It is preferred to choose tin plating (high-temperature tin layer) or nickel-gold plating to avoid OSP (incomplete organic film coverage). The pad area needs to be enlarged with a "solder mask opening window" to ensure the bonding force between the solder and thick copper.
Core Summary
The core of heavy copper PCBs is "high current carrying capacity + heat dissipation". In terms of design, it is necessary to match the copper thickness and current carrying capacity requirements. In manufacturing, problems such as thick copper etching and lamination warping need to be solved. They are suitable for high-power and high-current industrial and energy scenarios.
Frequently Asked Questions (FAQ)
What is the typical thickness range for heavy copper PCBs?
Heavy copper PCBs generally feature copper thicknesses starting from 70μm (2 ounces) up to 140μm (4 ounces). In extreme, high-power scenarios, the copper thickness can reach up to 420μm (12 ounces).
Why is heavy copper used instead of standard copper layers?
Heavy copper is selected for its superior current-carrying capacity, excellent heat dissipation performance, and enhanced mechanical strength, making it ideal for high-current and high-power applications.
How do you prevent false soldering on thick copper pads?
Because thick copper conducts heat very quickly, pads must be enlarged by 0.2 to 0.5mm compared to standard designs. This prevents the heat from dissipating too rapidly during assembly, ensuring strong solder joints.
What measures are taken to control board warpage during manufacturing?
Due to differences in thermal expansion coefficients between copper and the substrate, manufacturers use a symmetrical stack-up design (matching copper thickness on upper and lower layers) and add rigid support layers to keep board warpage below 0.5%.
Which surface treatments are recommended for heavy copper PCBs?
Tin plating (high-temperature tin layer) or nickel-gold plating are preferred. Standard OSP is generally avoided because the thick copper profile makes complete organic film coverage difficult to achieve, leaving the surface prone to oxidation.