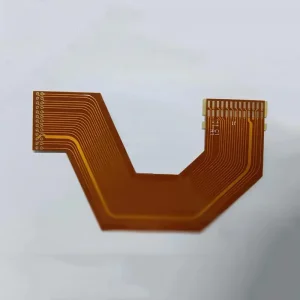
Advanced Flex & Multilayer PCB Solutions
Explore our core substrate solutions engineered to support complex flex SMT assemblies, high-density interconnect (HDI) micro-via layouts, and extreme RF microwave impedance matching.
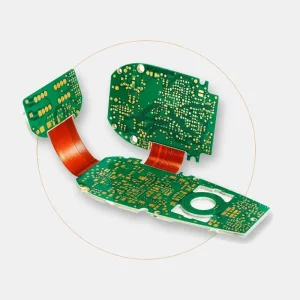



Macro Industry Solutions: Overcoming Dynamic Flex PCBA Challenges
Flexible Printed Circuit Board (FPC) surface-mount technology assembly demands a paradigm shift from rigid board processes. As mechanical envelopes contract across wearable medical diagnostic tools, aerospace avionics, and high-density automotive sensory systems, the integration of components directly onto polyimide membranes introduces severe thermo-mechanical stresses, hygroscopic expansion, and planar warpage that conventional EMS providers fail to manage.
Differential CTE Management
Polyimide base films possess a coefficient of thermal expansion (CTE) distinct from FR-4 stiffeners, copper foils, and lead-free SAC305 solder joints. Our engineering methodology utilizes graduated transitions, low-modulus acrylic or epoxy adhesive matrixes, and precision-compensated copper balancing to eliminate micro-cracking and solder fatigue across dynamic bend regions.
Dedicated Pallet & Vacuum Tooling
Because flexible foils cannot traverse high-speed SMT conveyor belts independently, we engineer magnetic, vacuum-assisted, or mechanical clamping fixture pallets. Synthetic stone (Durostone) carriers prevent flex flutter during pick-and-place, guaranteeing high coplanarity under YAMAHA mounters and eliminating stencil lift-off during paste printing.
Moisture De-Gassing Protocols
Polyimide is intrinsically hygroscopic, absorbing up to 3% atmospheric moisture by weight. Bypassing bake-out induces catastrophic delamination, solder blistering, and outgassing during 260°C lead-free reflow. We enforce an automated nitrogen-purged pre-bake cycle (110°C–120°C for 2–4 hours) within strict time-to-reflow windows monitored via our shop-floor MES.
Global EMS Dynamics & The Shenzhen Strategic Advantage
Global procurement teams operating in North America, Western Europe, and Asia-Pacific face tightening regulatory demands, microchip allocation volatility, and skyrocketing domestic NRE (Non-Recurring Engineering) overheads. Selecting a flex SMT assembly partner requires evaluating end-to-end component traceability, direct foundry ties, and comprehensive turnkey execution.
Component Ecosystem & Sourcing Authority
Shenzhen ICSLOVE Technology (PCB ADEPT) is strategically situated in Bao'an District, Shenzhen—the epicenter of global electronics hardware. Our procurement division maintains direct supply agreements with Tier-1 distributors for Texas Instruments, Analog Devices (ADI), STMicroelectronics, Microchip, Murata, and TE Connectivity (Tyco), securing genuine components, combating counterfeits via strict IQC inspection, and circumventing global logistics bottlenecks.
Unified Turnkey vs. Fragmented Sourcing
Procuring bare flex circuits from one vendor, loose ICs from brokerages, and outsourcing SMT placement to an onshore EMS creates fatal accountability gaps when yields drop. We integrate substrate fabrication (1–6 flex layers, 4–22 rigid-flex layers), component sourcing, SMT placement, THT DIP soldering, conformal coating, and enclosure assembly under a singular, transparent ISO 9001 quality framework.
Total Cost of Ownership (TCO) Optimization
Through proactive Design for Manufacturing (DFM) and Design for Assembly (DFA) audits, we eliminate unneeded flex lamination stages, swap hard-to-source passives with pin-compatible automotive-grade drop-ins, and streamline stiffener layouts (combining FR-4, stainless steel, and polyimide). This typically drives a 10%+ bill-of-materials cost-down while reducing engineering cycle times by weeks.
Industrial Governance, Quality Standards & Traceability
Reliability in mission-critical applications is not accidental. PCB ADEPT operates under rigorous international quality certifications, embedding continuous multi-stage inspection data into our Manufacturing Execution System (MES) for end-to-end component-to-board traceability.
IPC-A-610 Class 2 & 3
Assemblies are manufactured and verified against IPC-A-610 (Acceptability of Electronic Assemblies) and IPC-6013 (Qualification and Performance Specification for Flexible Printed Boards), maintaining solder joint integrity and fillet profiles under dynamic vibration.
In-Line 3D SPI & 3D AOI
Every flex board undergoes 3D Solder Paste Inspection (SPI) to detect height, volume, and bridge defects before component placement. Post-reflow 3D Automated Optical Inspection scans for tombstoning, pad skew, and solder voiding.
X-Ray & First Article Inspection
High-resolution oblique-angle X-ray inspection evaluates hidden solder joints under ultra-dense Ball Grid Arrays (BGAs), Chip-Scale Packaging (CSPs), and QFN thermal ground pads, validating zero bridging and minimal voiding (<10%).
RoHS, REACH & UL 94V-0
All substrate polyimide films, coverlays, pressure-sensitive adhesives, solder pastes, and fluxes adhere completely to EU RoHS/REACH environmental mandates. Materials satisfy UL 94V-0 flammability classifications for consumer and defense safety.
Flex PCB SMT Manufacturing Capability Matrix
Review standard and advanced tolerance specifications for flex and rigid-flex assembly at our Shenzhen manufacturing center.
| Process Parameter | Standard Flex Capability | Advanced / High-Density Capability | Quality & Test Verification |
|---|---|---|---|
| Layer Count Range | 1 – 4 Layers (Pure Flex) | 5 – 6 Flex / 4 – 22 Rigid-Flex Layers | Micro-sectioning & IPC-6013 Cross-Section |
| Base Core Substrate | 12.5µm – 25µm Polyimide (Kapton) | Adhesiveless Polyimide / Low-Loss PTFE | Dielectric breakdown & Peel Strength Test |
| SMT Pitch & Passives | 0402, 0201 passives, 0.5mm IC pitch | 01005 passives, 0.3mm BGA / CSP pitch | In-line 3D SPI, YAMAHA Multi-Vision Placement |
| Stiffener Variations | FR-4 (0.2–1.5mm), Polyimide backing | SUS303/304 Stainless, Aluminum, Ceramic | Optical CMM Alignment, Bond Shear Testing |
| Surface Finish Options | Immersion Gold (ENIG 1–3 µin) | Hard Gold (30-50 µin), ENEPIG, Immersion Silver | XRF Surface Plating Thickness Analyzer |
| Solder Reflow Atmosphere | Standard Convection Reflow | 10-Zone Nitrogen (N2) Reflow Tunnel | KIC Profiler thermal gradient logging per lot |
| Testing Protocols | Flying Probe, ICT, Open/Short E-Test | FCT Custom Jigs, Micro-BGA X-Ray, Aging Chamber | 100% Traceable MES Serialized Data Logging |
High-Reliability Industrial Application Scenarios
Flexible circuit SMT assemblies replace heavy wiring harnesses, reduce inter-board connectors, and fit inside non-planar enclosures across demanding technological sectors.
Medical Diagnostic & Wearables
Biocompatible flex substrates supporting high-density pulse oximeters, digital endoscopic camera links, ultrasonic transducer arrays, and continuous glucose monitoring patches where sub-millimeter flexibility and non-toxic polyimide are mandatory.
Aerospace & Defense Systems
Deployments across gimbaled thermal camera heads, satellite radar payloads, guidance computers, and anti-drone electronic jamming systems. Rigid-flex multilayer configurations absorb high g-forces and extreme thermal shock (-55°C to +125°C).
Automotive ADAS & BMS
Electric vehicle (EV) battery management systems (BMS) integrate continuous flexible circuit strips to monitor battery cell voltage and temperature in real time, substituting thick cable assemblies while resisting harsh under-the-hood engine vibrations.
Foldable IoT & Robotics
High-flex dynamic joints in multi-axis robotic arms, hinge interconnects in dual-display handhelds, and miniaturized optical transceiver modules utilizing controlled impedance traces up to 10 GHz with minimal signal attenuation.
Flex PCBA Roadmap: Next-Generation Innovations
As electronic systems migrate toward AI edge acceleration and ultra-compact packages, flexible circuit assembly is rapidly adopting advanced micro-fabrication paradigms.
Modified Semi-Additive Processing (mSAP)
Moving beyond subtractive copper etching, our advanced R&D lines are implementing mSAP on adhesiveless polyimide films, enabling ultra-fine line trace widths and spacings down to 25µm/25µm. This supports direct flip-chip bonding and wafer-level packaging onto flex circuits without intermediate interposers.
Embedded Passives & Thin-Film Dies
By embedding planar resistors, capacitors, and thinned bare silicon dies directly within intermediate polyimide core layers, flex assemblies free up external surface area for ultra-dense sensor layouts, while simultaneously shortening high-speed signal transit paths.
Laser Direct Structuring & Additive Dispensing
Integrating UV picosecond laser cutting and micro-additive conductive ink printing allows rapid modification of sensor footprints on 3D contoured flex surfaces, eliminating hard tooling cycles for medical and aerospace validation batches.
Frequently Asked Questions on Flex PCB SMT Assembly
Clear, unvarnished engineering answers covering DFM feasibility, assembly tooling, baking cycles, and cost considerations for overseas buyers.
Why is a pre-reflow baking cycle mandatory for flex PCB SMT assembly?
Polyimide base films naturally absorb moisture from atmospheric humidity. Exposing an unbaked flex board to the 240°C–260°C temperatures of lead-free reflow causes trapped water molecules to rapidly vaporize into steam. This pressure expansion creates micro-voids, internal delamination between copper and coverlay, and solder joint fractures. We enforce an automated nitrogen pre-bake at 110°C–120°C for 2–4 hours followed by dry-box storage.
How do you maintain planarity during pick-and-place and reflow soldering?
Because flex circuits lack intrinsic structural rigidity, placing tiny 01005 passives or fine-pitch BGAs directly onto an unconstrained sheet causes placement offsets and solder bridging. We fabricate dedicated CNC synthetic stone pallets (Durostone or aluminum) equipped with precision tooling pins and high-temperature silicone or mechanical clamps. For high-density micro-vias, vacuum-assisted carrier pallets hold the substrate flat throughout solder printing and placement.
What files are required to initiate a turnkey flex PCBA quote?
To deliver an exhaustive DFM review and quotation within 24 hours, our engineering team requires: (1) Gerber RS-274X or ODB++ files showing copper layers, coverlay openings, stiffener boundaries, and silk screens; (2) A Bill of Materials (BOM) in Excel with exact manufacturer part numbers (MPNs), reference designators, and approved alternative components; (3) Pick-and-Place (centroid) XY coordinate file; and (4) Fabrication drawings detailing stiffener materials, thickness, and peel tests.
How do FR-4 and Stainless Steel stiffeners affect SMT placement?
Stiffeners provide localized mechanical rigidity underneath heavy components, connectors, and fine-pitch ICs to prevent mechanical strain from transferring to delicate solder joints during flexing. FR-4 stiffeners are typically bonded under SMT zones using thermosetting adhesive film. For ultra-thin enclosures requiring grounded shielding or extreme flatness, 0.1mm–0.3mm SUS303 stainless steel or aluminum stiffeners are applied with conductive pressure-sensitive adhesive.
Can you assemble BGA packages on flexible PCB substrates reliably?
Yes. Assembling BGAs on flex substrates requires placing a solid stiffener directly underneath the BGA footprint on the reverse side of the board. This prevents the polyimide from warping under thermal reflow cycles. Additionally, our SMT lines use electroformed nickel or stepped stencils to achieve precise solder paste volume, followed by multi-angle 3D AOI and micro-focus oblique X-ray inspection to confirm ball coplanarity and check for solder bridging.
What is the typical lead time for flex SMT prototype versus volume lots?
For engineering prototypes and quickturn validation batches (1 to 500 pcs), our typical turnaround ranges from 3 to 9 business days, provided component procurement is expedited. Production volume runs (1,000 to 100,000+ units) typically ship in 2 to 3 weeks depending on raw material sourcing (such as specialized DuPont Pyralux or Rogers high-frequency substrates) and customized functional test fixture preparation.
Comprehensive Electronic Manufacturing Solutions
From flexible circuits and heavy copper power converters to IoT compute modules and multi-layer rigid-flex boards, explore our verified manufacturing catalog.