
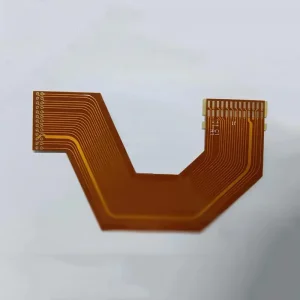
Flex Solutions
Accelerate deployment from 24-hour rapid prototyping to full-volume fabrication. Tested to IPC Class 2/3 and ISO 9001 quality specifications.




In modern hardware engineering, electronic velocity defines market leadership. As product lifecycles compress across automotive, avionics, defense, and edge computing, quick-turn circuit board fabrication has transformed from an ad-hoc prototyping convenience into a foundational pillar of enterprise New Product Introduction (NPI).
Traditional prototype cycles spanning 3 to 5 weeks paralyze firmware verification and mechanical validation. ODM fast-turn models compress bare-board manufacturing to 24 to 48 hours and turnkey PCBA prototypes to 3 to 9 days.
The global printed circuit board market is projected to surpass $90 billion, driven primarily by multi-layer RF, HDI, and rigid-flex configurations. North American and European OEMs increasingly depend on specialized Asian hubs to absorb initial iteration friction.
Speed without rigorous quality verification results in costly recall loops. Fast-turn ODM excellence integrates inline real-time automated optical inspection (AOI), solder paste inspection (SPI), and cross-sectional micro-section analysis directly into the rapid-flow lines.
Shenzhen’s Bao’an District and the broader Pearl River Delta represent the most concentrated, technologically complete electronics ecosystem on earth. When an ODM project encounters a rare dielectric laminate shortage or a specialty connector revision, resolution is measured in hours, not weeks.
Within a 30-minute radius of the manufacturing facility sit world-class laminate manufacturers (Shengyi, Kingboard), precision chemical formulators, copper foil suppliers, and authorized electronic component distributor networks. This geographic concentration completely eliminates shipping delays for specialized laminates such as Rogers RO4350B, Taconic, or Panasonic Megtron 6.
If an engineering revision requires an alternate resistor network or micro-controller from Texas Instruments, STMicroelectronics, or Murata, localized inventory pools allow same-day delivery to the SMT placement feeder lines.
Our 8,000 m² facility features dual-track Yamaha high-speed SMT placement systems, 10-zone reflow ovens, and an integrated Manufacturing Execution System (MES). The MES tracks every lot from incoming raw material check (IQC) through automated solder paste inspection (SPI), pre-reflow optical inspection, and post-reflow 3D AOI.
Barcoded traveler cards allow engineering teams in the USA, Germany, or Japan to trace exact reflow thermal profiles, lot numbers, and inspector IDs for their custom electronics builds.
Gerber, ODB++, and BOM files analyzed for trace clearance, copper balance, annular rings, and solder dam integrity to prevent fabrication holds.
Inner layer dry film photo-imaging via Laser Direct Imaging without mechanical photo tools, followed by multi-opening vacuum hot pressing.
Mechanical precision micro-drilling, UV laser drilling for blind vias, automated vertical continuous plating (VCP), and pulse electroplating.
Application of ENIG, Immersion Silver, or ENEPIG followed by flying probe netlist testing, impedance TDR certification, and vacuum packaging.
Hardware design teams must align layout rules with factory capabilities. Below is an exhaustive summary of parameters for standard rigid, multi-layer, high-frequency, and HDI flex-rigid configurations.
| Fabrication Parameter | Standard Prototype Capability | Advanced ODM Fast-Turn Limit | Quality Standards & Controls |
|---|---|---|---|
| Layer Count Range | 1 – 16 Layers (Rigid FR-4) | Up to 60 Layers (Hybrid / High-Density) | IPC-6012 Class 2 / Class 3 |
| Min. Trace Width / Spacing | 3.5 mil / 3.5 mil (0.089 mm) | 2.5 mil / 2.5 mil (0.063 mm) | Laser Direct Imaging (LDI) Verified |
| Min. Mechanical Drill Size | 0.20 mm (8 mil) | 0.15 mm (6 mil) | Automated CNC Optical Target Locating |
| Laser Microvia Diameter | 0.10 mm (4 mil) | 0.075 mm (3 mil) | CO2 / UV Laser Drilling for HDI 1-3+N-3 |
| Controlled Impedance Tolerance | ± 10% Standard | ± 5% Tight Differential Pair | Polar SI9000 & TDR Test Coupon Report |
| Finished Board Thickness | 0.4 mm – 3.2 mm | 0.2 mm – 6.0 mm | Micrometer & Cross-Sectional Analysis |
| Copper Weight (Finished) | 1 oz, 2 oz | 3 oz – 10 oz (Heavy Power Busboards) | X-Ray Fluorescence (XRF) Gauging |
| Surface Metallurgy | Lead-Free HASL, ENIG (Electroless Ni/Au) | ENEPIG, Immersion Silver, Hard Gold Plating | Solderability Testing & RoHS Compliance |
| Substrate Core Types | Standard Tg140, High Tg170+ FR-4 | Rogers, Taconic, Polyimide, Aluminum Core | IPC-4101 Base Material Validation |
Every industrial sector has unique environmental, thermal, and signal integrity constraints. Our factory lines adapt process windows to serve targeted mission-critical use cases.
Battery Management Systems (BMS), DC-DC converters, and motor inverters requiring thick 3oz to 6oz copper boards, heavy copper heat dissipation, and AEC-Q200 component qualifications.
Precision RF amplification, low-loss microwave dielectric cores, Rogers/FR-4 hybrid stackups, and hard gold fingers engineered for high heat flux and clean signal transmission up to 40 GHz.
Carrier boards and daughter cards for Raspberry Pi compute modules, NVIDIA Jetson platforms, and robotics motherboards requiring blind microvia HDI and fine-pitch 0.4mm BGA routing.
Portable patient monitors, diagnostic scanners, and wearable vital trackers using high-density flexible PCBs and rigid-flex boards designed for extreme flexural endurance and strict cleanroom assembly.
Rugged long-lifespan industrial controllers, LoRa/NB-IoT smart metering hubs, and remote sensors built on high-Tg substrates resistant to thermal shock, high humidity, and vibration.
Metal core PCB (MCPCB) configurations utilizing insulated aluminum and copper substrates with thermal conductivities up to 3.0 W/m·K for commercial LED luminaires and industrial power switches.
Multi-cavity filter boards, high-speed backplanes, and low-passive intermodulation (PIM) antenna modules designed with PTFE and ultra-smooth electrodeposited copper foils.
High-reliability military-grade circuit assemblies featuring conformal coating, selective underfill, automated X-ray inspection (AXI) of concealed solder joints, and tamper-resistant layouts.
Procurement officers and VP-level engineering managers face tight delivery schedules, volatile component spot markets, and stringent regulatory demands. Below are strategic principles for seamless fast-turn execution.
Prior to submitting manufacturing data, eliminate Single-Source components and components flagged as End-of-Life (EOL) or Not Recommended for New Designs (NRND). Our engineering team performs BOM scrubs to suggest pin-compatible alternates with verified factory stock.
Every engineering hold adds 24 hours of latency. By standardizing on clear stack-up documents, defining explicit impedance trace callouts, and providing centroid (pick-and-place) files aligned with CAD origins, offshore orders release directly to factory CAM lines within two hours.
Separating bare-board fabrication, component brokers, and SMT assembly leads to finger-pointing when yield issues arise. Contracting with a single turnkey partner establishes clear, single-source accountability across bare board lamination, solder paste chemistry, and reflow integrity.
As semiconductor process nodes shrink to 3nm and high-power computing packages proliferate, printed circuit board fabrication is evolving toward semiconductor substrate packaging paradigms.
Modified Semi-Additive Processes (mSAP) allow trace lines and spaces below 25µm / 25µm, bridging the gap between conventional PCB subtractive etching and silicon interposers for next-generation edge devices.
Embedding passive capacitors and active silicon dies directly into inner substrate prepregs frees top/bottom layer area, minimizes parasitic inductance, and enhances thermal management in ultra-compact designs.
Driven by ESG mandates and carbon footprint reporting, the industry is transitioning to halogen-free, recyclable resins and ultra-low Dk/Df hydrocarbon laminates designed for 6G sub-terahertz signal paths.
Detailed technical answers to common questions asked by senior hardware developers, procurement leads, and quality audit directors.
Achieving true 24-hour delivery on 2 to 6-layer designs requires removing manual intervention points across tooling. Our factory uses Direct CAM scripting for rapid DFM checks, Laser Direct Imaging (LDI) to bypass silver phototool generation, automated pinless vacuum lamination presses, and high-speed multi-spindle CNC drilling machines. High-Tg FR-4 copper-clad sheets are pre-conditioned and maintained in constant inventory, enabling bare boards to move directly into etching, solder mask curing, and surface finishing in a single continuous production cycle.
Standard manufacturing yields a ±10% controlled impedance tolerance across single-ended microstrips and differential pairs. For mission-critical RF, radar, and PCIe 5.0/6.0 lines, we utilize advanced automated optical inspection during etching and run Polar Instruments SI9000 modeling to hold a ±5% tolerance. Every production panel includes dedicated test coupons analyzed via Time-Domain Reflectometry (TDR), with serialized test reports included in customer quality documentation.
To ensure zero engineering holds, provide: (1) Complete Gerber files in RS-274X format or ODB++ directory; (2) An unambiguous fabrication drawing detailing copper weight, target board thickness, solder mask color, IPC class requirement, and surface finish (e.g., ENIG 2µ'' gold over 120µ'' nickel); (3) For PCBA, a comprehensive Bill of Materials (BOM) in Excel format with explicit Manufacturer Part Numbers (MPN), approved second-source equivalents, reference designators, and package footprints; and (4) An XY Centroid (Pick-and-Place) file referenced to the board origin.
While Electroless Nickel Immersion Gold (ENIG) offers reliable surface coplanarity for fine-pitch SMT, it can be vulnerable to "black pad" syndrome if phosphorus levels deviate during chemical nickel deposition. Electroless Nickel Electroless Palladium Immersion Gold (ENEPIG) introduces an intermediate palladium layer between the nickel and outer gold immersion. This completely eliminates black pad defect risks, improves thermal aging endurance, provides reliable solder joint reliability with SAC305 alloys, and supports both gold and aluminum wire bonding for aerospace, defense, and chip-on-board (COB) applications.
We apply a multi-tier Incoming Quality Control (IQC) protocol. All active ICs, passive arrays, and power modules are sourced directly from original manufacturers or authorized global franchised distributors (e.g., Digi-Key, Mouser, Arrow, Avnet) and verified Chinese franchise agents. Parts entering the facility undergo packaging seal checks, lot code traceability audits, optical digital microscopy, pin oxidation checks, and, where necessary, acetone marking permanence tests and internal X-ray lead-frame die inspection.
Yes. Hybrid construction is an effective way to balance performance and cost. For example, routing 24 GHz to 77 GHz RF signals on an outer layer of Rogers RO4350B or RO4003C while building the lower digital routing and power planes with standard high-Tg FR-4 helps manage overall material costs. Our engineering team reviews the thermal expansion coefficients (CTE) and prepreg resin flow characteristics during lamination to prevent inner-layer delamination or excessive board bow and twist.
Every assembly order passes through: (1) Solder Paste Inspection (SPI) to measure 3D volume, height, and alignment; (2) Post-reflow 3D Automated Optical Inspection (AOI) to detect bridging, tombstones, solder voids, and polarity deviations; (3) First Article Inspection (FAI) using automated LCR fixtures; (4) Automated X-Ray Inspection (AXI) for hidden BGA, QFN, and bottom-terminated components; (5) In-Circuit Testing (ICT) or Flying Probe testing for circuit continuity; and (6) Optional functional testing (FCT) and environmental burn-in/aging based on customer-supplied test specifications.
There is no minimum order quantity—we build quick-turn prototypes from a single piece up to 500 units for engineering validation. Once pilot runs and field testing are approved, your project transitions seamlessly to our high-volume production lines within the same corporate group. This keeps tooling, test fixtures, SMT pick-and-place profiles, and reflow recipes consistent, avoiding the yield fallout that often occurs when changing factories.
From heavy copper heat sinks to high-frequency Rogers communication boards and Raspberry Pi industrial expansion shields.

