OEM Flexible PCB from China Suppliers: Lightweight, Thin, and Bendable Solutions for Consumer Electronics Factory Manufacturer, Factory
Product Description
The main functions are reflected in
It can be bent and folded inside the device, greatly enhancing space utilization and design freedom.
Its thin and light characteristics are the key for smartphones and wearable devices to achieve lightness and portability.
Reduce connectors and solder joints to be more durable in vibrating and bending environments.
Far-reaching impact
It has directly given rise to innovative product forms such as foldable screen mobile phones and wearable devices, and has become an indispensable cornerstone for the high-end development of fields such as automotive electronics, medical equipment, and aerospace. Flexible PCBs have profoundly transformed the design concepts and industrial landscape of electronic products by endowing them with "flexibility" and "deformability" capabilities.
What is Flexible PCB(FPC)
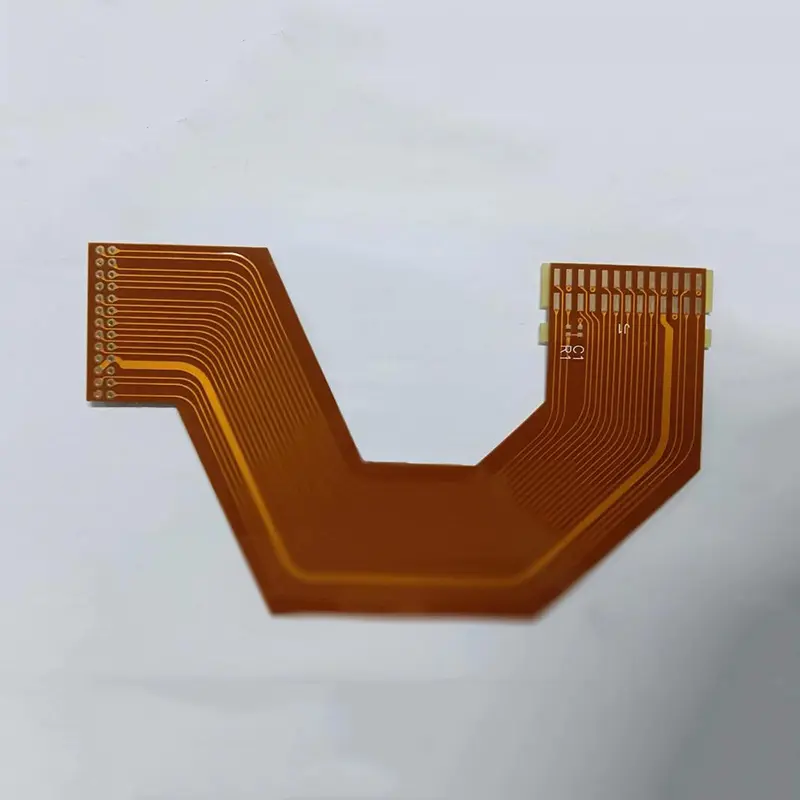
Flexible PCB, whose full name is flexible printed circuit board, is commonly known as "soft board". You can imagine it as a kind of "flexible electronic circuit" or "circuit cloth". It is a "relative" of the common green, hard computer motherboard (rigid PCB) we often see, but the core material is completely different.
Core features (What is it)
The material is soft: Its substrate is not hard glass fiber but a flexible plastic film such as polyimide, which is heat-resistant and can be repeatedly bent.
Bendable and foldable: This is its most prominent feature. It can be bent, wound and folded in three dimensions to adapt to various narrow or irregular Spaces.
Thin and light: Much thinner and lighter than rigid PCBs.
Main uses (what to do with it)
Because it can bend and stretch, it is used in all places that require space saving, movement or lightness and thinness:
Smartphones/foldable phones: The most classic applications. The "flat cables" that connect the screen, camera, buttons and battery in a mobile phone are mostly flexible PCBs. The hinge part of a foldable phone requires a high-end flexible PCB that can withstand hundreds of thousands of bends.
Wearable devices: Such as smartwatches, bracelets and health patches, need to fit the curves of the human body.
Notebook computer: The "link" connecting the motherboard and the screen.
Automotive electronics: LED headlights, central control screens, various sensors, complex wiring harnesses and compact space.
Precision medical equipment: Such as endoscope capsules and pacemakers, has extremely high requirements for space and reliability.
Aerospace: The "sinews and bones" for satellites and aircraft, capable of reducing weight and adapting to complex cabin layouts.
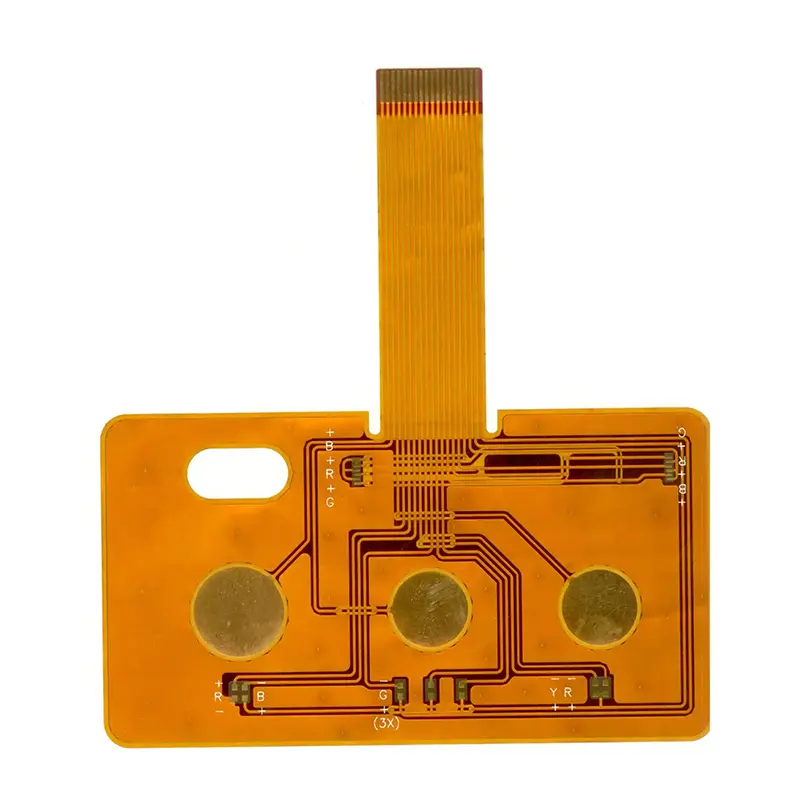
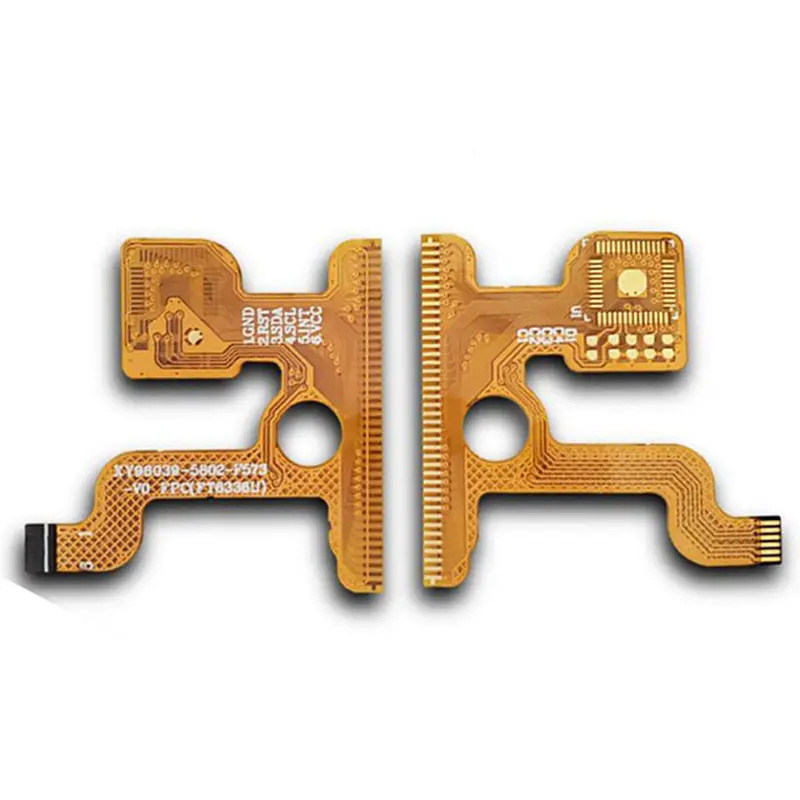
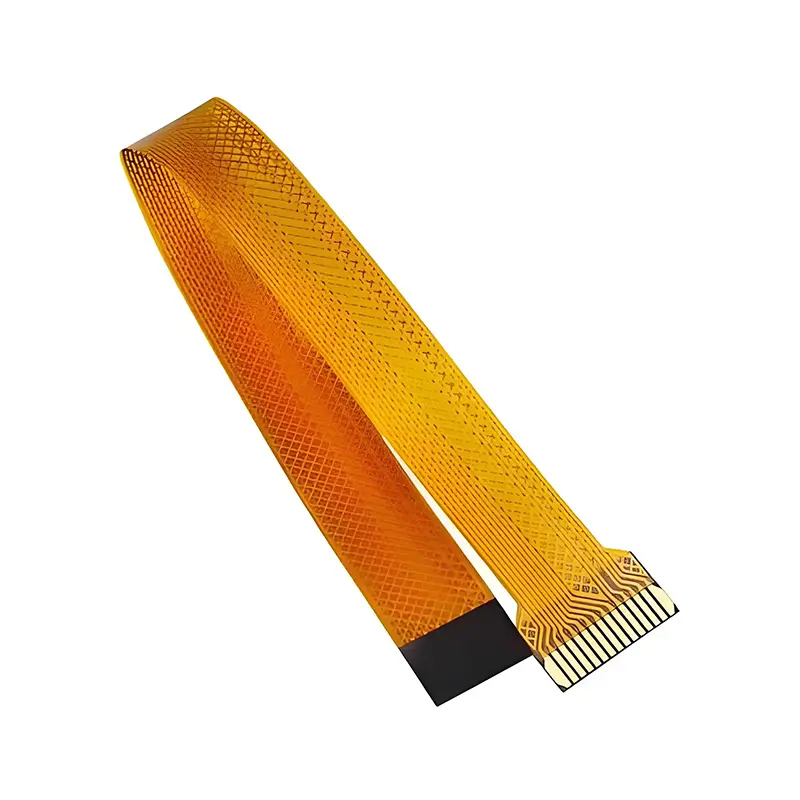
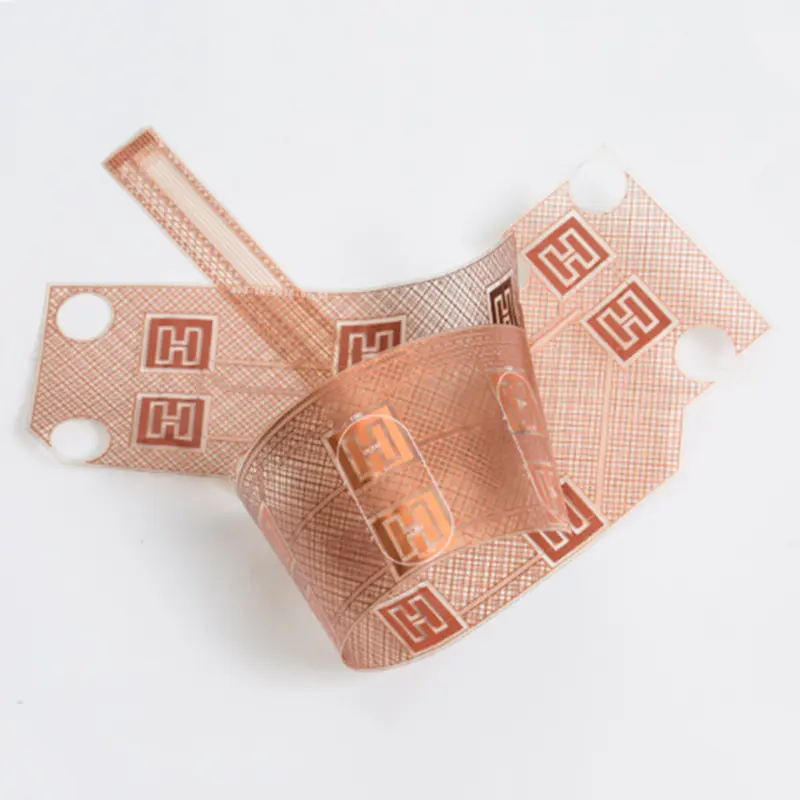
Normal type of flexible PCB:
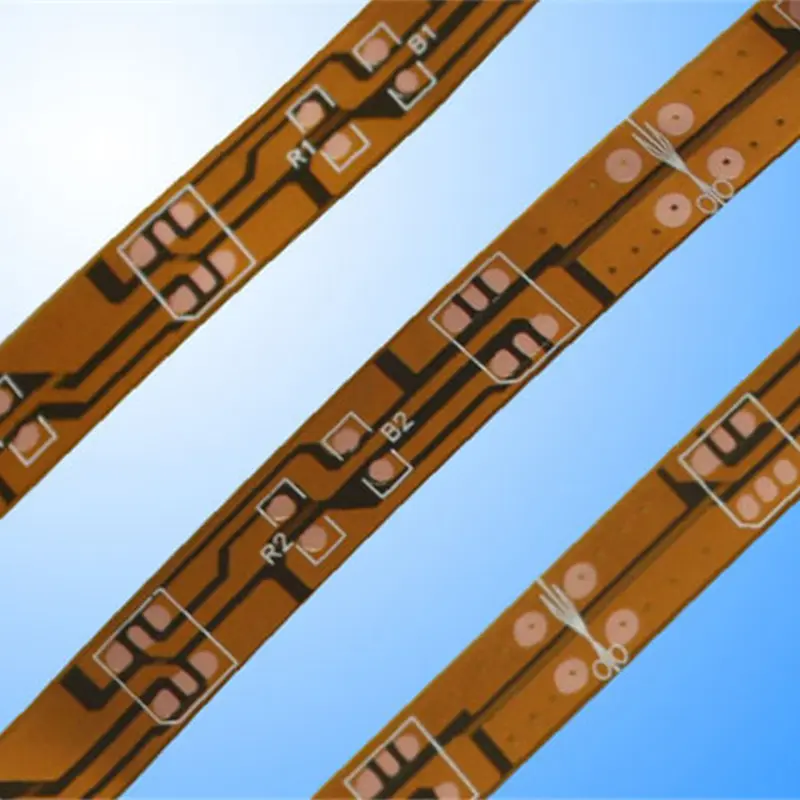
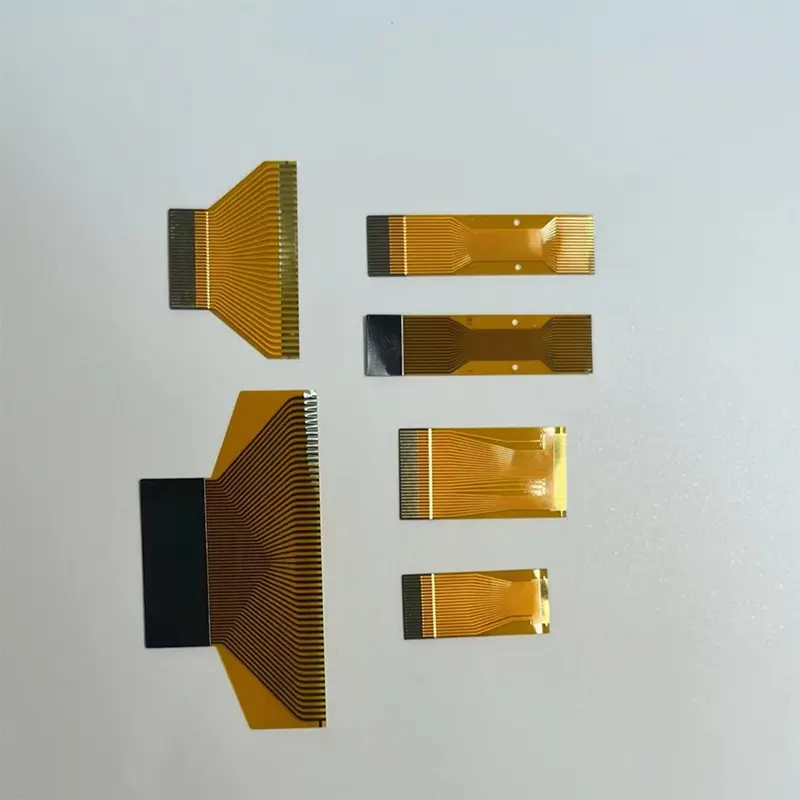
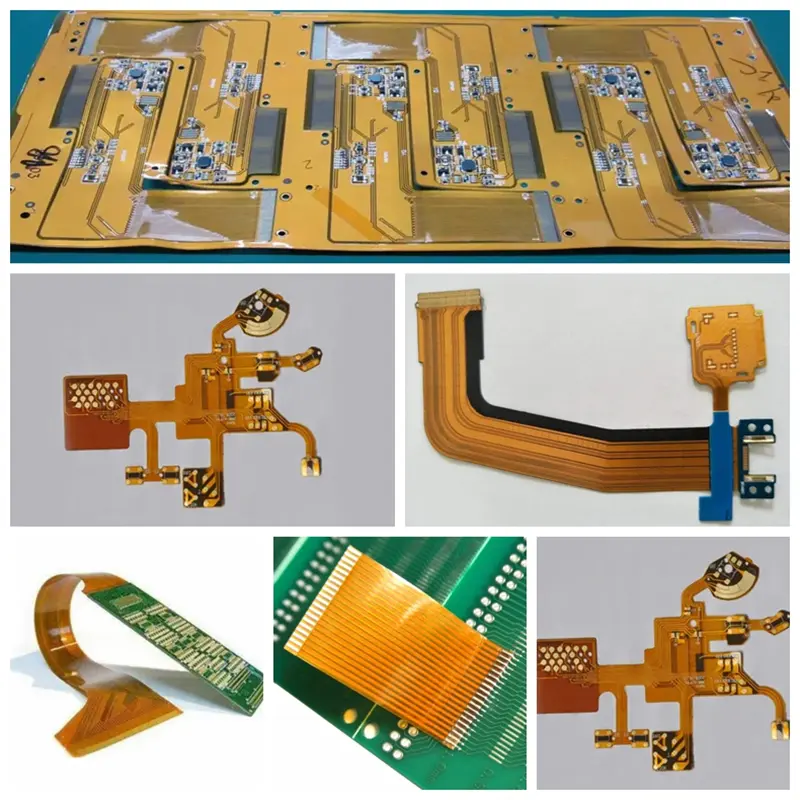
How to design Flexible PCB?
Flexible PCB (flexible printed circuit board) is widely used in consumer electronics, automotive electronics, medical equipment and other fields due to its characteristics of being bendable, thin and light, and resistant to bending. Its design needs to take into account the characteristics of flexible substrates, mechanical reliability and electrical performance. The core design points can be decomposed into the following core dimensions.
① . Base Material and Structure Selection
▶ Substrate selection
• Core base material: Commonly used PI (polyimide) base material (temperature resistance -200 ℃ to 260℃, excellent bending resistance), supplemented by PET (low cost, poor temperature resistance, only suitable for low-requirement scenarios); For the covering film, PI material is preferred as it needs to match the bending characteristics of the base material.
• Thickness matching: The thickness of the flexible substrate (such as 25μm, 50μm PI) should be combined with the bending radius and load-bearing requirements. If it is too thick, it is prone to cracking; if it is too thin, it is prone to deformation. Electrolytic copper (with good ductility) is preferred for copper foil. The recommended thickness is 12μm or 18μm. Thick copper (≥35μm) should be avoided as it may increase bending stress.
▶ Structural design
• Single/double/multi-layer flexible boards: Single layers are suitable for simple wiring, while multi-layers require an additional bonding layer (such as acrylic adhesive), but the bonding layer will reduce the bending life. For high-frequency/high-bending scenarios, glue-free flexible boards (Rigid-Flex) are preferred.
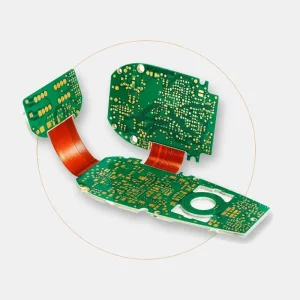
• Transition between rigid zone and flexible zone: The junction between the rigid zone (FR-4 substrate) and the flexible zone of the rigid-flex board should be chamfered (≥0.3mm) to prevent cracking caused by stress concentration.
②. Wiring and Layout Design
▶ Routing rules
• Line width and line spacing: The line width in the flexible zone is ≥0.1mm, and the line spacing is ≥0.1mm (fine lines can reach 0.05mm, but the yield decreases). For high-current traces, the width should be widened (for example, for 1A current, the line width should be ≥0.3mm and the copper thickness 18μm) to prevent heating.
• Routing form: Right-angle/acute Angle routing is prohibited (as it is prone to stress). All should use circular arc transitions (fillet radius ≥0.1mm). The wiring in the bending area should be as parallel as possible to the bending direction to avoid vertical wiring (vertical wiring is prone to breakage).
• Avoid single-point connection: The wiring in the bending area should not be fixed at a single point. Auxiliary wiring can be added or copper can be laid to enhance mechanical strength.
▶ Layout optimization
• Keep components away from the bending area: Components are not allowed to be mounted in the flexible area. Components should be placed in the rigid area and at least 1mm away from the edge of the flexible area to prevent the solder joints from being pulled during bending.
• Symmetrical layout: The wiring of multi-layer flexible boards should be symmetrically distributed to reduce the stress difference between layers during bending.
③. Bending and Reliability Design
▶ Bending radius control
• Minimum bending radius: It must meet the requirement of "bending radius ≥5 times the total thickness of the flexible board" (for example, if the total thickness is 0.1mm, the bending radius ≥0.5mm). For dynamic bending (repeated bending) scenes, the radius needs to be increased to 10 times the total thickness.
• Bending times: The dynamic bending life of a common flexible board is approximately 100,000 times. For high-reliability scenarios, bent-resistant base materials (such as modified PI) should be selected, and the number of layers in the bending zone should be reduced.
▶ Stress relief
• Copper laying design: Grid-shaped copper sheets (instead of solid copper) can be laid in the bending area to reduce the stretching/compression of the copper foil during bending. The edges of the copper sheet are chamfered to prevent warping.
• Reinforcing ribs: In areas prone to wear or high stress, polyimide reinforcing ribs (25 to 50μm in thickness) can be added, or the covering film can be thickened locally.
④. Pad and Hole Position Design
▶ Pad specification
• There are no pads in the flexible zone: Pads are only arranged in the rigid zone. If welding is required in the flexible zone (such as connectors), a rigid reinforcing plate (FR-4 or stainless steel) needs to be added. The size of the reinforcing plate should cover the outside of the pad by ≥0.5mm.
• Pad shape: Rectangular pads with rounded corners (radius ≥0.1mm) to prevent cracking at the pad edges. The size of the surface mount pad (SMD) should match the pins of the components, with a solder allowance of 0.05 to 0.1mm reserved.
▶ Hole position design
• Through holes: Through holes are prohibited in the flexible zone and must be arranged in the rigid zone. The hole diameter of the metallized vias should be no less than 0.2mm, and the copper plating thickness on the hole walls should be no less than 8μm to prevent the vias from breaking.
• Positioning holes: Positioning holes should be kept away from the bending area, with a hole diameter tolerance of ±0.05mm. The edges of the holes should be chamfered to prevent the flexible area from being scratched during assembly.
⑤. Manufacturing and Process Compatibility
▶ Covering film design
• The covering film (the insulating layer protecting the flexible substrate) must completely cover the flexible area traces. The distance between the edge of the window of the covering film (exposed pads/test points) and the traces should be ≥0.1mm to avoid exposed copper.
• Covering film lamination: It should be free of bubbles and wrinkles. The recommended thickness of the covering film in the bending area is 25μm. If it is too thick, the bending flexibility will be reduced.
▶ Process limitations
• Bending process: For flexible boards, cold bending (at room temperature) is required. Hot bending is strictly prohibited (high temperatures can damage the performance of the base material). The bending Angle should not exceed 180°, and a rebound allowance should be reserved.
• Surface treatment: For the flexible zone surface, OSP (organic solder mask) or nickel-gold plating is preferred. Tin spraying should be avoided (high-temperature tin spraying will reduce the flexibility of the substrate).
⑥. Electrical Performance Supplement
• Impedance control: For high-frequency flexible boards (such as 5G and RF scenarios), impedance calculation (such as 50Ω and 100Ω differential impedance) is required. This can be achieved by adjusting the line width, line spacing, and dielectric constant of the substrate. The impedance deviation in the bending area needs to be controlled within ±10%.
• Grounding design: The flexible board should be designed with a complete grounding layer (or grounding wiring) to reduce electromagnetic interference. The grounding layer should be as continuous as possible and avoid disconnection in the bending area.
The core of flexible PCB design lies in "adapting to bending characteristics, distributing stress, and ensuring dual reliability of electrical and mechanical aspects". It prioritizes following the basic principles of "wide traces, arc transitions, component placement far from the bending area, and matching the bending radius", while adjusting the substrate and structure selection in combination with application scenarios (static/dynamic bending, high frequency/large current).
Flexible PCB manufacturing processes and controls.
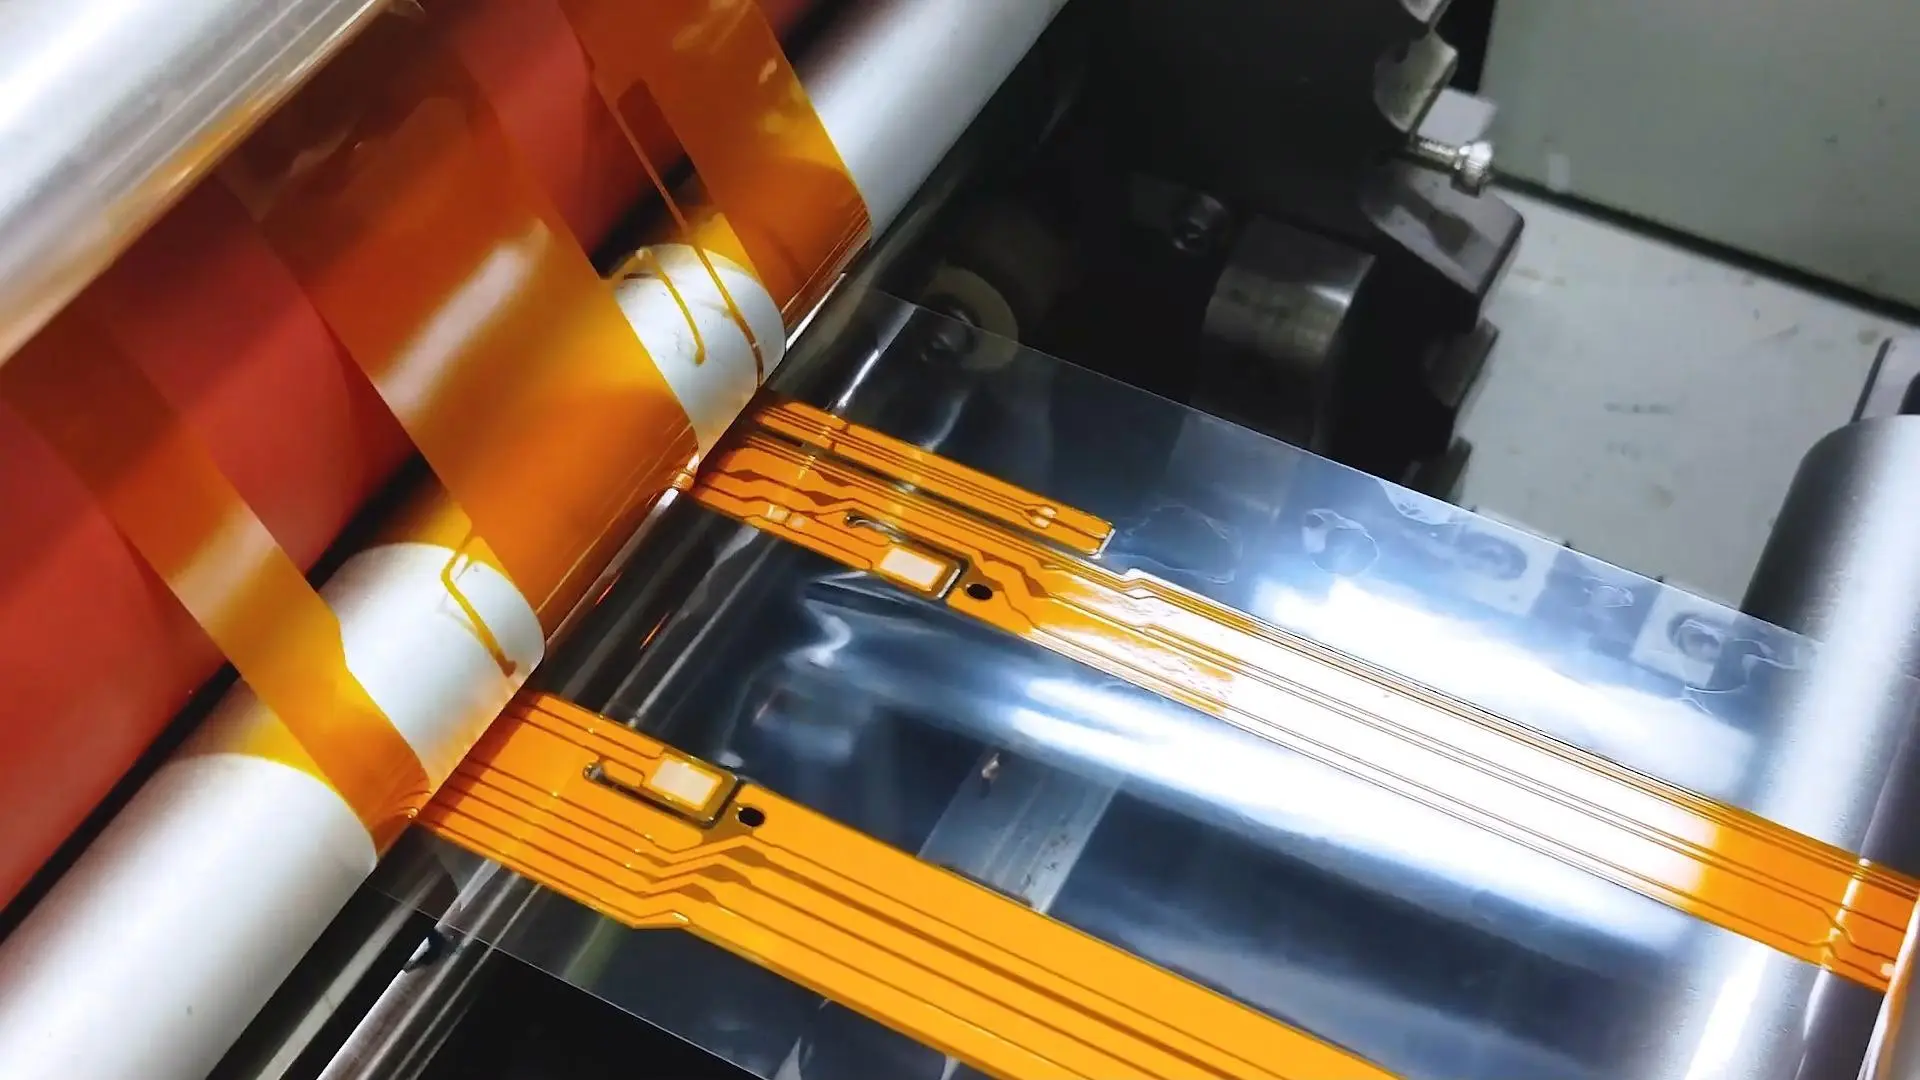
The manufacturing process of flexible PCBs is one of the most delicate and complex fields in electronic manufacturing. The core difficulty lies in dealing with extremely thin, soft, deformable and environmentally susceptible materials. The following figure clearly summarizes its core process flow and the key points of control at each link:
Below, we will provide a detailed interpretation of the process details and control points of each link:
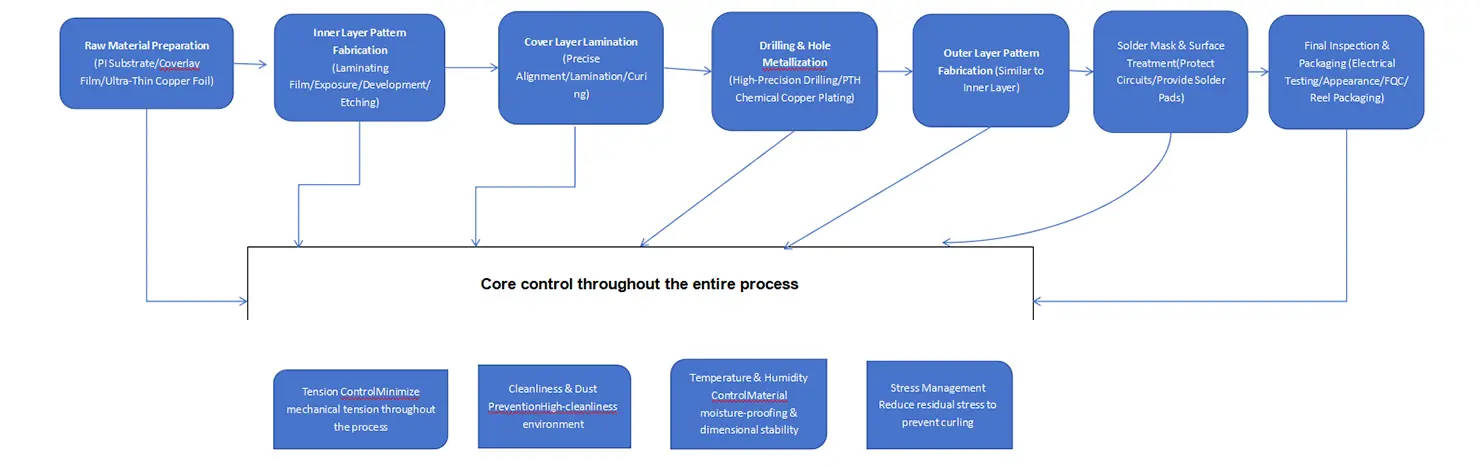
I. Detailed Explanation of Core Manufacturing Process Flow
▶ Phase One: Formation of the inner layer circuit
• Cutting and cleaning: Cut the roll-shaped PI substrate and copper foil. It should be carried out in a constant temperature and humidity environment. After cutting, clean immediately to remove oil stains and particles.
• Dry film application/photoresist coating: Apply a single layer of photosensitive resist (dry film) onto the copper foil.
• Exposure and development: By exposing the film with a line pattern to ultraviolet light and then developing it, the required line pattern is protected, and the unexposed resist is washed away.
• Etching: Use chemical solutions (such as acidic copper chloride) to etch away unprotected copper to form fine copper circuits. Here, the control requirements for the etching factor (degree of side etching) are extremely high to ensure the accuracy of the fine lines.
• Film removal and cleaning: Remove the resist layer protecting the circuit to obtain the exposed inner circuit pattern.
▶ Phase Two: Coating lamination
• Surface treatment: Micro-etching or chemical treatment is carried out on the copper circuit to enhance the adhesion with the covering layer.
• Coating alignment and lamination: This is the key difficulty. Align the PI covering film (with an opening to expose the solder pad) or liquid photosensitive covering ink with the inner circuit through a precise optical alignment system, and then perform hot-pressing curing. It is essential to ensure that there are no bubbles, no wrinkles and that the alignment is precise.
▶ Phase Three: Drilling and hole metallization
• Drilling: Due to the softness of the material, a drilling rig with high rotational speed and low feed rate should be used, along with specially designed covers and pads, to prevent burrs at the hole opening, nail heads or material tearing.
• Pre-treatment of hole walls and electroless copper plating: The hole walls of flexible materials are smooth and not prone to adhesion. First, the drilling dirt should be removed and activated with plasma or potassium permanganate solution, and then a thin layer of chemical copper should be deposited on the hole wall to provide a conductive substrate for the subsequent electroplating.
▶ Phase Four: Outer Circuit and Final Processing
• Outer layer pattern transfer: Similar to the inner layer, through steps such as film application, exposure, development, pattern electroplating, thickening of copper holes and circuits, and etching, the outer layer circuits and through hole connections are formed.
• Solder mask and surface treatment: Apply flexible solder mask ink to protect the circuit and expose the pads. The pads undergo surface treatment, such as chemical nickel-gold, OSP or electroplated hard gold (for gold fingers), to meet the welding or contact requirements.
• Shape processing: The final shape is cut out through precision die punching or CNC milling machines. The mold clearance and milling cutter parameters must be strictly controlled to prevent delamination and burrs.
• Electrical Testing and final Inspection: Conduct 100% open and short circuit electrical tests (commonly used flying probe tests). And carry out strict visual inspection, dimensional measurement and reliability spot checks (such as bending test, solderability test).
II. Four core control dimensions running through the entire process
▶ Tension control
• Objective: From opening to winding, all conveying rollers and mechanical hands must achieve minimum tension or even zero tension transmission.
• The reason is that any excessive stretching will lead to permanent deformation of the material, inaccurate alignment of the graphics, dimensional deviations, and even microcracks.
▶ Cleaning and dust-proof control
• Objective: Key processes (exposure, lamination, covering) must be carried out in an environment with a cleanliness level of 1,000 or higher.
• The reason is that tiny dust particles falling on the film or material can cause defects such as circuit notches, short circuits or open circuits.
▶ Temperature and humidity control
• Objective: Maintain a constant temperature and humidity throughout the workshop (e.g., 22±2°C, 50± 5%RH). All hygroscopic materials (PI, covering films) must be strictly baked before use.
• Reason: After the material absorbs moisture, it may experience plate cracking, delamination and bubbles during high-temperature processes. Changes in humidity can also cause slight variations in material dimensions, affecting alignment accuracy.
▶ Stress Management
• Objective: To balance the stress of each layer of material in design and process.
• Measures: Design symmetrical stacked structures; A slow cooling process is adopted after lamination. Stress release baking should be carried out when necessary. Prevent the finished board from warping and curling.
The application of flexible PCBs in 2026
Looking ahead to 2026, the application of flexible PCBs (FPCs) and rigid-flex boards will become more extensive and in-depth. The core driving forces for their growth come from the innovation of equipment forms, the demand for performance improvement, and the explosion of emerging markets. The following are predictions and trends for several key application areas:
1. Consumer electronics: The core of the form revolution
• Folding/curling/stretching screen devices: Flexible PCBs will continue to serve as the "neural network" for hinges and screens. By 2026, the forms of foldable phones will be more diverse (such as three-fold and rollable), and the requirements for the bending reliability, thinness and lightness, and signal integrity of FPCs will reach new heights.
• Augmented reality/virtual reality devices: Pursuing ultimate lightness and ergonomics, flexible PCBs are the key to achieving high-density wiring and sensor integration in thin and light helmets and smart glasses.
• New wearable devices and "electronic skin": Smart bracelets/watches will integrate more health sensors (such as continuous blood glucose monitoring), and flexible PCBs will serve as the carrier to fit the skin and achieve comfortable wearing. "Electronic tattoos" or flexible patches used for health monitoring will start to enter the consumer market.
2. Automotive Electronics: The "Blood vessels" of Intelligence and Electrification
• Intelligent cockpits and displays: Large-sized, irregular-shaped, and height-adjustable automotive displays (such as full-width curved screens) will extensively employ rigid-flex panels and FPCs to achieve complex wiring and high reliability.
• Advanced driver assistance systems and autonomous driving: An increasing number of cameras, millimeter-wave radars and lidar sensors around the vehicle body require lightweight FPCs that can adapt to complex vehicle body curves for high-speed signal transmission.
• Battery management system: Inside the battery pack of new energy vehicles, the replacement of traditional wiring harnesses by FPC has become a clear trend. By 2026, the application penetration rate of FPC in BMS will increase significantly as it can achieve more accurate voltage/temperature monitoring, higher integration and automated production.
3. Medical and health care: In-depth from diagnosis to treatment
• Implantable and ingestible devices: Micro-implantable devices used for cardiac monitoring, nerve stimulation, etc., whose ultimate miniaturization and biocompatibility requirements must rely on highly integrated flexible/rigid-flexible combined circuits.
• High-end wearable medical devices: Hospital-grade continuous vital sign monitoring patches will become more widespread, and flexible PCBs are the core to ensure comfort, accuracy and wireless connectivity.
4. Communication and Computing: The Cornerstone of Performance Upgrade
• 5G-Advanced/6G and millimeter-wave devices: High-frequency communication requires extremely low signal loss. Flexible circuits using new substrates such as liquid crystal polymers will become the preferred solution for millimeter-wave antenna modules and high-speed connectors in mobile phones and base stations.
• Advanced packaging and chip interconnection: In the semiconductor field, FPC technology will be more widely applied to chip-level interconnection, such as the interposer layer in 2.5D/3D packaging or the rewiring layer in fan-out packaging, to enhance computing power.
5. Robots and Human-Machine Interaction
• Bionic and collaborative robots: Flexible sensors and circuits will be integrated into the robot's "fingers" and "skin", endowing it with more sensitive touch and adaptive grasping capabilities.
• The integration of flexible electronics and structural components: FPC will be further integrated with structural components to form "structural electronics", meaning that the product casing itself is part of the circuit, achieving ultimate space savings and functional integration.
Summary: Core trends in 2026
• Technology integration: FPC is no longer merely a "connecting wire", but is integrating with functional devices such as sensors, antennas, heat dissipation films, and light-emitting components, becoming a "multi-functional system module".
• Material innovation: The pursuit of higher frequencies, greater heat resistance, and better bending performance will continue to drive the popularization of high-end substrates such as LCP and modified PI.
• Market penetration: With cost optimization and process maturation, FPC will rapidly penetrate from high-end models to mid-range consumer electronics and mainstream vehicle models.
Conclusion
Flexible PCB (FPC) is a silent revolution in electronic interconnection technology. It is not only a material that makes electronic devices "softer" and "thinner", but also a fundamental enabling technology that drives product innovation, enhances system performance, and gives rise to brand-new application scenarios. Its future development will continue to follow the direction of "thinner and lighter, more reliable, higher frequency and speed, and higher integration", deeply embedded in every key electronic node of the intelligent society, and its importance will increase day by day.
Send inquiry
Frequently Asked Questions (FAQ)
The main difference lies in the core material. Rigid PCBs use a hard glass fiber substrate, while Flexible PCBs (FPCs) use a flexible plastic film, typically polyimide (PI). This allows FPCs to bend, fold, and fit into irregular or tight three-dimensional spaces, reducing weight and device thickness.
For static bending, the minimum bending radius should be at least 5 times the total thickness of the flexible board. For dynamic bending (repeated bending applications), the radius must be increased to at least 10 times the total thickness to prevent mechanical failure and track cracking.
No, components should not be mounted within the active bending zone. They must be placed in rigid zones or supported by rigid reinforcing plates (FR-4 or stainless steel) at least 1mm away from the flexible boundary to prevent the solder joints from cracking during bending.
Because flexible substrates are thin and soft, any excessive tension during roll-to-roll processing can cause permanent stretching. This stretching leads to dimensional variations, misaligned circuit layers, and microcracks in the copper traces.
By 2026, FPCs will be highly integrated into foldable/rollable mobile screens, AR/VR headsets, smart health patches, advanced driver assistance systems (ADAS), and electric vehicle Battery Management Systems (BMS), replacing traditional heavy wiring harnesses.