Buy Heavy Copper PCB for Power Converters - High Current Capacity & Heat Dissipation from China Suppliers & Factory Manufacturers, Suppliers
Product Description
What is Heavy Copper PCB?
Core Features and Application Scenarios
Key Design Points
Common specifications: 70μm (2 oz), 105μm (3 oz), 140μm (4 oz), and up to 420μm (12 oz) in extreme scenarios.
Matching scenarios: For large current (≥5A) circuits, 2–4 oz copper is preferred. For ultra-power scenarios (≥20A), 6–12 oz copper should be selected.
Current-carrying capacity calculation:
Thick copper trace capacity must combine copper thickness, line width, and temperature rise requirements (usually designed based on a 10℃ temperature rise).
Formula reference: I = K × W × T0.83 (I = current, K = coefficient, W = line width, T = copper thickness).
Example: 2 oz copper (70μm), wire width 5mm → current carrying capacity ≈ 15A (temperature rise 10℃).
Trace optimization:
• Keep high-current traces as short and wide as possible; avoid narrow necks (sudden line width changes can cause local overheating).
• Multi-layer boards can use "parallel connection of multiple copper layers" (e.g., 2 layers of 2 oz copper ≈ 4 oz) to enhance current-carrying capacity.
Vias: For high-current vias, increase hole diameter (≥0.5mm), increase number of vias (estimated at 1A per hole), and ensure copper plating thickness on hole wall ≥20μm (vs. 8–12μm for ordinary PCBs).
Pads: Thick copper pads should be enlarged (0.2–0.5mm larger than ordinary pads) to prevent heat dissipation during soldering from causing false soldering.
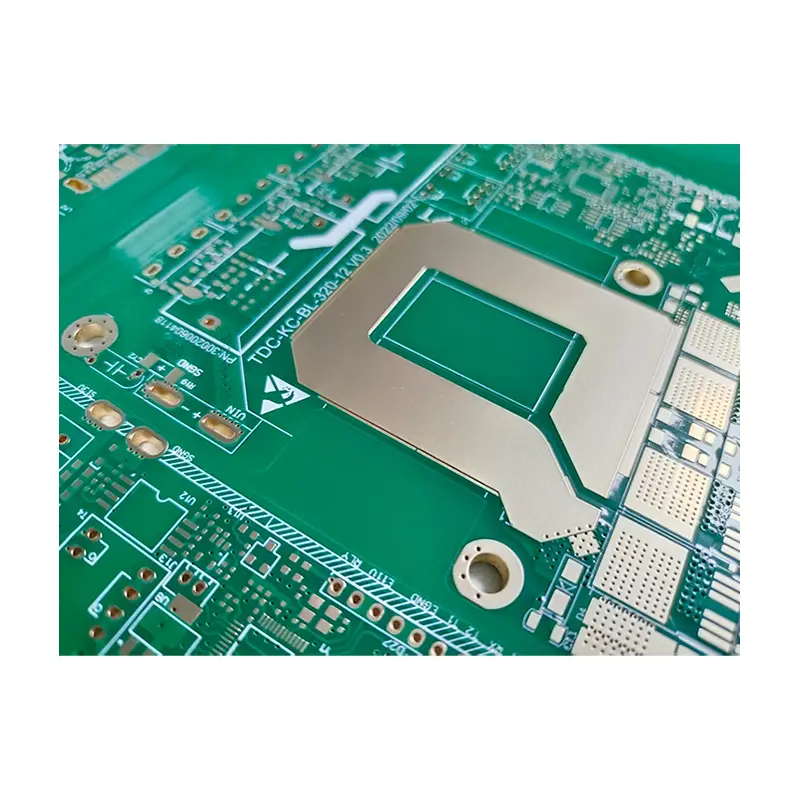
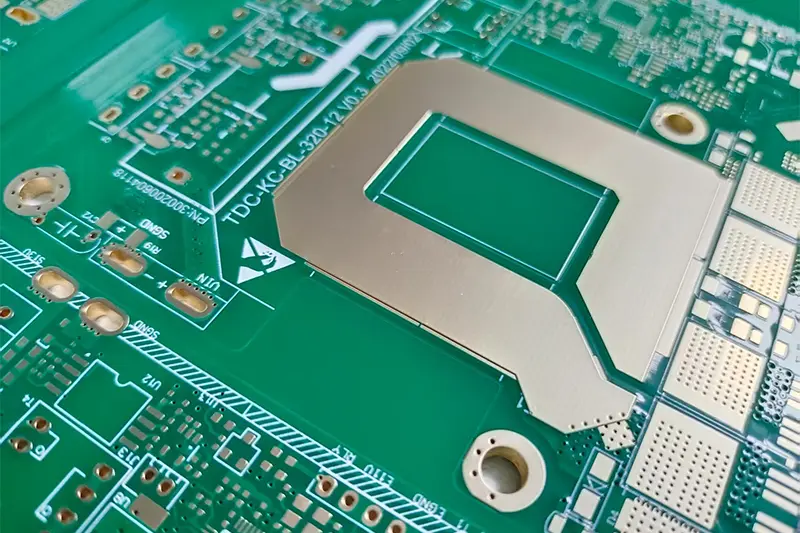
Heat dissipation: The thick copper area can be designed as a "copper sheet heat sink," or a metallized via array (via spacing ≤1mm) can be added to connect to the heat dissipation layer.
Insulation: Wire spacing for thick copper layers should be widened (for 70μm copper, wire spacing ≥0.2mm) to prevent creepage breakdown under high voltage.
Manufacturing Process Difficulties and Control
Thick copper lamination: High-temperature and high-pressure lamination (180℃ / 4MPa) is required to ensure peel strength between copper foil and substrate (≥1.2N/mm).
Thick copper etching: The etching rate is slow (~1μm/min); etching time must be controlled to avoid side etching (side etching ≤0.05mm). A stepwise etching process should be adopted to reduce line width deviation.
The coefficient of thermal expansion (CTE) of thick copper layers differs significantly from the substrate. During lamination, a "symmetrical structure" (consistent copper thickness between upper and lower layers) should be adopted, and a rigid support layer should be added to prevent PCB warping (warping degree ≤0.5%).
The surface of thick copper is prone to oxidation. It is preferred to choose tin plating (high-temperature tin layer) or nickel-gold plating to avoid OSP (incomplete organic film coverage).
The pad area needs to be enlarged with a "solder mask opening window" to ensure strong bonding force between the solder and thick copper.