
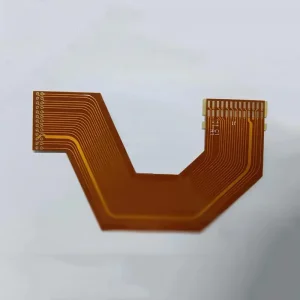
Polyimide Flex Solutions
Specially vetted for sub-millimeter tolerances, ruggedized vibration damping, and superior thermal dissipation across oceanic and agricultural operations.


Navigating unique geographic isolation, strict biosecurity standards, and the transition toward world-class intellectual property commercialization in Australasia.
New Zealand's commercial and industrial fabric presents one of the most distinctive technological ecosystems across the Asia-Pacific region. Often categorized globally under the "punching above its weight" paradigm, the Kiwi hardware sector is defined not by mass-market, razor-thin margin assembly, but by ultra-reliable, high-value specialty engineering. From the high-tech agriculture corridors of the Waikato and Canterbury plains to the thriving aerospace launch infrastructure at the Mahia Peninsula, New Zealand companies require electronics manufacturing partners capable of delivering industrial-grade resilience rather than generic commodity boards.
Historically, New Zealand hardware enterprises—spanning dynamic hubs in Auckland, Christchurch, Wellington, and Hamilton—confront severe logistical friction. Domestic printed circuit board fabrication capacity is constrained, geared predominantly toward rapid low-complexity breadboarding. Once a product graduates from pilot bench-testing to volume manufacturing, Kiwi engineers face extended lead times, escalated shipping tariffs, and inconsistent incoming quality from overseas spot brokers. Furthermore, electronic hardware operating in Aotearoa must withstand punishing environmental stressors: intense oceanic UV exposure, high coastal salt mist, fluctuating geothermal sulfur exposure in Rotorua and Taupō, and relentless temperature cycling across sub-alpine territories.
How international shifts in semiconductor geometries, advanced laminates, and automated manufacturing empower regional Kiwi tech champions.
As autonomous robotics, handheld diagnostic readers, and ultra-miniaturized cattle ear tags demand multi-core edge processors in sub-credit-card footprints, microvia technologies (laser-drilled blind and buried vias, stacked via-in-pad structures) have transformed from luxury military builds to standard commercial baseline requirements.
Transitioning to lead-free RoHS alloys (SAC305) with elevated reflow temperatures alongside demanding electric vehicle (EV) fast-charging infrastructure requires glass transition temperatures ($T_g$) reaching 170°C to 200°C. Heavy copper designs (3oz to 10oz) prevent delamination under extreme thermal shock.
With low-Earth-orbit (LEO) constellations such as Starlink and domestic aerospace innovations driving satellite-direct IoT communications, RF loss tangents ($\tan \delta$) must be rigidly preserved. Hybrid laminates coupling Rogers or Taconic PTFE cores with FR-4 backplanes offer low dielectric constant stability at optimized cost points.
Real-world execution paradigms demonstrating how specialized manufacturing addresses strict local operational criteria.
Operating Environment: Rotational pastures in Manawatu and Southland, characterized by deep animal washdowns, chemical slurry contact, and mechanical impacts from livestock.
Hardware Solution: Rigid-flex multi-layer boards coated with customized conformal silicones, equipped with IP68 potting encapsulation. Low-power Bluetooth (BLE) and LoRaWAN transceivers built with ultra-tight crystal impedance tuning to maximize 10-year field battery life.
Operating Environment: High-salinity oceanic expanses off the Chatham Rise and Cook Strait, enduring continuous vibration, brine ingress, and deep thermal cycling.
Hardware Solution: Immersion Gold (ENIG) and Electroless Nickel Electroless Palladium Immersion Gold (ENEPIG) finishes preventing galvanic tin whisker degradation. Aluminum substrates for high-efficiency solar harvesting drivers under intermittent southern cloud cover.
Operating Environment: Rapid decompression, acoustic launch shocks exceeding 20G, and low outgassing constraints during ascent trajectories from launch facilities.
Hardware Solution: Polyimide-based rigid-flex PCBs featuring IPC Class 3 via barrel thickness (≥25μm), hybrid Taconic/PTFE RF laminates, and complete serialized MES tracking for every single component date code.
Eliminating fragmented sourcing by consolidating bare PCB engineering, BOM lifecycle optimization, SMT execution, and automated box-build verification.
Managing an overseas electronics supply chain from Wellington or Auckland often induces substantial friction: communication lags across disparate time zones, opaque component sourcing channels vulnerable to grey-market counterfeit chips, and finger-pointing between the bare board fab shop and the assembly house when solder bridging or thermal voids emerge. Our macro turnkey solution provides New Zealand engineering teams with a single, legally accountable partner operating from Shenzhen—the world's foremost electronics epicenter—bridged by international-standard project management.
Before metal touches copper, our engineering team executes thorough Design for Manufacturability (DFM) and Design for Assembly (DFA) audits. We verify aspect ratios, drill-to-copper clearances, solder mask dam integrity, and perform active BOM scrubs to identify end-of-life (EOL) or high-risk allocation components, recommending drop-in pin-compatible alternatives.
Through direct authorization agreements with Tier-1 franchises (Texas Instruments, Analog Devices, STMicroelectronics, Microchip, Murata), every passive and active silicon wafer is tracked under strict Incoming Quality Control (IQC). X-ray fluorescence (XRF) and decapsulation microscopy safeguard against refurbished or counterfeit silicon.
Solder volume consistency dictates joint integrity. Our Yamaha high-speed SMT lines deploy automated 3D Solder Paste Inspection (SPI) to catch aperture clogging before component placement, followed by dual-stage pre- and post-reflow 3D Automated Optical Inspection (AOI) to eradicate coplanarity offsets, tombstoning, and solder balls.
Strategic evolutionary targets driving high-density routing, environmental sustainability, and ultra-high frequency hardware architectures.
Full industrialization of 01005 passives and 0.3mm pitch BGAs for wearable health monitors and compact drone gimbals. Solder paste stencil nanocoating as a standardized assembly protocol.
Embedding resistors and capacitors within inner core laminates, freeing top and bottom surface topology for high-pin-count FPGAs and integrated RF front-ends.
Aligning with New Zealand's aggressive "Clean Green" mandates by pioneering recyclable water-soluble transient PCB laminates for seasonal soil sensing and single-use agricultural diagnostics.
Co-packaged optics (CPO) and integrated polymer waveguides on flexible polyimide substrates for real-time edge AI inference and sub-millimeter aerospace lidar telemetry.
Actionable technical clarification regarding customs, shipping routes to NZ ports, IPC validation, and intellectual property safety.
Select from our certified high-layer count, heavy copper, high-Tg, and turnkey embedded solutions to accelerate your production cycles.

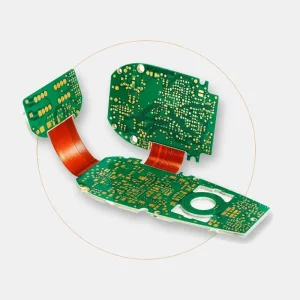




Connect directly with our senior hardware and DFM engineers in Shenzhen. Send your Gerber files, BOM lists, or custom enclosure specs to receive a comprehensive quote and DFM report within 24 hours.