
Famous China PCB Prototyping: Leading Suppliers and Factory Solutions for Rapid Product Development Supplier, Companies
View Specifications
Pre-engineered rigid, flex, RF, and thermal management interconnect platforms optimized for mission-critical deployments.
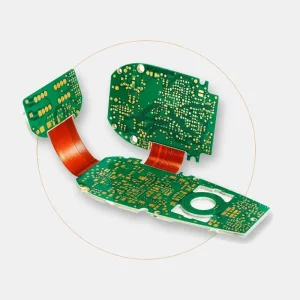



Eliminating wire harnesses, minimizing signal reflection, and mastering differential thermal expansion in high-reliability 3D packaging.
In modern electronic hardware architectures, the transition from discrete multi-board connector wiring assemblies to hybrid Rigid-Flex Printed Circuit Boards represents one of the most substantial advancements in structural reliability, signal preservation, and cubic-volume optimization. Rigid-flex circuitry integrates the mechanical stiffness of rigid FR-4/high-Tg polyimide laminates with the continuous dynamic flexing capabilities of adhesiveless polyimide (PI) films. By removing fragile board-to-board connectors, solder terminals, and flexible flat cables (FFCs), rigid-flex boards inherently eradicate the primary failure modes of high-vibration systems—contact fretting, pin oxidation, and intermittent crimp disconnects.
Achieving defect-free rigid-flex manufacturing requires deep metallurgical mastery and specialized tooling. The thermal expansion coefficient (CTE) mismatch between polyimide flex cores (CTE-Z ≈ 50–70 ppm/°C) and standard rigid prepregs (CTE-Z ≈ 35–45 ppm/°C) presents severe delamination risks during sequential lamination cycles and high-temperature reflow soldering (260°C lead-free profiles). Top-tier Chinese manufacturers overcome this physical limitation using low-flow or no-flow prepregs, adhesiveless copper-clad laminates (FCCL), laser-direct drilling for blind/buried microvias, and precise plasma etching to guarantee chemical-free hole wall smear removal prior to electroless copper deposition.
Pioneering sub-micron precision, modified Semi-Additive Processes (mSAP), and high-frequency polymer substrates.
Traditional subtractive etching creates trapezoidal trace cross-sections that degrade high-frequency signals. Leading China facilities employ modified Semi-Additive Processing (mSAP) to build vertical rectangular trace geometries down to 20/20 μm line/space.
As 5G millimeter-wave and 6G satellite communications surpass 40 GHz, conventional polyimide exhibits unviable dielectric losses (Df > 0.015). Advanced factories implement LCP and Modified Polyimide (MPI) substrates providing near-PTFE electrical performance.
Eliminating surface-mounted passives from outer layers by burying thin-film resistors, planar capacitive foils, and cavity-embedded die directly within internal rigid cores. This technology expands external surface real estate for high-density processors.
High-Density Interconnect (HDI) structures combined with flexible inner layers demand multi-press lamination control. Advanced vacuum laminators and CO2/UV picosecond laser drills enable stacked copper-filled microvias from layer 1 through layer 24.
Configured specifically to counter extreme thermal cycling, chemical ingress, mechanical strain, and EMI interference.
Medical electronics require biocompatible materials and zero-defect tolerance. Rigid-flex boards enable micro-cameras and sensor articulation in gastrointestinal endoscopes, hearing aids, and pacemaker battery monitoring systems.
Flight control computers, radar modules, and satellite solar array tracking systems face massive atmospheric pressure swings, thermal shock (-55°C to +125°C), and g-force vibration profiles.
Electric vehicle (EV) battery packs demand extended, distributed wiring topologies. Rigid-flex busbar assemblies integrate cell voltage monitoring, temperature sensing, and overcurrent fuses into a single robotic-assembly form factor.
Wearable augmented reality glasses and dual-screen foldable mobile devices require dynamic flex circuits capable of surviving hundreds of thousands of cycles without conductor cracking or impedance degradation.
Audited traceability, environmental stewardship, and aerospace-level quality gates for international procurement teams.
Procuring custom printed circuits from an overseas supplier creates valid supply chain security and compliance concerns. Top Shenzhen manufacturers counter these risks by maintaining rigorous, audit-ready global standards. Every rigid-flex production lot is governed by a fully documented Manufacturing Execution System (MES), providing barcoded component-level and panel-level traceability from raw laminate receipt to final functional burn-in.
| Standard / Regulation | Certified Scope & Target Applications | Audit Mechanism & Testing Frequency | Procurement Advantage |
|---|---|---|---|
| IPC-6013 Class 3 | Qualification and performance specification for flexible and rigid-flex printed circuit boards. | Micro-section cross-sectional analysis per panel coupon; barrel copper thickness ≥25 μm. | Guarantees zero-defect survivability in aerospace, military, and life-critical applications. |
| ISO 13485:2016 | Comprehensive quality management system for medical device components and PCBA assemblies. | Annual third-party registrar audits; cleanroom particulate monitoring; strict DHF/DMR records. | Seamless pass-through documentation for FDA 510(k) and EU MDR medical filings. |
| IATF 16949:2016 | Automotive quality management standard focused on defect prevention and supply chain variation reduction. | PPAP Level 3 documentation; 8D corrective action reports; MSA and SPC statistical process gates. | Verified tier-1 automotive qualification for electric vehicle power and sensor electronics. |
| UL 94V-0 & UL 796F | Safety standard for tests for flammability of plastic materials for parts in devices and appliances. | Quarterly unannounced UL laboratory sampling; vertical flame chamber burn time tests ≤10 seconds. | Global electrical safety acceptance without regional redesign or insurance re-certification. |
| RoHS & REACH Compliance | Restrictions on hazardous heavy metals (lead, cadmium, mercury, Cr-VI) and SVHC chemical substances. | X-ray fluorescence (XRF) screening on incoming raw stock and weekly certified lab ICP-OES tests. | Unrestricted import compliance across European Union, North American, and Asian markets. |
Shenzhen's 1-hour hardware cluster combined with automated smart fabrication and real-time MES traceability.
Shenzhen's Bao'an and Greater Bay Area industrial corridors integrate every required raw supplier—from DuPont Kapton films and Rogers ceramics to Panasonic Megtron laminates—within an hour's transit time. This geographical density compresses standard prototype turnaround to 3–7 business days.
Optical panel tracking, robotic AGV material handling, and smart recipe dispatching eliminate human handling errors. Real-time statistical process control (SPC) analyzes plating bath chemical concentrations and lamination press curves automatically every 15 minutes.
Overseas projects suffer when rigid-flex bare boards are shipped to secondary assembly houses that lack specialized flex-circuit SMT baking profiles and magnetic pallet tooling. Our unified 8,000 m² factory handles bare fabrication, high-speed SMT, conformal coating, and box build under one roof.
Rules-based Design for Manufacturability (DFM) benchmarks to maximize yields and eliminate post-assembly fatigue failures.
Rigid-flex circuit layouts cannot simply be treated as standard rigid boards with flexible segments attached. Dynamic mechanical forces, adhesive flow during hot pressing, and stress concentrations along the rigid-to-flex boundary demand adherence to strict DFM design rules:
In multi-layer flexible sections subjected to cyclic dynamic folding, copper conductors must reside as close as possible to the mechanical Neutral Bending Axis. Placing copper off-center introduces tensile stress during outward bending and compressive wrinkling during inward bending, leading to premature copper grain boundary shearing.
The boundary where the rigid coverplate terminates and the flexible polyimide emerges represents the highest stress riser on the assembly. Designers must specify a minimum clearance of 1.5 mm (60 mils) between the rigid edge and adjacent plated through-holes (PTH), and extend flex coverlays at least 0.8 mm inside the rigid zone.
Sharp 90° and 45° trace corners act as mechanical stress focus points within flexible zones. All flexible traces must utilize gentle radius curves (minimum 3x trace width) with reinforced teardrops at all pad and via junctions to prevent trace lifting during thermal reflow and repeated flex cycles.
On two-layer flexible arms, copper conductors on layer 1 should never be routed directly over conductors on layer 2 ("I-beam effect"), as this drastically increases overall flexural rigidity. Offsetting and staggering top and bottom traces retains maximum mechanical suppleness and extends dynamic flex life by over 300%.
Explore our specialized HDI, heavy copper, high-frequency microwave, and quick-turn high-layer manufacturing capabilities.



In-depth responses from our senior process engineering and quality assurance departments.